High temperature fine powder conveying systems are critical components in industrial processes that handle materials with high temperature characteristics and fine particle sizes. These systems are designed to efficiently transport powders such as cement, coal ash, and other fine particulate materials in environments where temperature control and material integrity are paramount. Understanding the working principle and key features of such systems is essential for optimizing operational efficiency and ensuring safe material handling in various industrial applications.
Working Principle of High Temperature Fine Powder Conveying Systems
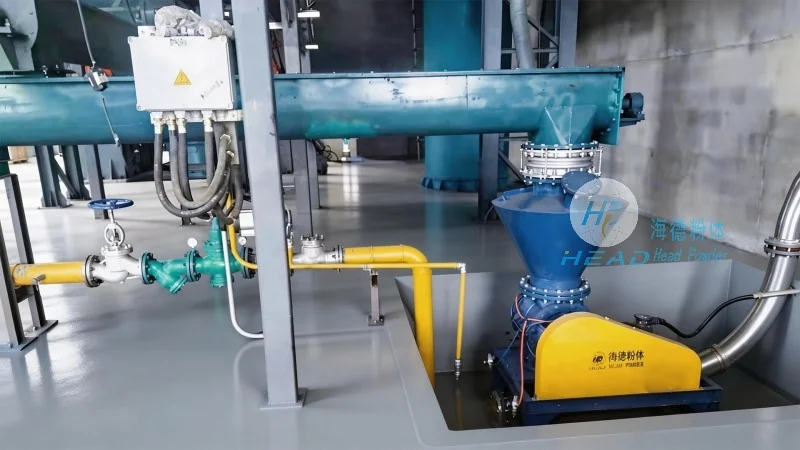
The core working principle of high temperature fine powder conveying systems revolves around the use of specialized equipment that can handle the thermal and physical properties of fine powders under elevated temperatures. Typically, these systems employ mechanisms like pneumatic conveying, screw conveyors, or combination systems that integrate both mechanical and pneumatic components. The process generally involves the following steps: material feeding, heating or temperature regulation, and controlled transportation to the destination point. In pneumatic conveying, for instance, the system uses compressed air to create a flow that transports the fine powder through a pipeline. The temperature of the material is maintained within safe limits through insulation and temperature control measures, ensuring that the powder does not degrade or lose its properties during transit. The system also includes components like cyclones, filters, and dust collectors to manage the powder and air mixture, ensuring efficient separation and collection of the material. The mechanical parts, such as screw conveyors, are designed with heat-resistant materials and proper sealing to prevent heat loss and material leakage. Overall, the working principle is centered on maintaining the material's temperature and particle integrity while achieving reliable and continuous transportation.
Key Features of High Temperature Fine Powder Conveying Systems
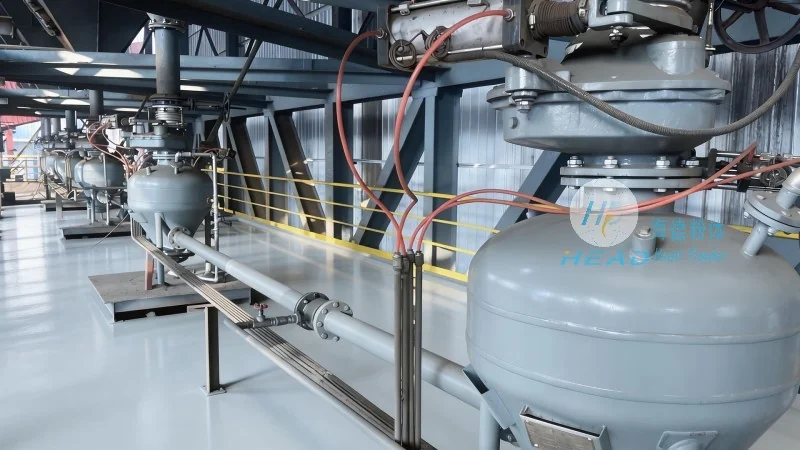
High temperature fine powder conveying systems are characterized by several key features that make them suitable for demanding industrial applications. First, they are equipped with advanced temperature control mechanisms that ensure the material remains within the optimal temperature range throughout the conveying process. This is crucial for materials that are sensitive to temperature changes, as degradation or quality loss can occur if the temperature is not properly managed. The systems also incorporate robust insulation and heat-resistant components, such as stainless steel or special alloys, to withstand the high temperatures and prevent heat transfer to the surroundings. Another important feature is the ability to handle fine particles without clogging or blockages. This is achieved through the design of the conveying components, including the use of high-efficiency cyclones and filters that can separate the fine powder from the air stream effectively. The systems are also designed for durability and long-term operation, with components that can withstand continuous exposure to high temperatures and abrasive materials. Additionally, they often include monitoring and control systems that allow operators to track the temperature, flow rate, and other parameters in real-time, ensuring optimal performance and preventing potential issues. The integration of safety features, such as pressure relief valves and emergency shut-off mechanisms, further enhances the reliability and safety of these systems. Overall, the key features of high temperature fine powder conveying systems focus on efficiency, durability, and safety, making them indispensable in industries that require the transportation of fine powders at elevated temperatures.
Application and Benefits in Industrial Settings
High temperature fine powder conveying systems find extensive applications in various industrial sectors, including cement production, power generation, and chemical processing. In cement plants, for example, these systems are used to transport raw materials and finished products, such as cement clinker, which are often at high temperatures. The ability to handle fine particles and maintain temperature control is essential for ensuring the quality of the final product. In power plants, the systems are used to convey fly ash and other fine particulate materials from boilers to storage or disposal sites. The efficiency and reliability of these systems help in maintaining the operational efficiency of the plant and reducing downtime. The benefits of using high temperature fine powder conveying systems include improved material handling efficiency, reduced energy consumption, and enhanced safety. By minimizing the need for manual handling and direct contact with hot materials, these systems reduce the risk of accidents and improve workplace safety. Additionally, the use of automated control systems allows for precise monitoring and adjustment of the conveying process, leading to better process control and product quality. The durability of the equipment ensures long-term operation with minimal maintenance, resulting in cost savings over the system's lifespan. Overall, the application of high temperature fine powder conveying systems contributes to the overall productivity and sustainability of industrial operations.
Conclusion and Company Overview
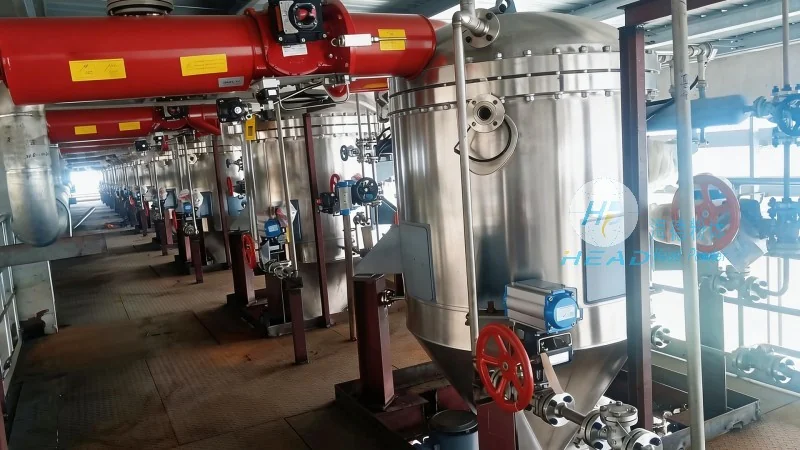
High temperature fine powder conveying systems are sophisticated industrial solutions that combine advanced technology and robust design to meet the demanding requirements of modern industrial processes. The working principle, which involves temperature control, efficient material transport, and effective separation, ensures that fine powders are handled safely and efficiently. The key features, including advanced temperature regulation, durability, and safety mechanisms, make these systems reliable and suitable for various applications. The benefits of using such systems, such as improved efficiency, reduced energy consumption, and enhanced safety, highlight their importance in industrial settings. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality high temperature fine powder conveying systems. With a focus on innovation and customer satisfaction, the company ensures that its products meet the specific needs of different industries, providing reliable and efficient solutions for material handling challenges. The company's commitment to quality and technical expertise has made it a trusted partner for businesses seeking to optimize their industrial processes and enhance operational performance. By leveraging advanced engineering and manufacturing capabilities, Shandong HeadPowder Engineering Co., Ltd. continues to deliver cutting-edge solutions that meet the evolving demands of the industry.




