For industrial applications requiring precise and efficient material handling, metering bin pumps represent a critical solution. This article explores the fundamental concepts of metering bin pump systems, their operational mechanisms, and the key design principles that ensure optimal performance in various material handling scenarios.
Understanding Metering Bin Pump Systems
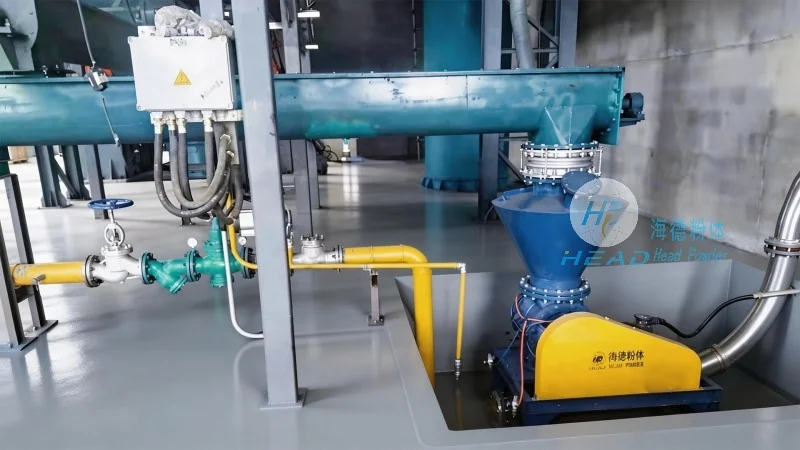
Metering bin pumps are specialized equipment designed to transport bulk materials from storage bins or silos to processing units with high accuracy and control. These systems are widely used in industries such as chemical processing, food production, and pharmaceutical manufacturing, where consistent material flow is essential for maintaining product quality and operational efficiency.
Key Components of Metering Bin Pump Systems
The core components of a metering bin pump system typically include a hopper or bin for material storage, a feeding mechanism (often a screw or rotary valve), a pump chamber, and a discharge outlet. The hopper is designed to hold the bulk material, while the feeding mechanism regulates the flow rate into the pump chamber. The pump chamber, equipped with a diaphragm or piston, creates a pressure differential to move the material forward. Finally, the discharge outlet delivers the material to the next stage of processing.
Design Principles for Optimal Performance
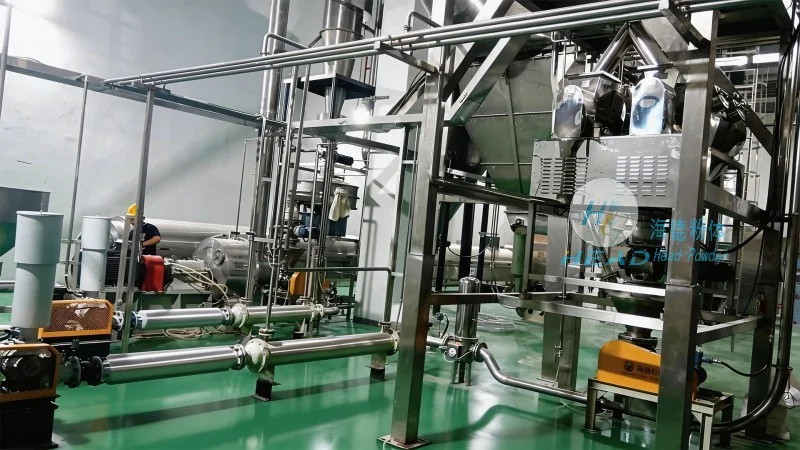
The design of metering bin pumps is guided by several critical principles to ensure reliable operation and precise material measurement. One of the primary principles is the maintenance of a consistent pressure differential within the pump chamber. This is achieved through the use of a flexible diaphragm or piston that expands and contracts, creating a suction and discharge cycle. The frequency and duration of these cycles determine the flow rate, allowing for precise control over the material output.
Another essential design principle is the prevention of material blockages and clogging. This is addressed through features such as anti-wearing liners in the pump chamber, which reduce friction and wear from abrasive materials. Additionally, the feeding mechanism is often equipped with a variable speed drive, enabling operators to adjust the feed rate according to the material's characteristics and processing requirements.
Applications and Benefits of Metering Bin Pumps
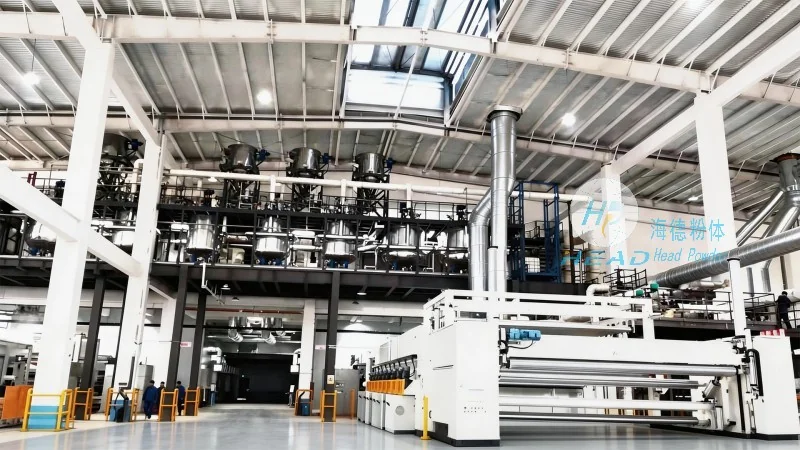
Metering bin pumps offer numerous advantages in industrial material handling, including high accuracy in material measurement, reduced material waste, and improved process control. These systems are particularly beneficial in applications where precise dosing is critical, such as in chemical mixing, pharmaceutical formulation, and food processing. By maintaining a consistent flow rate, metering bin pumps help ensure that downstream processes receive the exact amount of material needed, minimizing variations and improving overall product quality.
Conclusion
In summary, metering bin pump systems are sophisticated equipment designed to handle bulk materials with precision and efficiency. Their design, incorporating principles such as controlled pressure differentials, anti-clogging features, and adjustable feed rates, enables reliable operation across a wide range of industrial applications. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of these systems, leveraging decades of expertise to deliver solutions tailored to the unique needs of each client.




