For industries dealing with bulk powders, the efficient and safe handling of raw materials is a critical operational requirement. The intelligent bulk bag unloading powder conveying system equipment has emerged as a sophisticated solution to streamline these processes. This article delves into the functionality of such systems and explores the underlying design principles that make them effective in various industrial applications.
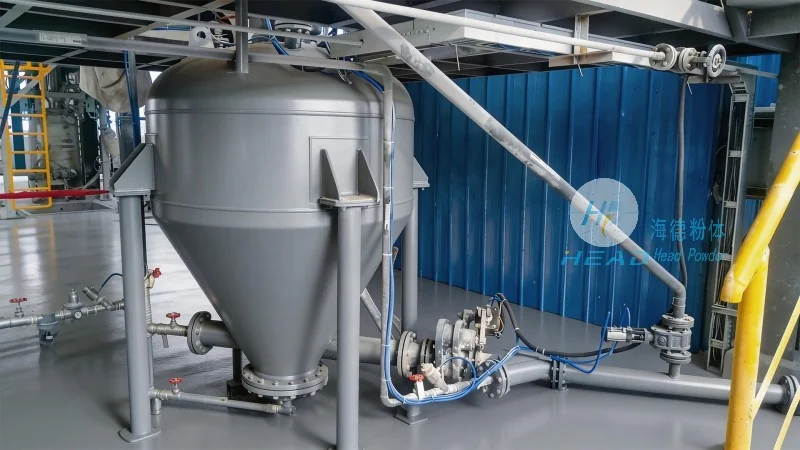
Introducing the Intelligent Bulk Bag Unloading Powder Conveying System
The intelligent bulk bag unloading powder conveying system is a specialized piece of equipment designed to automate the entire workflow from the unloading of bulk bags to the precise delivery of powders to processing units. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, this system integrates advanced technologies to enhance productivity, reduce labor costs, and minimize material loss during handling.
Key Components and Functionalities
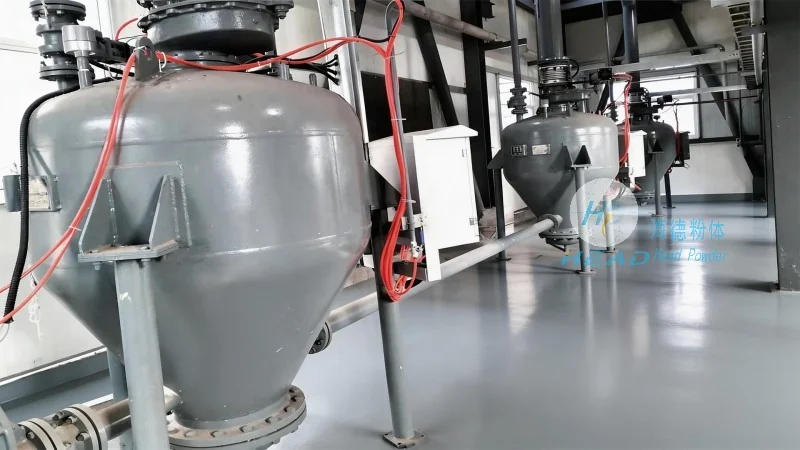
At the core of the system are several key components that work in tandem to ensure seamless operation. The primary unit is the bulk bag unloader, which features an automated mechanism to open and empty the bag without manual intervention. This is often coupled with a hopper or a feeding device that regulates the flow of powder into the conveying system. The conveying section typically employs screw conveyors, pneumatic systems, or a combination of both, depending on the specific material characteristics and process requirements. Additionally, the system includes a control panel equipped with sensors and monitoring tools to track the flow rate, detect blockages, and adjust operational parameters in real-time.
Design Principles Behind the System
The design principles of the intelligent bulk bag unloading powder conveying system are centered on efficiency, safety, and adaptability. One fundamental principle is the integration of automation to eliminate human error and reduce the risk of exposure to dust or hazardous materials. The system is engineered to handle a wide range of powder types, from fine powders to bulkier granules, by adjusting the speed of the conveyor and the pressure of the pneumatic components. Another key principle is the emphasis on material containment and dust control. The design incorporates sealed hoppers and enclosed conveying lines to prevent dust dispersion and ensure compliance with environmental regulations. Furthermore, the system is built for scalability, allowing it to be customized to fit different production capacities and facility layouts.
Technical Advantages and Benefits
Implementing an intelligent bulk bag unloading powder conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves operational efficiency by reducing the time required for material handling and minimizing downtime caused by manual interventions. The automated control system ensures consistent flow rates, which is crucial for maintaining product quality in downstream processes. Secondly, the system enhances safety by eliminating the need for workers to handle heavy bulk bags or work in dusty environments. This not only reduces the risk of occupational injuries but also improves overall workplace safety standards. Thirdly, the system contributes to cost savings through reduced labor costs and minimized material loss. By preventing spillage and optimizing the use of raw materials, the system helps in lowering operational expenses and improving the overall profitability of the facility.
Application Scenarios
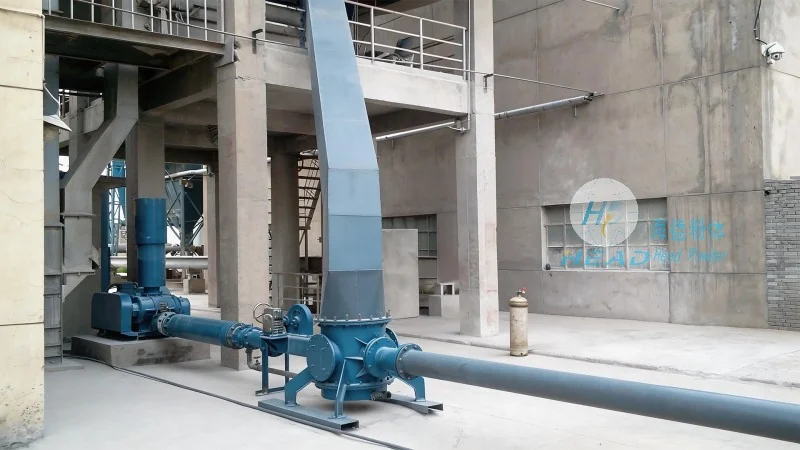
The intelligent bulk bag unloading powder conveying system is widely used across various industries that rely on bulk powder handling. In the chemical industry, it is employed to transport raw chemicals and intermediates, ensuring precise dosing and minimizing contamination risks. The food and pharmaceutical sectors also benefit from this technology, as it allows for the safe and hygienic handling of sensitive powders while maintaining compliance with regulatory standards. Additionally, in the mining and mineral processing industries, the system is used to transport ore powders and other bulk materials, supporting efficient extraction and processing operations.
Conclusion
As industries continue to seek more efficient and sustainable solutions for bulk powder handling, the intelligent bulk bag unloading powder conveying system stands out as a robust and versatile option. Developed by Shandong HeadPowder Engineering Co., Ltd., this equipment exemplifies the integration of advanced design principles and automation technology to meet the evolving demands of modern industrial operations. By understanding its components, functionalities, and design philosophy, businesses can make informed decisions about adopting such systems to enhance their operational performance and competitive edge.




