At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced pneumatic conveying systems tailored for handling shredded paper dust. This equipment is essential for efficiently transporting fine particulate materials like shredded paper, ensuring a clean and effective process in various industrial applications. The core of these systems lies in the principle of using air flow to move materials, which is a fundamental approach in powder and dust handling technology.
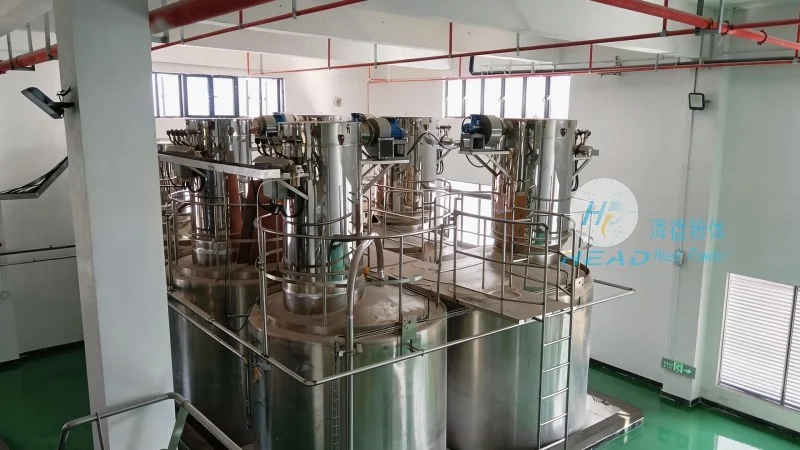
Working Principle of Pneumatic Conveying Systems
The pneumatic conveying equipment for shredded paper dust operates on the principle of air movement to transport material particles. There are two primary types of systems: the suction (or negative pressure) system and the pressure (or positive pressure) system. In the suction system, a vacuum is created at the material inlet to draw the shredded paper dust into the conveying line. This method is ideal for applications where the material is to be transported from multiple sources or over relatively short distances. The pressure system, on the other hand, uses compressed air to push the material through the pipeline, making it suitable for longer distances and higher material loads.
Key Components and Their Functions
Several critical components work together to ensure the smooth operation of the pneumatic conveying equipment. The material hopper or inlet is where the shredded paper dust is loaded, and it often includes a feeder to control the flow rate. The air supply system, which may consist of a vacuum pump or a compressed air source, provides the necessary air pressure or vacuum. The conveying line, typically made of stainless steel or other corrosion-resistant materials, transports the material from the inlet to the discharge point. The discharge unit, such as a rotary valve or a dust collector, manages the release of the material at the end of the line. Additionally, filters and dust collectors are integrated to maintain air quality and prevent dust contamination in the environment.
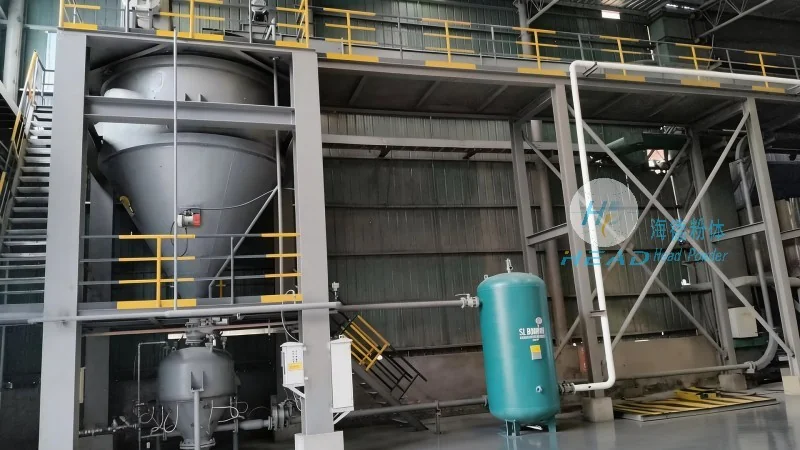
Advantages of Using Pneumatic Conveying for Shredded Paper Dust
Implementing pneumatic conveying equipment for shredded paper dust offers numerous benefits. First, it provides a dust-free and hygienic handling process, which is crucial in industries where contamination control is paramount. The enclosed system prevents the release of fine particles into the air, reducing health risks and maintaining compliance with environmental regulations. Second, these systems offer high efficiency and reliability, with minimal maintenance requirements compared to traditional mechanical conveying methods. The ability to handle fine and abrasive materials like shredded paper dust without causing wear and tear on equipment components is a significant advantage. Third, the flexibility of pneumatic conveying allows for the integration of multiple material sources and destinations, making it adaptable to various production layouts. This adaptability enhances operational efficiency and reduces downtime in industrial settings.
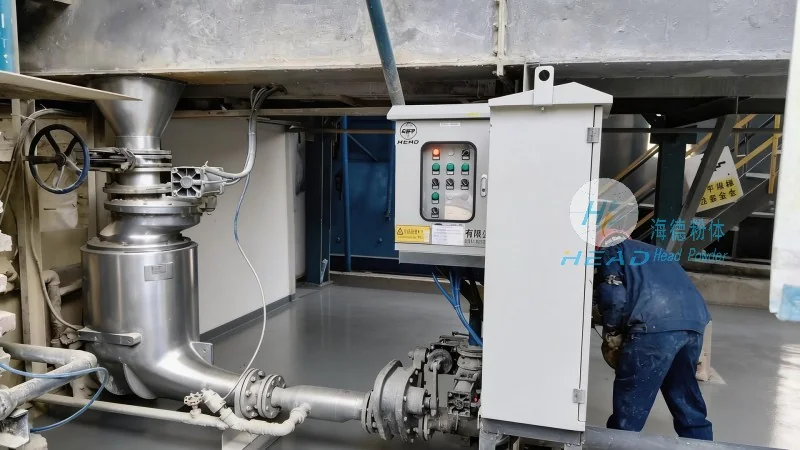
Application Scenarios and Industrial Use Cases
Pneumatic conveying equipment for shredded paper dust is widely used in several industrial sectors. In the paper and recycling industry, it is employed to transport shredded paper from sorting lines to processing facilities or storage areas. The equipment ensures that the material is moved without the risk of cross-contamination or loss of quality. In waste management facilities, it helps in the efficient transfer of shredded paper from collection points to recycling plants. The system's ability to handle large volumes of material quickly and safely makes it indispensable in these applications. Additionally, in research and development labs that work with fine paper particles, the equipment provides a controlled environment for material handling, supporting experiments and product development processes.
Customization and Engineering Solutions by HeadPowder
Shandong HeadPowder Engineering Co., Ltd. offers customized pneumatic conveying solutions tailored to the specific needs of each client. Our engineering team works closely with customers to understand their material characteristics, operational requirements, and space constraints. Based on this information, we design systems that optimize performance, energy efficiency, and cost-effectiveness. For instance, we can adjust the air flow rate, pipeline diameter, and component materials to suit the unique properties of shredded paper dust, such as its moisture content, particle size, and abrasive nature. Our commitment to quality and innovation ensures that each system we deliver meets the highest standards of reliability and durability. By leveraging our expertise in pneumatic conveying technology, we help our clients achieve efficient, safe, and sustainable material handling processes.




