HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced synthetic fiber pneumatic conveying systems. These systems are crucial for efficient material handling in various industrial sectors, offering a reliable and flexible solution for transporting powders and granules.
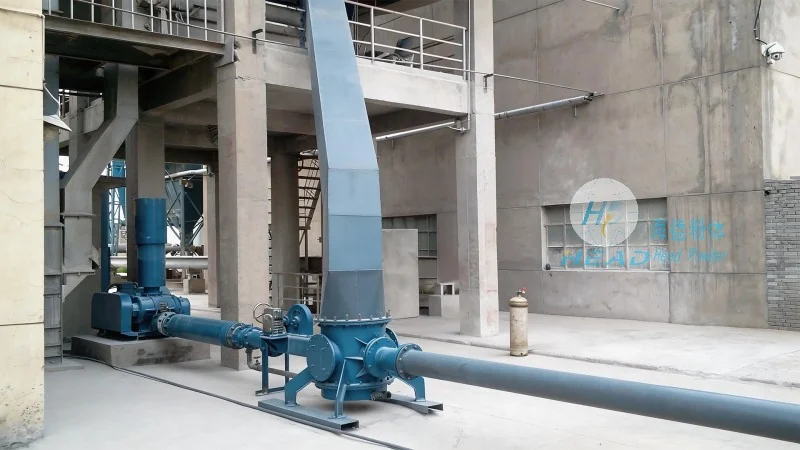
Overview of Synthetic Fiber Pneumatic Conveying Systems
Synthetic fiber pneumatic conveying systems utilize flexible hoses or pipes made from synthetic materials to transport bulk materials through a pressurized or vacuum environment. This method is widely adopted in industries such as chemical, food, pharmaceutical, and agriculture due to its ability to handle a diverse range of materials with minimal product degradation. The systems are designed to ensure consistent flow rates, maintain material integrity, and reduce operational costs compared to traditional mechanical conveying methods.
Classification of Synthetic Fiber Pneumatic Conveying Systems
Based on the operating principle and pressure differentials, synthetic fiber pneumatic conveying systems can be broadly classified into two main types: positive pressure systems and negative pressure systems.
Positive Pressure Systems
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air. The material is drawn into the system and transported through the hose. This type of system is ideal for applications requiring high material flow rates and long-distance transport. The positive pressure ensures that the material is continuously pushed forward, minimizing the risk of blockages and ensuring consistent performance.
Negative Pressure Systems
Negative pressure systems, also known as suction systems, operate by creating a vacuum in the conveying line, drawing material from the source and transporting it to the destination. These systems are commonly used for handling materials that are sensitive to pressure changes or for applications where the material source is at a higher elevation. The negative pressure helps in maintaining the material's quality and preventing contamination from external air.
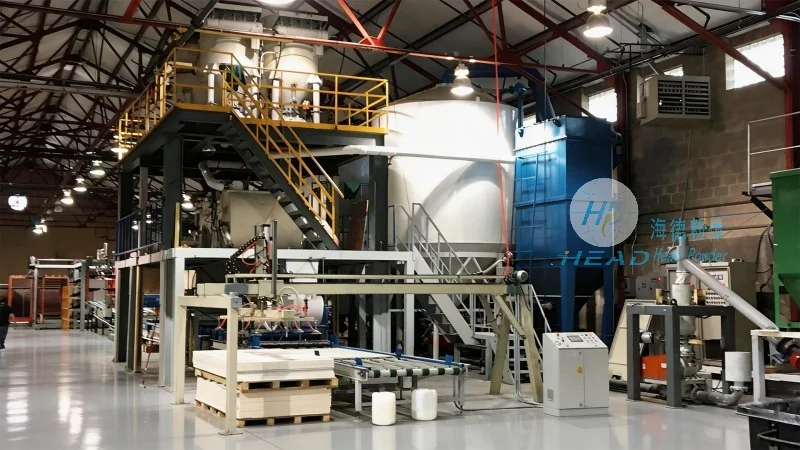
Key Applications in Industrial Sectors
HeadPowder's synthetic fiber pneumatic conveying systems are applied across multiple industries, each tailored to meet specific operational requirements.
Chemical Industry
In the chemical industry, these systems are used for transporting various powders and granules, including raw materials, intermediates, and finished products. The systems are designed to handle materials with varying particle sizes and moisture content, ensuring safe and efficient transfer. The synthetic fiber hoses are resistant to chemical corrosion, making them suitable for corrosive environments.
Food and Pharmaceutical Industry
For the food and pharmaceutical sectors, the systems are used to convey ingredients, additives, and finished products with strict hygiene standards. The materials are transported in a sterile environment, minimizing the risk of contamination. The flexible hoses are made from food-grade materials, ensuring compliance with regulatory requirements such as FDA and GMP standards.
Agricultural Industry
In agriculture, synthetic fiber pneumatic conveying systems are employed for handling agricultural products like seeds, grains, and powders. These systems are robust and durable, capable of withstanding harsh environmental conditions. The systems are designed to handle large volumes of material, improving the efficiency of harvesting and processing operations.
Advantages of Synthetic Fiber Pneumatic Conveying Systems
Compared to traditional mechanical conveying methods, synthetic fiber pneumatic conveying systems offer several advantages that make them a preferred choice in many industries.
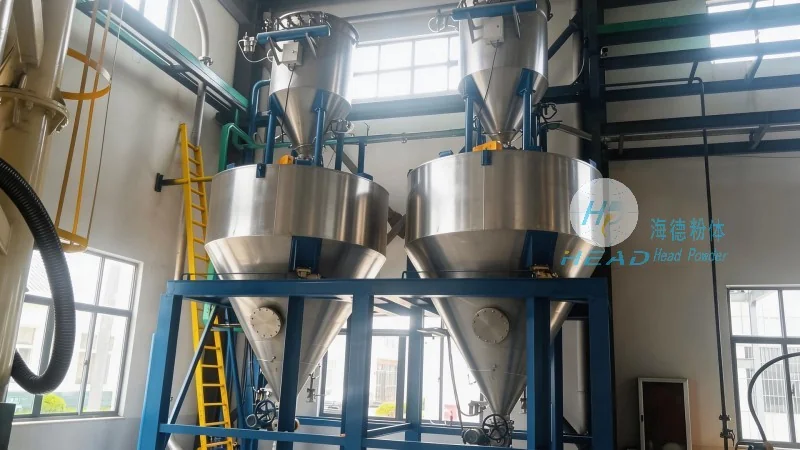
Flexibility and Versatility
The use of flexible synthetic fiber hoses allows for easy installation and configuration, enabling the system to adapt to different layouts and operational needs. The hoses can be bent and routed around obstacles, providing greater flexibility in plant design.
Low Maintenance and Longevity
Synthetic fiber hoses are durable and resistant to wear and tear, reducing the need for frequent replacements. The systems require minimal maintenance, resulting in lower operational costs over their lifespan. The materials used in the hoses are also resistant to UV radiation and chemical exposure, extending their service life.
Energy Efficiency
Modern synthetic fiber pneumatic conveying systems are designed to be energy-efficient, utilizing optimized air flow and pressure control to minimize energy consumption. This not only reduces operational costs but also contributes to environmental sustainability by lowering carbon emissions.
Conclusion
HeadPowder's synthetic fiber pneumatic conveying systems represent a reliable and efficient solution for material handling in various industrial applications. By understanding the classification and application of these systems, industries can make informed decisions to enhance their operational efficiency and product quality. The company's commitment to quality and innovation ensures that clients receive systems tailored to their specific needs, supporting their long-term success in the market.




