The intelligent tonne bag loading station material pneumatic conveying machine, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized equipment designed for efficient and automated material handling in industrial settings. This system integrates advanced technology to streamline the process of transferring bulk materials from tonne bags into processing equipment, ensuring high accuracy, minimal waste, and enhanced operational safety. The following sections will detail the operational process and working principles of this equipment, highlighting its key components and functional mechanisms.
Key Components of the Pneumatic Conveying System
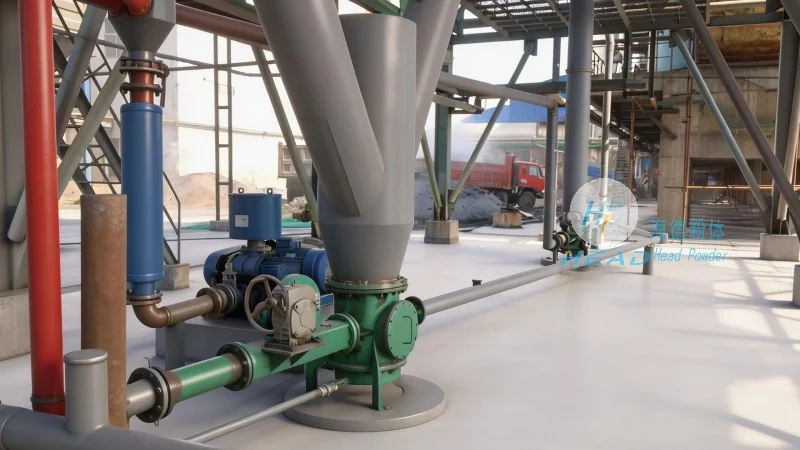
The intelligent tonne bag loading station is composed of several critical components that work in tandem to achieve seamless material transfer. These include the bag opening and discharge mechanism, the pneumatic conveying pipeline system, the material separation and cleaning unit, and the control system. Each component is engineered to optimize performance and reliability, ensuring consistent operation under various industrial conditions. The bag opening mechanism is designed to safely and efficiently open tonne bags, while the discharge system ensures that the material is transferred into the conveying pipeline without blockages or spills. The pneumatic pipeline network, equipped with appropriate valves and regulators, manages the air flow and pressure required for effective material transport. The material separation unit, such as cyclones or filters, prevents dust and debris from entering downstream equipment, maintaining product purity and system longevity. The control system, integrated with sensors and automation technology, monitors and adjusts the entire process in real-time, enhancing operational efficiency and reducing human error.
Operation Process of the Material Handling System
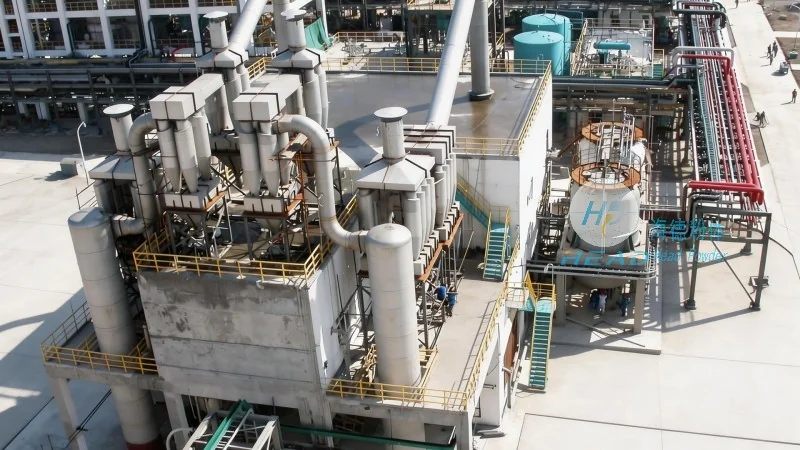
The operation of the intelligent tonne bag loading station begins with the placement of a tonne bag onto the loading platform. The system's sensors detect the bag's presence and initiate the opening sequence. The bag opening mechanism, typically a hydraulic or mechanical device, safely cuts and opens the bag, allowing the material to fall into the discharge hopper. The discharge hopper is connected to the pneumatic conveying pipeline, which uses compressed air to draw the material into the system. The air flow is controlled by a pressure regulator and valve system, ensuring that the material is conveyed at an optimal velocity without causing excessive wear on the pipeline or equipment. As the material travels through the pipeline, it passes through the material separation unit, where any fines or dust are removed and collected for recycling or disposal. The cleaned material then reaches the processing equipment, such as a mixer or reactor, where it is further processed according to the production requirements. The entire process is automated, with the control system continuously monitoring parameters like air pressure, material flow rate, and system temperature to maintain stable operation. In case of any anomalies, such as blockages or pressure drops, the system automatically triggers alarms and initiates corrective actions, preventing downtime and ensuring continuous production.
Working Principle of Pneumatic Conveying Technology
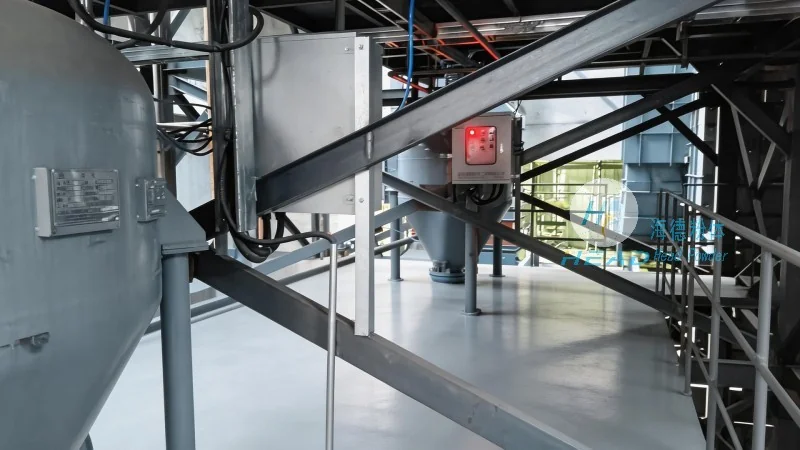
The core of the intelligent tonne bag loading station is the pneumatic conveying principle, which utilizes compressed air to transport bulk materials through a pipeline. This technology operates on the principle of creating a pressure differential between the conveying line and the ambient environment. When compressed air is introduced into the conveying line, it creates a low-pressure zone that draws the material into the pipeline. The material is then carried by the air stream, moving through the pipeline to the destination point. The velocity of the air and the size of the particles determine the conveying efficiency and system design. For fine powders, low-velocity conveying is often used to minimize particle degradation and system wear, while for larger particles, higher velocities may be required to prevent blockages. The system's design, including the pipeline diameter, length, and bends, is carefully calculated to ensure that the material is conveyed smoothly without excessive pressure losses or particle separation. The control system plays a crucial role in managing the air flow and pressure, adjusting parameters in real-time to adapt to changes in material characteristics or system conditions. This dynamic control ensures that the conveying process remains efficient and reliable, even with varying material types or production demands.
Advantages of the Intelligent Tonne Bag Loading Station
The intelligent tonne bag loading station material pneumatic conveying machine offers several advantages over traditional material handling methods. Firstly, it significantly reduces manual labor, as the entire process is automated from bag opening to material transfer. This not only improves operational efficiency but also enhances workplace safety by minimizing the risk of manual handling of heavy or hazardous materials. Secondly, the system ensures high accuracy in material measurement and transfer, reducing waste and improving product consistency. The automated control system maintains consistent flow rates and pressure levels, preventing over- or under-conveying of materials. Thirdly, the equipment is designed for easy maintenance and cleaning, with components that can be easily accessed and serviced. The material separation unit and cleaning mechanisms help maintain system hygiene, reducing the risk of contamination and ensuring product quality. Additionally, the system's compact design and modular components allow for flexible installation and integration into existing industrial facilities, making it suitable for various production environments. The use of advanced sensors and automation technology also enables real-time monitoring and data collection, providing valuable insights for process optimization and predictive maintenance.
Application Scenarios and Industry Impact
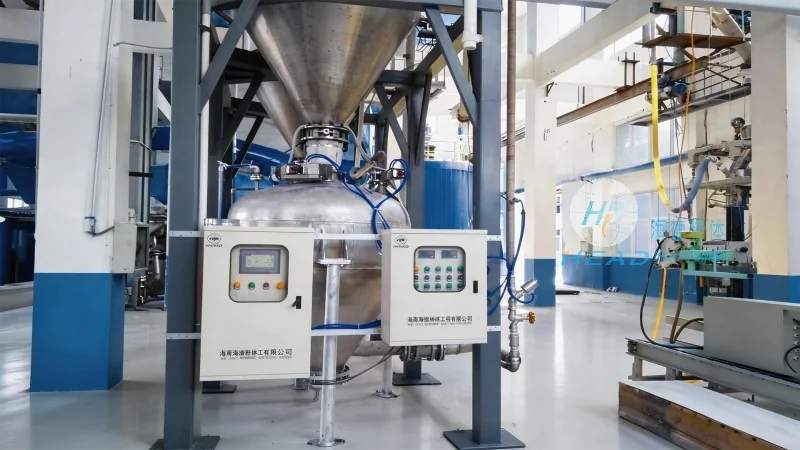
The intelligent tonne bag loading station is widely used in various industries, including chemical, pharmaceutical, food, and mining. In the chemical industry, it is used to handle powders and granules for production processes such as mixing, coating, and compounding. The pharmaceutical industry benefits from the system's ability to maintain high purity and prevent contamination, ensuring compliance with regulatory standards. The food industry utilizes the equipment for handling ingredients like flour, sugar, and spices, where hygiene and product quality are paramount. In the mining sector, the system is employed to transport bulk materials like ores and minerals from storage to processing equipment. The consistent and efficient material transfer provided by the intelligent tonne bag loading station enhances overall production efficiency and reduces operational costs in these industries. By streamlining the material handling process, the equipment contributes to improved productivity, reduced downtime, and enhanced product quality, making it a valuable asset for modern industrial operations.




