HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for diverse industrial applications. Among their portfolio is a sophisticated dry cobblestone material pneumatic conveying system, which efficiently handles the transportation of dry cobblestone materials from source to destination without the need for traditional bulk handling methods.
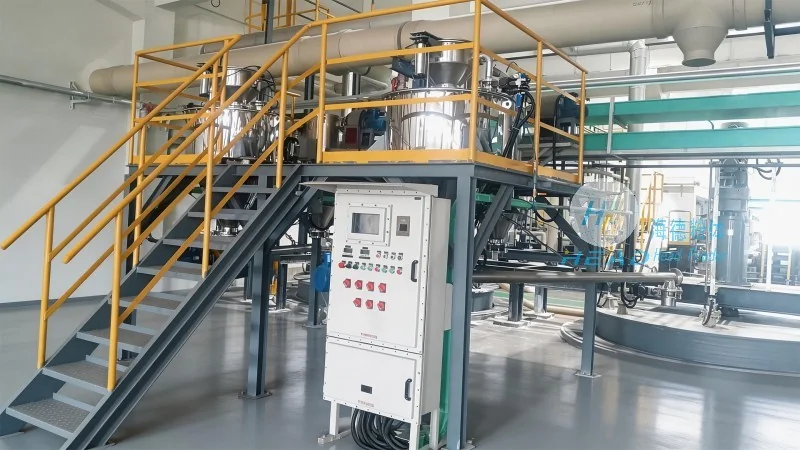
Overview of the Dry Cobblestone Material Pneumatic Conveying System
The dry cobblestone material pneumatic conveying system developed by HeadPowder is engineered to address the unique challenges associated with transporting dry cobblestone materials, such as irregular shapes, varying sizes, and abrasive properties. This system utilizes a combination of positive pressure and negative pressure conveying techniques to ensure reliable and efficient material movement. The system is designed to minimize material degradation, reduce operational costs, and enhance overall process efficiency in industrial settings.
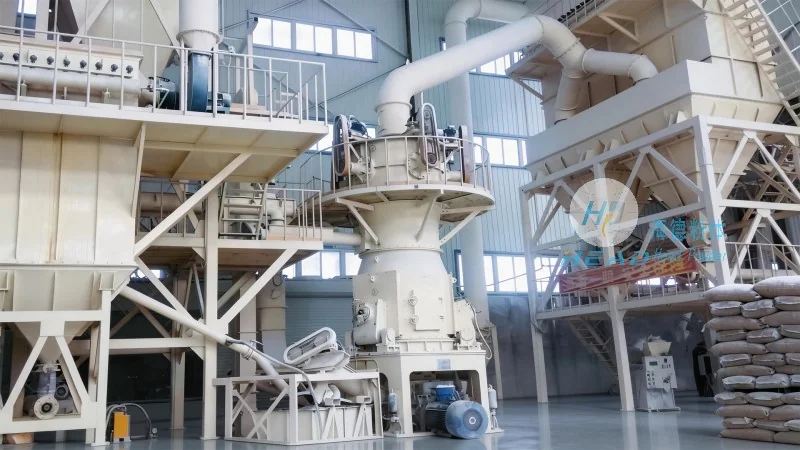
Key Components and Their Functions
The pneumatic conveying system consists of several critical components that work in tandem to achieve seamless material transport. These include a material hopper for storage and feeding, a rotary airlock valve to control the flow of dry cobblestone material into the conveying line, a positive pressure blower or air compressor to generate the necessary air pressure, a conveying pipeline network that transports the material, and a receiver or discharge hopper at the destination. Each component plays a vital role in maintaining the system's performance and ensuring consistent operation.
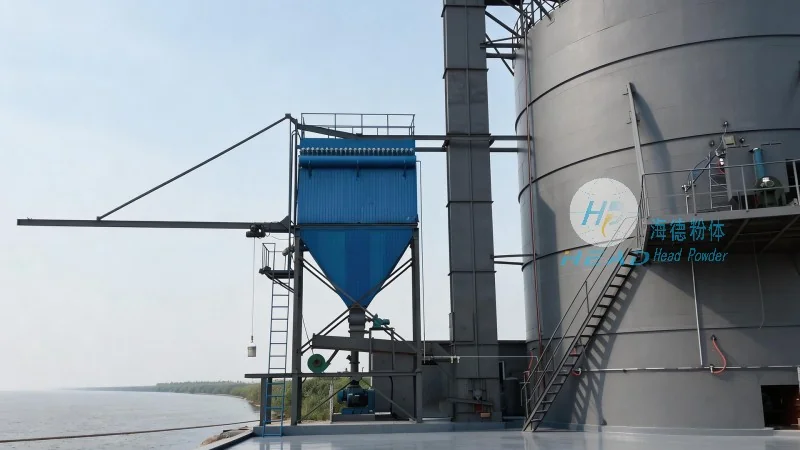
Working Principle of the System
The operation of the dry cobblestone material pneumatic conveying system begins with the loading of dry cobblestone material into the material hopper. The rotary airlock valve then regulates the material flow, allowing a controlled amount of material to enter the conveying pipeline. Simultaneously, the positive pressure blower generates a high-pressure air stream that propels the material through the pipeline. As the material travels, it is suspended and carried by the air flow, preventing blockages and ensuring smooth transport. At the destination, the material is discharged into the receiver hopper, where the air is separated from the material through a cyclone or other separation device. The separated air is then returned to the blower for reuse, while the dry cobblestone material is collected for further processing or storage.
Operation Process and Flow Control
The system's operation follows a systematic process to ensure optimal performance and material handling. The material is first fed from the hopper into the rotary airlock valve, which acts as a gate to control the flow rate. The air compressor then supplies compressed air to the conveying line, creating a pressure differential that drives the material forward. The conveying pipeline is typically made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of dry cobblestone materials. The receiver hopper is equipped with a discharge valve to regulate the outflow of material, ensuring that the system operates at a consistent rate. The entire process is monitored by sensors and control systems that adjust the air pressure and material flow as needed to maintain efficiency and prevent system failures.
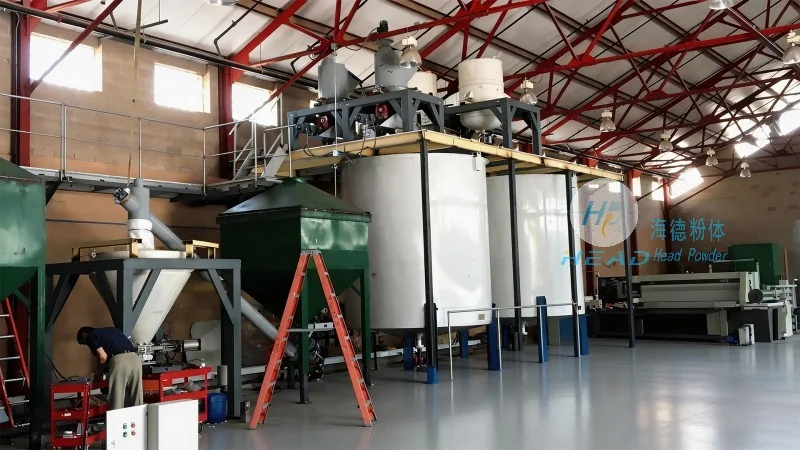
Advantages and Applications
HeadPowder's dry cobblestone material pneumatic conveying system offers several advantages over traditional bulk handling methods. These include reduced labor costs, minimized material loss, improved safety by eliminating manual handling, and enhanced process control. The system is particularly suitable for industries such as construction, mining, and landscaping, where dry cobblestone materials are commonly used. It can be customized to handle various material types and flow rates, making it a versatile solution for different industrial applications.




