HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for fine chemical applications. Based in Shandong, China, the company leverages decades of expertise to deliver reliable and efficient equipment that meets the stringent requirements of the fine chemical industry.
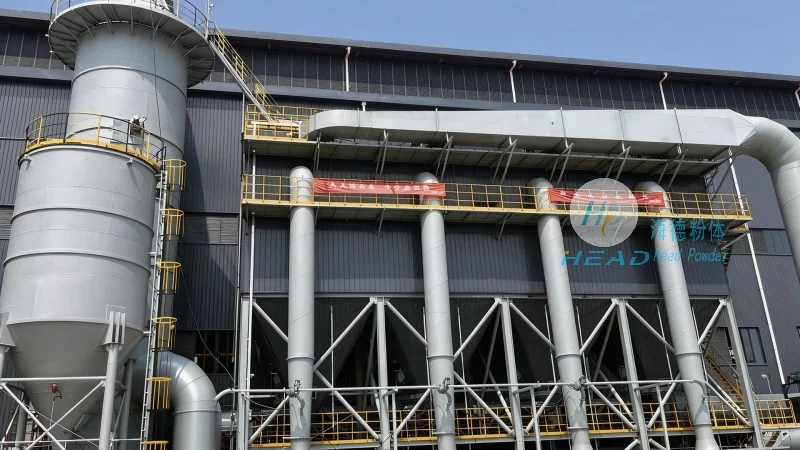
At the core of our product line is the fine chemical powder pneumatic conveying machine, which utilizes air as the primary medium to transport dry powders over long distances with minimal product degradation. This technology is particularly critical for industries dealing with sensitive materials, where maintaining product integrity and preventing contamination is paramount.
Working Principle of Pneumatic Conveying Systems
The pneumatic conveying process operates on the principle of transporting solid particles through a pipeline using a moving gas stream. In the case of fine chemical powders, the system typically employs a positive pressure or negative pressure (or a combination of both) to move the material. The key components include a hopper for material storage, a feeder to control the flow rate, a compressor or vacuum pump to generate the air flow, and a pipeline network that transports the powder to the destination.
When the system is activated, the feeder releases the fine chemical powder into the pipeline, where it is entrained by the high-velocity air stream. The air-powder mixture travels through the pipeline, often with the assistance of bends, valves, and other components that ensure smooth flow and prevent blockages. The destination equipment, such as a silo, reactor, or packaging unit, then receives the material through a receiving hopper or valve.
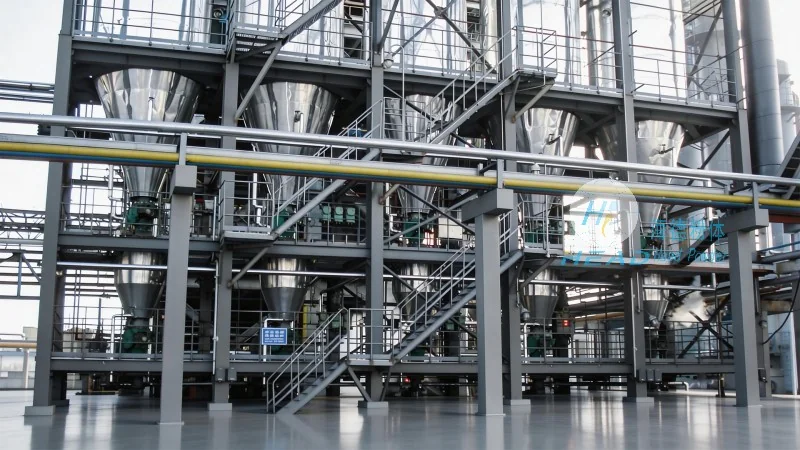
Step-by-Step Operation Process
The operation of a fine chemical powder pneumatic conveying machine involves several sequential steps, each designed to ensure optimal performance and product quality. The process begins with material loading into the hopper, where the powder is stored under controlled conditions to prevent caking or agglomeration.
Next, the feeder system activates, metering the powder at a consistent rate to match the air flow. The compressor then generates the necessary pressure or vacuum, depending on the system configuration. As the air stream moves through the pipeline, it carries the fine chemical powder, maintaining a stable mixture that prevents particle separation or settling.
During transit, the pipeline may include features such as cyclones or filters to separate any entrained air from the powder, ensuring that the delivered material is free of contaminants. The receiving equipment then processes the material, either by storing it in a silo for later use or by feeding it directly into a production line.
Key Advantages and Applications
For the fine chemical industry, pneumatic conveying offers several advantages over traditional methods like belt conveyors or screw conveyors. These include reduced product contamination, as the material is never in direct contact with metal or other surfaces, and the ability to transport materials over long distances without the need for multiple transfer points. Additionally, the system is highly flexible, allowing for easy integration with existing production lines and the ability to handle a wide range of powder properties, from low to high density.
HeadPowder's fine chemical powder pneumatic conveying machines are specifically engineered to address the unique challenges of the fine chemical sector. The equipment is designed with materials that are compatible with a variety of chemicals, ensuring that the product remains pure and unaltered throughout the conveying process. The company's commitment to quality and precision is evident in the robust construction and advanced control systems that are standard features of their machines.




