Efficient and reliable fertilizer granule material conveying equipment is crucial for modern agricultural operations, ensuring that granular fertilizers are transported safely and efficiently from production sites to storage or application areas. The operation process of such equipment involves a series of integrated steps designed to maintain product integrity and operational efficiency.
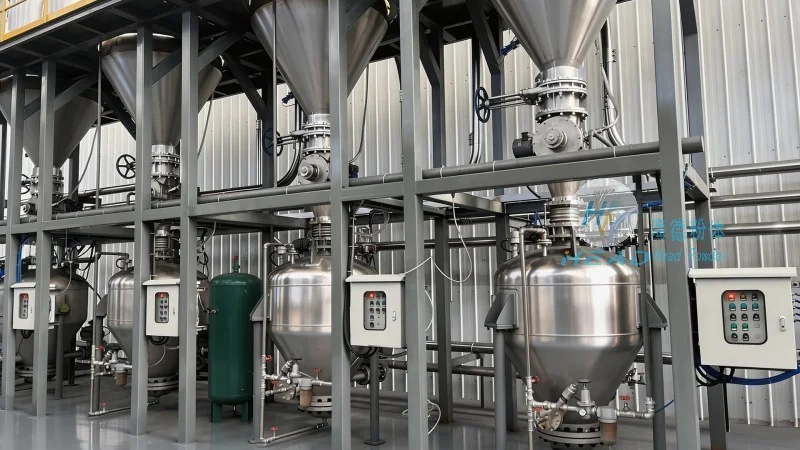
Overview of the Conveying Equipment System
The fertilizer granule material conveying equipment typically consists of several key components, including feed hoppers, conveyor belts or screw conveyors, control systems, and safety mechanisms. Each component plays a vital role in the overall operation, working in tandem to facilitate the smooth movement of granular materials. The system is engineered to handle various types of fertilizer granules, from nitrogen-based to phosphorus or potassium formulations, while maintaining consistent flow rates and minimizing material degradation.
Step-by-Step Operation Process
The operation process begins with the loading of fertilizer granules into the feed hopper. The hopper is designed with a sloped surface to ensure uniform material distribution and prevent clogging. Once the hopper is filled, the material is fed into the conveyor system, which may use a belt or screw mechanism to transport the granules along a designated path. The conveyor speed is controlled by an automated system that adjusts based on the material load and desired output rate. As the granules move through the conveyor, they are monitored for any blockages or irregularities, with sensors triggering alarms or adjustments to maintain optimal performance.
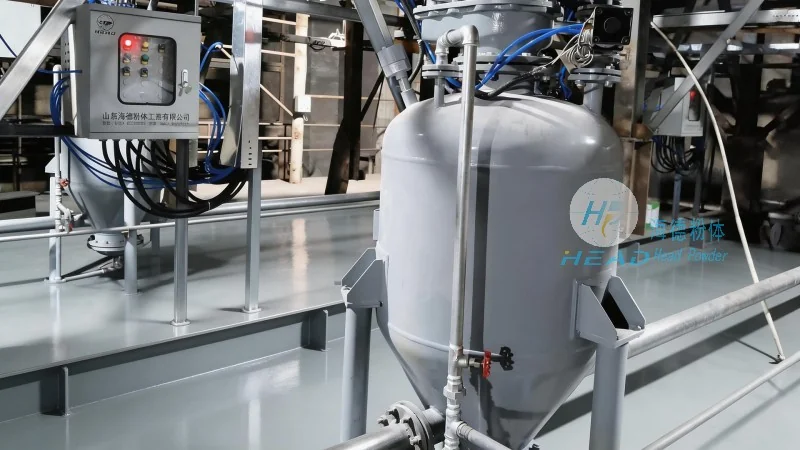
During the conveying process, the equipment may incorporate additional features such as vibration screens or air classifiers to separate oversized or undersized granules, ensuring that only the desired particle size reaches the final destination. This quality control step is critical for maintaining product specifications and meeting customer requirements. The conveyor system is also equipped with dust suppression mechanisms to minimize airborne particles and protect both the material and the surrounding environment.
Working Principle of the Conveying Mechanism
The core working principle of fertilizer granule material conveying equipment revolves around the application of mechanical force to move granular materials. For belt conveyors, the system uses a motor-driven pulley to rotate the conveyor belt, which transports the granules through friction and gravity. The belt is typically made of durable materials, such as rubber or polyurethane, to withstand the abrasive nature of fertilizer granules and resist wear and tear over time. Screw conveyors, on the other hand, utilize a rotating screw to push the granules forward, creating a positive displacement effect that ensures continuous movement even in vertical or inclined orientations.
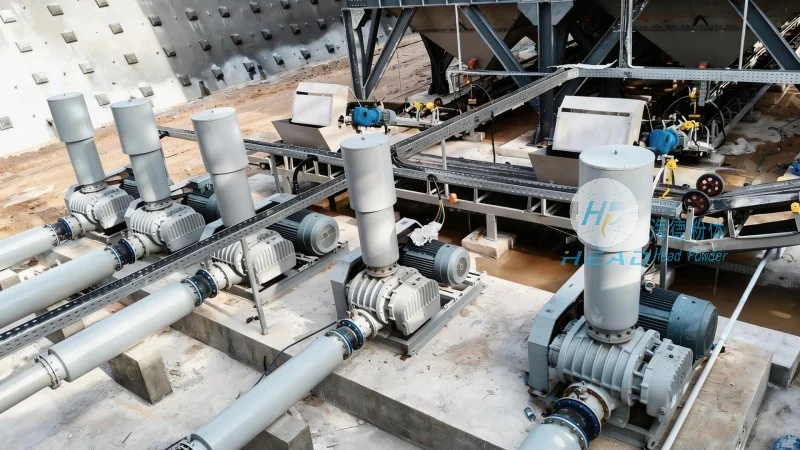
The control system of the equipment is integral to its operation, as it manages variables such as speed, pressure, and temperature to optimize performance. Sensors and feedback mechanisms continuously monitor the system's status, adjusting parameters in real-time to prevent overloading or underperformance. This closed-loop control ensures that the conveying process remains stable and efficient, even under varying load conditions. Additionally, the equipment is designed with safety features, including emergency stop buttons and overload protection, to safeguard operators and prevent equipment damage.
Key Features and Benefits
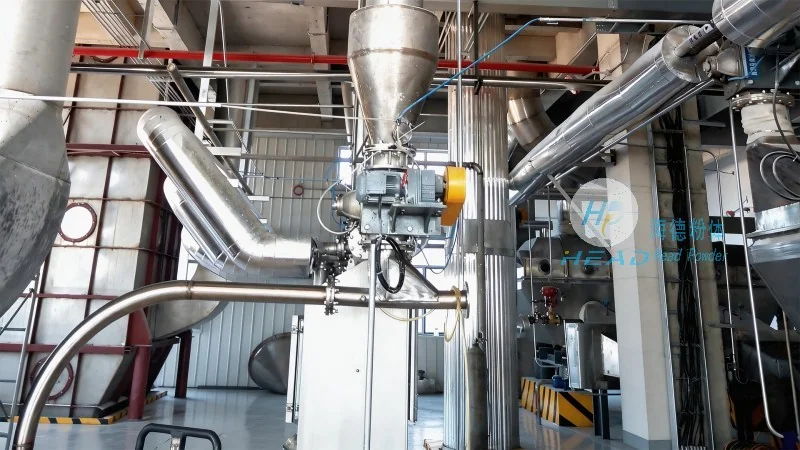
Modern fertilizer granule material conveying equipment from Shandong HeadPowder Engineering Co., Ltd. incorporates advanced technologies to enhance operational efficiency and product quality. These features include variable speed drives, which allow for precise control of conveyor speed, and automated material level sensors, which prevent overfilling and ensure consistent feeding. The equipment also utilizes corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of fertilizers and extend service life. By integrating these features, the conveying system minimizes downtime, reduces maintenance costs, and improves overall productivity.
Company Information and Location
HeadPowder, a leading manufacturer of fertilizer processing equipment, is based in Shandong, China. The company specializes in designing and manufacturing high-quality conveying systems tailored to the specific needs of the agricultural industry. With a strong commitment to innovation and customer satisfaction, HeadPowder provides reliable solutions for fertilizer granule transportation, ensuring that farmers and agricultural businesses can efficiently manage their fertilizer supply chains. The company's facilities in Shandong are equipped with state-of-the-art technology and skilled personnel, enabling them to deliver superior products and services to clients worldwide.




