Efficient and reliable sulfur material handling equipment is crucial in various industrial applications, particularly in the chemical and mining sectors. These systems are designed to transport sulfur, a versatile and widely used element, from storage to processing units with precision and safety. Understanding the operation process and working principle of such equipment is essential for optimizing industrial workflows and ensuring operational efficiency.
Overview of Sulfur Material Handling Equipment
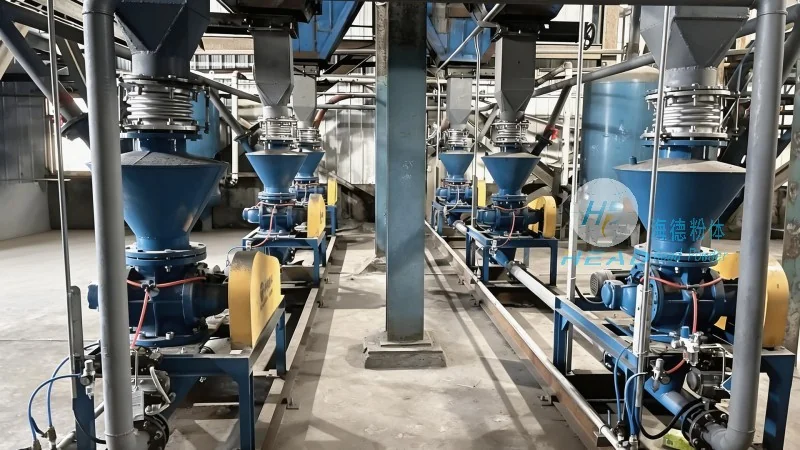
Sulfur material handling equipment encompasses a range of machinery and systems engineered to manage the transportation, storage, and processing of sulfur. This includes conveyor systems, bulk material handling equipment, and specialized handling tools tailored to the unique properties of sulfur, such as its solid or liquid state under different temperature conditions. The equipment is typically designed to handle large volumes of sulfur while maintaining safety standards and operational reliability.
The Operation Process of Sulfur Material Handling Equipment
The operation process of sulfur material handling equipment involves several key steps that ensure the smooth and efficient transfer of sulfur from its source to the processing unit. The process begins with the loading of sulfur into the handling system, which may involve bulk storage silos or direct loading from production facilities. Once loaded, the equipment uses mechanical or pneumatic systems to transport the sulfur through a network of conveyors, pipelines, or containers. The system is equipped with sensors and control mechanisms to monitor the flow rate, temperature, and pressure, ensuring that the material is handled under optimal conditions. The final step involves the unloading of sulfur into the processing unit, where it is further refined or utilized in various industrial applications.
Working Principle of Sulfur Material Handling Equipment
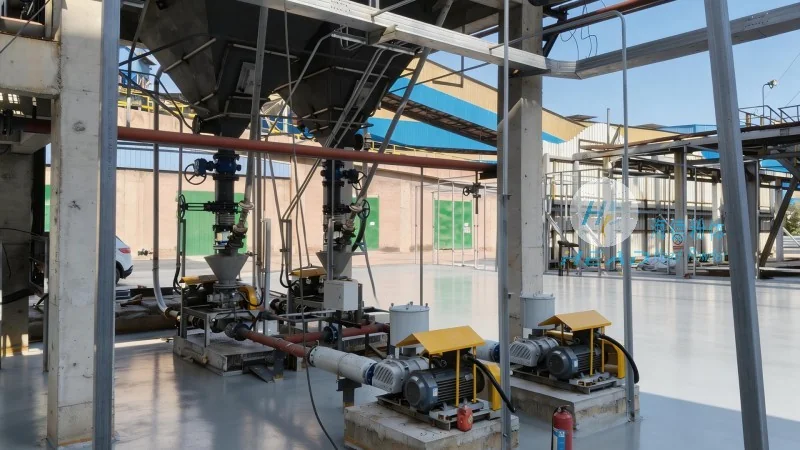
The working principle of sulfur material handling equipment is based on mechanical and hydraulic systems that facilitate the movement of sulfur. Conveyor systems, for instance, use rollers or belts to transport solid sulfur, while pneumatic systems employ compressed air to move powdered or granular sulfur through pipelines. The equipment is designed with materials that are resistant to sulfur's corrosive properties, such as stainless steel or specialized coatings, to prevent degradation and ensure longevity. Additionally, the systems incorporate safety features like temperature controls and emergency shut-off mechanisms to prevent accidents and maintain operational safety.
Key Components and Their Functions
Several key components contribute to the effective operation of sulfur material handling equipment. These include loading hoppers, which collect and feed sulfur into the system; conveyors, which transport the material; and unloading mechanisms, which release the sulfur into processing units. Control panels and monitoring systems are also integral, providing real-time data on the equipment's performance and enabling operators to adjust parameters as needed. The use of advanced materials and engineering techniques ensures that each component works in harmony to achieve efficient and safe sulfur handling.
Applications and Industries
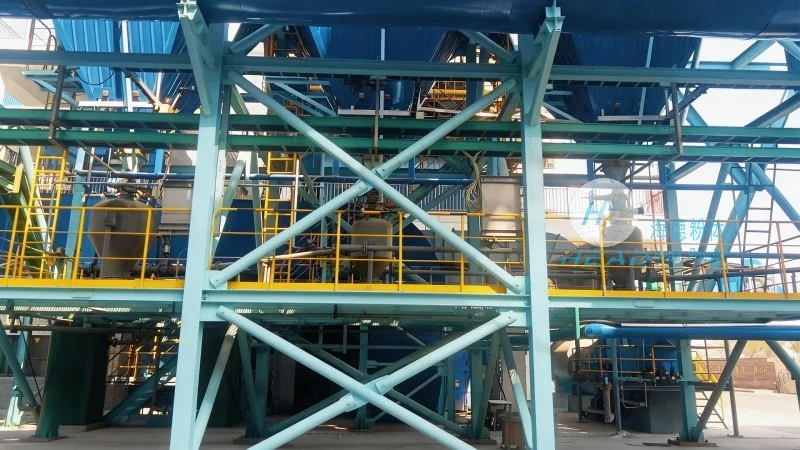
Sulfur material handling equipment is widely used in industries such as chemical manufacturing, mining, and energy production. In chemical plants, it is used to transport sulfur for the production of sulfuric acid and other sulfur-based compounds. In mining operations, it helps in the extraction and processing of sulfur from ore deposits. The equipment is also utilized in the energy sector for the handling of sulfur in power plants and refineries. Its versatility makes it a critical component in various industrial processes that rely on sulfur as a raw material.
Benefits of Using Sulfur Material Handling Equipment
Implementing sulfur material handling equipment offers numerous benefits to industrial operations. These include increased efficiency in material transport, reduced labor costs, and improved safety through automated systems. The equipment minimizes the risk of human error and accidents associated with manual handling of sulfur, which can be hazardous due to its corrosive nature. Additionally, the systems are designed to handle large volumes of sulfur, reducing the need for frequent stops and maintenance, thereby enhancing overall productivity. The use of advanced technology also allows for better monitoring and control, leading to more consistent and reliable performance.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
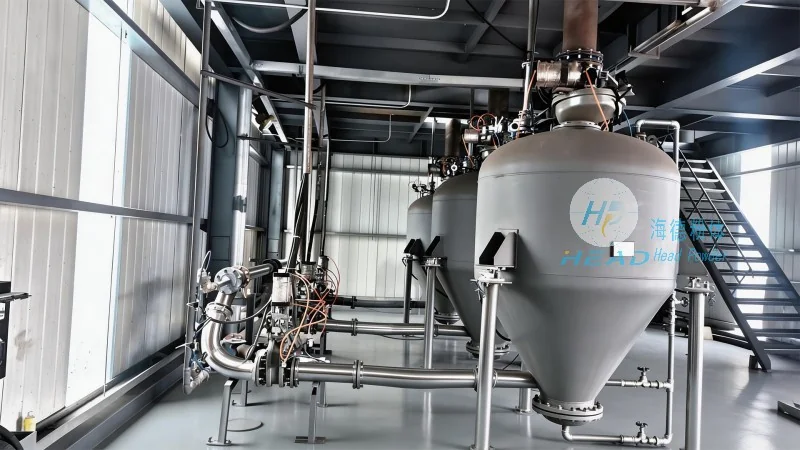
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of sulfur material handling equipment. With its headquarters in Shandong, China, the company specializes in designing, manufacturing, and installing customized equipment tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians leverages advanced technology and industry expertise to develop solutions that meet the highest standards of efficiency, safety, and durability. The company's commitment to quality and customer satisfaction has made it a trusted partner in the sulfur handling industry, providing reliable equipment that enhances industrial operations worldwide.
Conclusion
In conclusion, sulfur material handling equipment plays a vital role in modern industrial processes, ensuring the efficient and safe transportation of sulfur. The operation process and working principle of such equipment are designed to optimize performance while maintaining safety standards. Companies like Shandong HeadPowder Engineering Co., Ltd. continue to innovate and improve these systems, providing industries with reliable solutions that enhance productivity and operational efficiency. As the demand for sulfur-based products grows, the importance of advanced material handling equipment will only increase, making it a critical component in the future of industrial operations.




