Intelligent centralized material handling systems represent a sophisticated solution for optimizing material transport and logistics within industrial environments. These systems are designed to enhance efficiency, reduce operational costs, and improve overall workflow management by integrating advanced technologies such as automation, real-time monitoring, and intelligent control. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the development and implementation of such systems, leveraging years of expertise to deliver tailored solutions for diverse industrial applications.
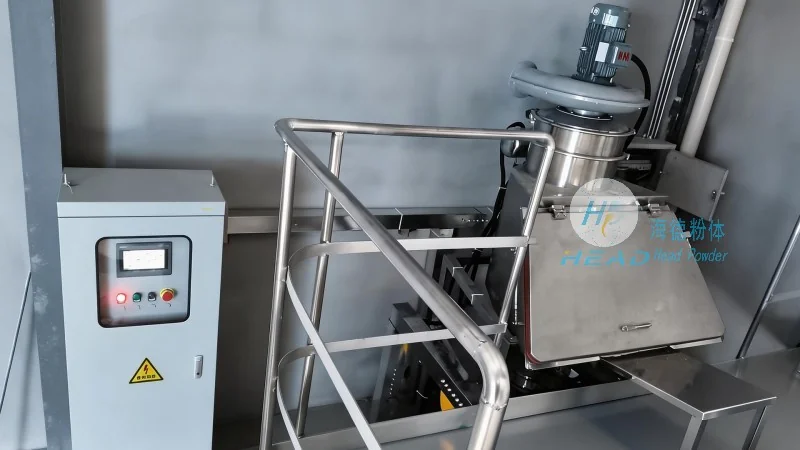
Overview of Intelligent Centralized Material Handling Systems
At the core of intelligent centralized material handling is the concept of consolidating material transport from multiple sources into a centralized system. This approach eliminates the need for separate, individual transport routes, thereby streamlining operations and minimizing bottlenecks. The systems typically consist of components like automated guided vehicles (AGVs), conveyor networks, robotic arms, and advanced software platforms that work in tandem to manage the movement of materials from storage to processing areas and back. The integration of these elements allows for real-time tracking and dynamic rerouting, ensuring that materials are handled efficiently and with minimal human intervention.
Key Components and Their Roles
The effectiveness of intelligent centralized material handling systems relies on several critical components. First, automated guided vehicles (AGVs) or automated mobile robots (AMRs) are used to transport materials between different locations within the facility. These vehicles are equipped with sensors and navigation systems that enable them to move autonomously, avoiding obstacles and following pre-programmed paths. Second, conveyor systems, including belt conveyors, roller conveyors, and sortation conveyors, are employed to move materials horizontally or vertically, facilitating the transfer of goods between different levels or areas. Third, robotic arms and pick-and-place systems are utilized for tasks such as loading, unloading, and sorting, enhancing the precision and speed of material handling. Finally, a centralized control system, often based on a cloud or on-premise server, manages all operations, monitors performance, and adjusts parameters in real time to optimize efficiency.
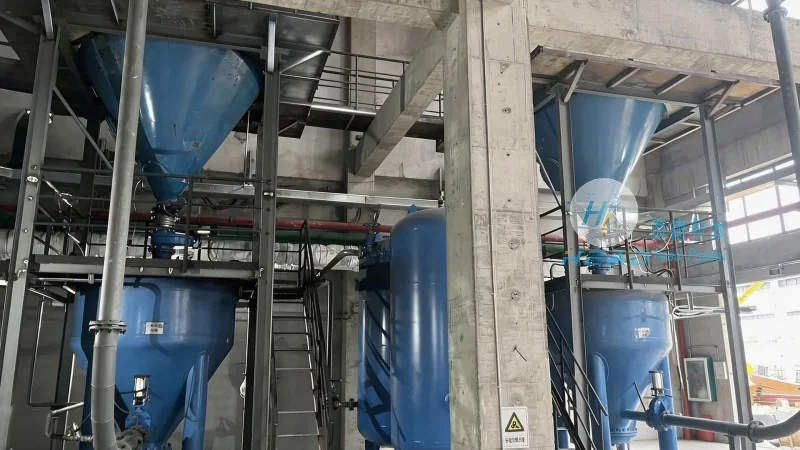
Operation Process: From Input to Output
The operation process of intelligent centralized material handling systems begins with the receipt of materials at the input point. Materials are typically stored in a warehouse or storage area, and the system uses sensors and software to identify and track each item. Once a material is identified, the control system determines the optimal path for transport. The AGVs or AMRs then pick up the material and transport it to the designated processing or storage location. During this process, the system continuously monitors the status of the material, including its position, temperature, and condition, ensuring that it is handled appropriately. Upon arrival at the destination, the material is either transferred to a conveyor system for further processing or placed into storage. The system then updates its database to reflect the new location of the material, enabling real-time tracking and inventory management.
Working Principle: Integration of Automation and Intelligence
The working principle of intelligent centralized material handling systems is centered on the integration of automation and artificial intelligence to achieve intelligent material transport. The system uses a combination of hardware and software to create a closed-loop control environment. The hardware components, including AGVs, conveyors, and robotic arms, perform the physical tasks of moving and handling materials. The software components, such as the control system and monitoring platforms, process data from various sensors and devices, analyze it, and make decisions to optimize operations. For example, the system can use predictive analytics to anticipate demand and adjust the flow of materials accordingly, or use machine learning algorithms to improve the efficiency of path planning and task allocation. This integration allows the system to adapt to changing conditions, such as increased demand or equipment failures, and maintain optimal performance.
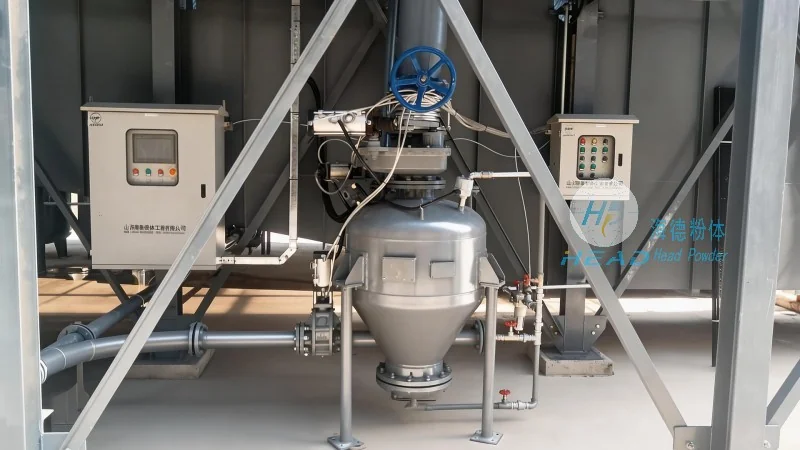
Benefits and Applications
Intelligent centralized material handling systems offer numerous benefits to industrial operations. These include increased efficiency through reduced travel time and minimized bottlenecks, lower labor costs due to automation, improved safety by reducing human involvement in hazardous tasks, and enhanced inventory management through real-time tracking. The systems are widely used in various industries, including manufacturing, logistics, pharmaceuticals, and food processing. For instance, in a manufacturing plant, the system can transport raw materials from storage to production lines and finished products to packaging areas, ensuring a smooth and continuous workflow. In a logistics facility, the system can handle the sorting and distribution of packages, improving delivery times and reducing errors. The adaptability of these systems allows them to be customized to meet the specific needs of different industries and facilities.
Conclusion
Intelligent centralized material handling systems represent a significant advancement in industrial logistics, offering a comprehensive solution to the challenges of material transport and management. By leveraging advanced technologies and intelligent control, these systems enhance operational efficiency, reduce costs, and improve overall productivity. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and develop cutting-edge solutions to meet the evolving needs of industrial clients. With its headquarters in Shandong, China, the company remains committed to delivering high-quality, reliable systems that help businesses achieve their operational goals and stay competitive in the global market.




