Quartz sand granular pneumatic conveying system equipment is a specialized industrial device designed for the efficient transportation of quartz sand particles through an air-based system. This technology is widely used in various industries, including mining, construction, and manufacturing, where the reliable and safe movement of bulk materials is crucial. The system combines advanced engineering principles with robust construction to ensure optimal performance under diverse operational conditions.
Key Components of the Pneumatic Conveying System
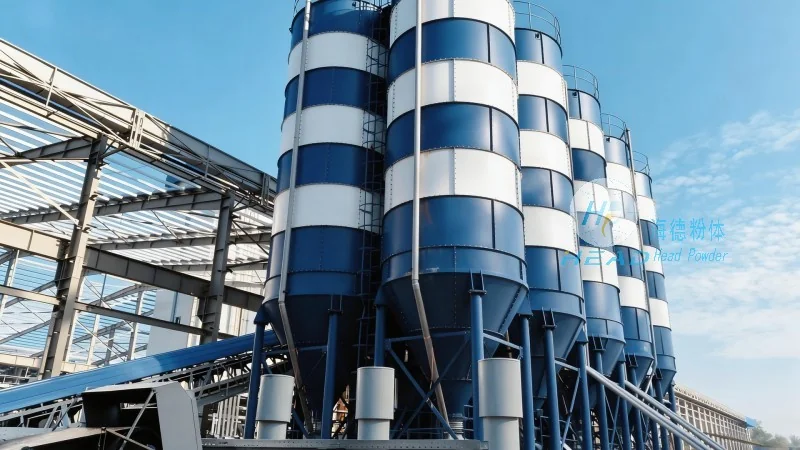
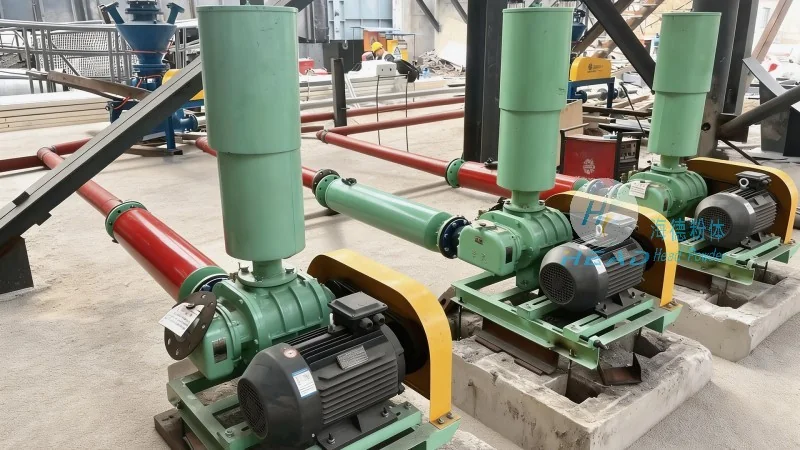
The quartz sand granular pneumatic conveying system consists of several critical components that work in tandem to achieve effective material transport. These components include the hopper for material storage, the air compressor or blower that generates the necessary air pressure, the conveying pipeline network, the control valves and regulators for flow management, and the discharge unit where the material is released. Each component plays a vital role in maintaining the system's efficiency and safety.
Working Principle of the Pneumatic Conveying Process
The operation of the quartz sand granular pneumatic conveying system is based on the principle of air suspension, where the quartz sand particles are entrained and transported by a high-velocity air stream. The process begins with the material being fed into the hopper, where it is then drawn into the conveying pipeline by the air flow generated by the compressor. The air pressure and velocity are carefully controlled to ensure that the quartz sand particles remain suspended in the air, preventing blockages and ensuring smooth transport. The system uses either positive pressure or negative pressure (or a combination of both) depending on the specific application requirements. The positive pressure system pushes the air and material through the pipeline, while the negative pressure system pulls the material from the source and draws it into the pipeline.
Operation Process of the Quartz Sand Pneumatic Conveying System
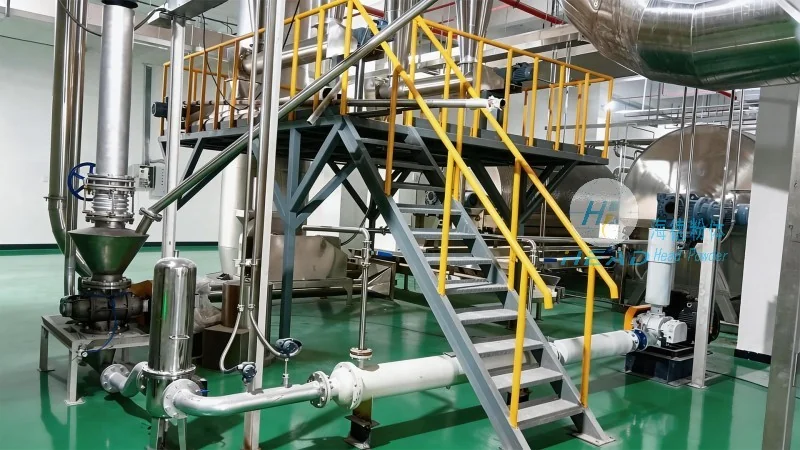
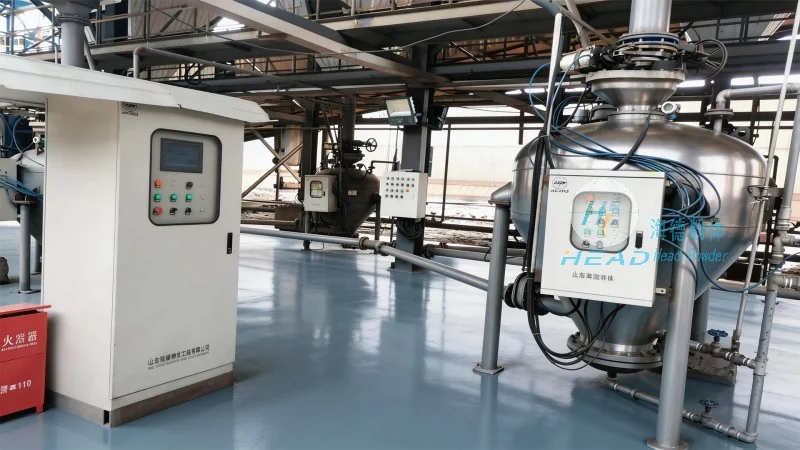
The operation process of the quartz sand granular pneumatic conveying system involves several sequential steps that ensure the efficient and safe movement of the material. First, the quartz sand is loaded into the hopper, which is equipped with a feeding mechanism such as a screw feeder or a rotary valve to control the material flow rate. Next, the air compressor or blower is activated, generating the required air pressure and flow rate. The air is then introduced into the conveying pipeline, creating a high-velocity stream that entrains the quartz sand particles. The material is transported through the pipeline to the discharge point, where it is released into the receiving container or processing unit. The system's control panel monitors and adjusts the air pressure, flow rate, and material feed rate in real-time to maintain optimal performance. This closed-loop control system ensures that the conveying process is consistent and reliable, minimizing downtime and maximizing productivity.
Advantages of Using Quartz Sand Granular Pneumatic Conveying System
Implementing a quartz sand granular pneumatic conveying system offers several advantages over traditional material handling methods. One of the primary benefits is the ability to transport the material over long distances without the need for intermediate transfer points or manual handling. This reduces labor costs and minimizes the risk of material contamination or loss. Additionally, the system is highly flexible, allowing for easy integration with existing production lines and the ability to adjust the conveying rate based on production demands. The enclosed pipeline design also prevents dust emissions, improving workplace safety and compliance with environmental regulations. Furthermore, the system's low maintenance requirements and long service life contribute to overall cost savings and operational efficiency.
Applications of Quartz Sand Granular Pneumatic Conveying System
The quartz sand granular pneumatic conveying system is widely used in various applications where the efficient handling of quartz sand is essential. In the mining industry, it is used to transport mined quartz sand from the extraction site to processing facilities, ensuring a continuous supply of raw material. In the construction industry, the system is employed to deliver quartz sand to concrete mixing plants and other construction sites, where it is used as a key ingredient in concrete production. The manufacturing industry also utilizes this system to transport quartz sand to grinding and polishing machines, where it is used as an abrasive material. Additionally, the system is suitable for use in chemical and pharmaceutical applications where the material needs to be handled in a clean and controlled environment.
Conclusion and Company Information
Quartz sand granular pneumatic conveying system equipment, as provided by Shandong HeadPowder Engineering Co., Ltd., represents a reliable and efficient solution for the transportation of bulk quartz sand materials. With its advanced design and robust construction, the system ensures optimal performance, safety, and productivity in various industrial applications. The company, known as headpowder, is committed to delivering high-quality equipment and services to meet the diverse needs of its clients. Located in Shandong, China, headpowder leverages its expertise in engineering and manufacturing to provide tailored solutions for material handling challenges. By choosing the quartz sand granular pneumatic conveying system from headpowder, industries can enhance their operational efficiency, reduce costs, and ensure the safe and reliable handling of quartz sand.




