Operation Process and Working Principle of Mineral Sand Pneumatic Conveying Equipment
Release time:2026-09-20 10:01:34
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying systems tailored for mineral sand applications. With a strong commitment to engineering excellence and customer satisfaction, the company has established itself as a reliable partner in the material handling industry.
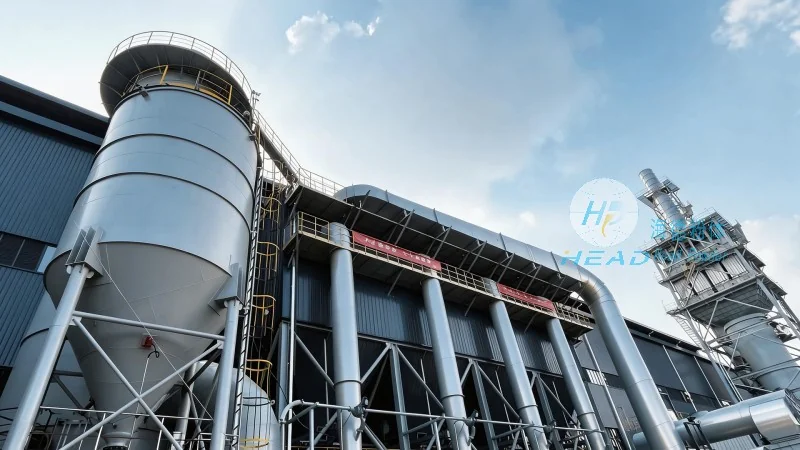
Introduction to Mineral Sand Pneumatic Conveying Equipment
Mineral sand pneumatic conveying equipment is a sophisticated system engineered to transport bulk materials like mineral sands through an air-driven process. This technology offers a highly efficient and flexible solution for moving materials over short to medium distances, ensuring minimal product degradation and operational reliability. The system typically comprises a hopper, a conveying line, a separator, and a discharge unit, all working in tandem to achieve seamless material transfer.
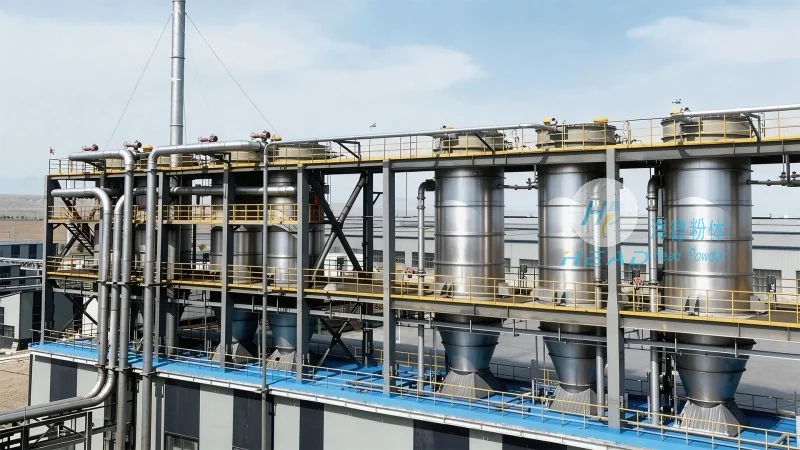
Operation Process of the Pneumatic Conveying System
The operation of a mineral sand pneumatic conveying machine begins with the material being fed into the hopper. As the material accumulates, it is drawn into the conveying line by a high-pressure air stream generated by a blower or compressor. The air and material mixture travels through the pipeline, reaching the separator where the air is separated from the solid particles. The mineral sand is then discharged into the target container, while the air is either recirculated or vented, depending on the system design. This continuous process ensures a steady flow of material, minimizing downtime and maximizing productivity. The system’s design also minimizes product exposure to external contaminants, preserving the quality of the mineral sand during transport.
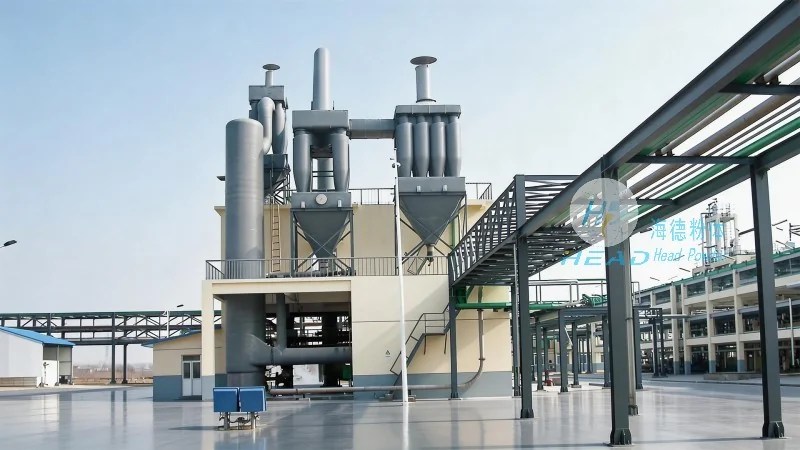
Working Principle of the Equipment
The core of the pneumatic conveying system lies in the interaction between the air flow and the material particles. The system operates on the principle of fluidization, where the air velocity is sufficient to lift and transport the mineral sand particles. The blower creates a pressure differential that pulls the material from the hopper into the pipeline. The conveying line is designed with appropriate diameters and bends to minimize pressure loss and maintain consistent air velocity. The separator uses centrifugal force or other mechanisms to separate the air from the solid material, ensuring that the mineral sand is delivered to the discharge point without contamination. This integrated approach ensures efficient material handling while maintaining product integrity. The air flow management is critical, as it directly impacts the conveying capacity and the overall system efficiency.




