Shandong HeadPowder Engineering Co., Ltd., situated in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for organic fertilizer granules. The organic fertilizer granule pneumatic conveying line is a critical component in modern fertilizer production, facilitating efficient, dust-free transportation of granular organic fertilizers from storage silos to processing or packaging stages.
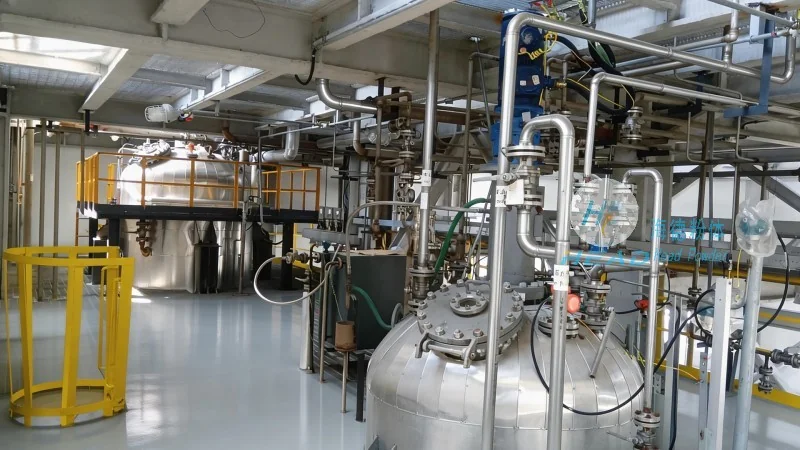
Overview of the Organic Fertilizer Granule Pneumatic Conveying Line
The organic fertilizer granule pneumatic conveying line is engineered to handle bulk organic fertilizer granules with precision and reliability. This system replaces traditional mechanical conveyors, offering advantages such as reduced labor costs, minimized material loss, and enhanced safety in organic fertilizer handling. The system typically comprises several key components: a hopper for material storage, a feeder for controlled discharge, an air compressor to generate compressed air, a pipeline network for material transport, and a control system for operational management.
Working Principle of the Pneumatic Conveying System
The core working principle of the organic fertilizer granule pneumatic conveying line relies on compressed air to transport granular materials through a pipeline. When the feeder releases organic fertilizer granules into the hopper, the air compressor supplies high-pressure air. This air is introduced into the pipeline, creating a flow that lifts and moves the granules. The air and granules are separated at the discharge point, with the air being recycled or safely released. The system may use positive pressure, negative pressure, or a combination, depending on the transport distance and application requirements.
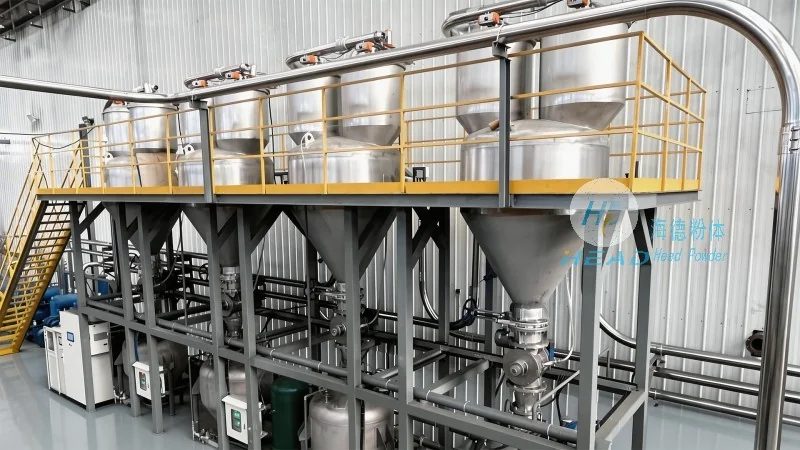
Step-by-Step Operation Process
The operation of the organic fertilizer granule pneumatic conveying line follows a systematic sequence: First, organic fertilizer granules are loaded into the storage hopper. The feeder then meters the granules at a controlled rate into the conveying pipeline. Simultaneously, the air compressor provides compressed air to the system. The air and granules are mixed in the pipeline, and the air pressure propels the granules forward. At the discharge point, the air and granules are separated. The granules are deposited into the next processing stage (e.g., mixer or packaging machine), while the air is filtered and recycled. The control system monitors pressure, flow rate, and material levels to maintain optimal performance and prevent system failures.
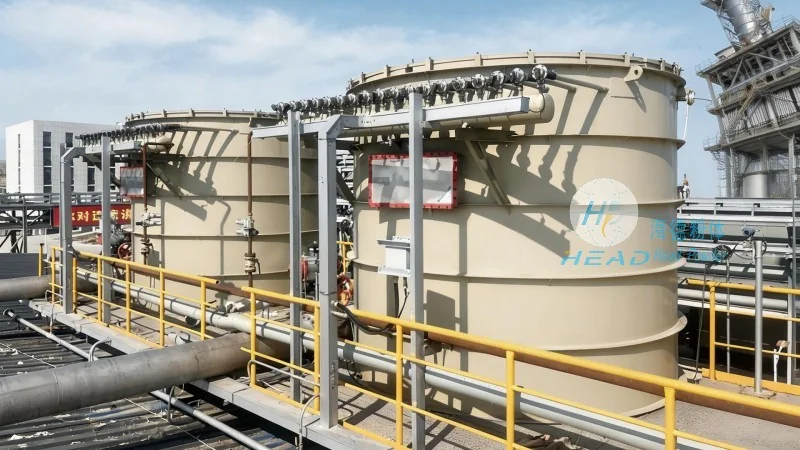
Key Technical Features and Advantages
The organic fertilizer granule pneumatic conveying line from Shandong HeadPowder Engineering Co., Ltd. incorporates technical features that enhance performance and reliability. These include adjustable air pressure and flow control to accommodate varying granule sizes and moisture content, ensuring consistent conveying efficiency. The system features advanced filtration and dust collection systems to minimize environmental impact and maintain air quality. The pipeline network is constructed with corrosion-resistant materials to withstand acidic and moisture-rich conditions of organic fertilizers, extending service life. The automated control system provides real-time monitoring and alarm functions, enabling quick issue resolution and continuous operation.
Application and Benefits in Fertilizer Production
The organic fertilizer granule pneumatic conveying line is widely used in fertilizer production facilities to transport granular organic fertilizers from storage to processing or packaging stages. Key benefits include improved operational efficiency, reduced labor costs, and enhanced safety compared to traditional conveyors. Dust-free operation minimizes health risks and reduces material loss from spillage. The system's flexibility allows easy integration with existing production lines, and its compact design saves floor space. Consistent material flow ensures smooth operation of downstream processes (e.g., mixing, packaging), boosting overall productivity in fertilizer manufacturing.




