For industries dealing with glucose material, efficient and reliable material handling is crucial. Pneumatic conveying equipment offers a solution that combines precision, safety, and adaptability. This article explores the principles, working scenarios, and key characteristics of pneumatic conveying systems specifically designed for glucose material transport, highlighting how such equipment enhances operational efficiency and product integrity.
The Working Principle of Pneumatic Conveying Equipment
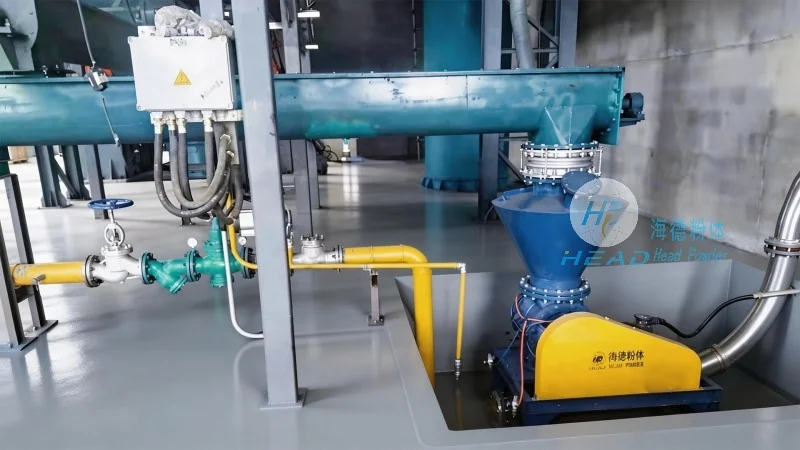
Pneumatic conveying systems operate by using air or gas to transport bulk materials through a pipeline network. In the case of glucose material, the equipment typically employs a positive pressure or negative pressure system. The positive pressure system, also known as a pressure conveyor, generates air pressure within the pipeline to push the material forward. This method is ideal for short to medium-distance transport and is commonly used in glucose processing facilities where materials need to be moved from storage silos to processing lines. The negative pressure system, or vacuum conveyor, creates a vacuum to draw material into the pipeline, which is suitable for applications requiring material to be transported from multiple points to a central collection point. Both systems ensure that glucose particles are conveyed without direct contact with mechanical components, minimizing the risk of contamination and maintaining product quality.
Key Features and Advantages of Glucose Material Pneumatic Conveying
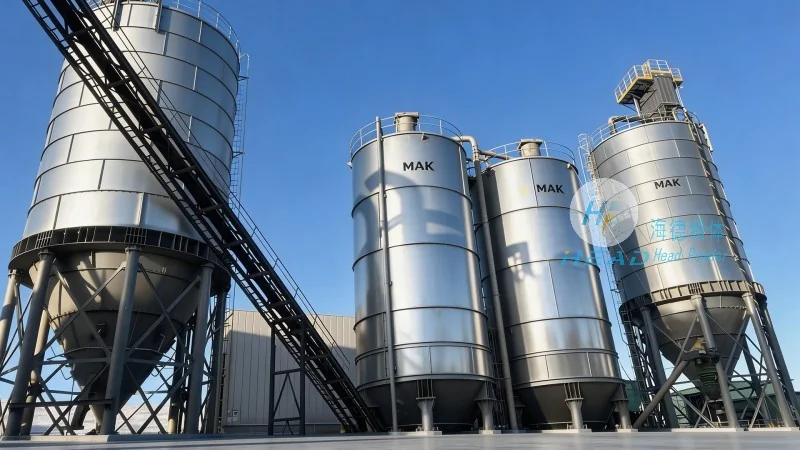
HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying equipment tailored for glucose material. The systems are engineered with several key features that address the unique challenges of handling glucose. For instance, the equipment is designed with smooth, corrosion-resistant internal surfaces to prevent material buildup and ensure easy cleaning, which is essential for maintaining hygiene standards in food processing environments. Additionally, the conveying lines are equipped with adjustable air flow controls, allowing operators to optimize the conveying speed and pressure based on the material's characteristics and the distance of transport. This flexibility ensures that the glucose material is conveyed at the optimal velocity, reducing the risk of particle degradation or clogging. Another significant advantage is the ability to handle varying material densities and flow rates. The systems can accommodate different batch sizes and material types, making them versatile for diverse production needs. Furthermore, the equipment is designed for low maintenance, with components that are easily accessible and replaceable, reducing downtime and operational costs.
Typical Working Scenarios and Applications
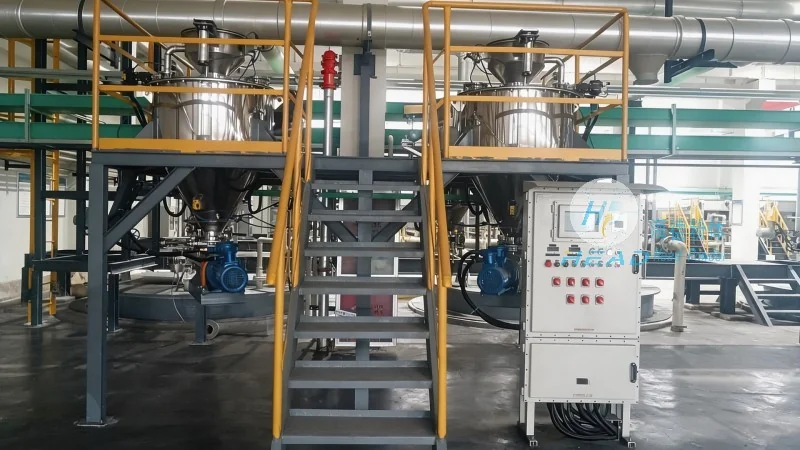
The application of pneumatic conveying equipment for glucose material is widespread across various industrial settings. In glucose processing plants, these systems are commonly used to transport raw glucose from storage silos to mixing and refining units. The equipment efficiently moves the material from the storage area to the production line, ensuring a continuous flow of raw materials. In pharmaceutical and food processing facilities, where product purity is paramount, pneumatic conveying is preferred over mechanical conveyors to avoid cross-contamination. The systems are also utilized in bulk handling operations, such as moving glucose from production lines to packaging areas or storage silos. The versatility of the equipment allows it to be integrated into existing production lines, enhancing overall operational efficiency. Additionally, the equipment is suitable for both indoor and outdoor applications, making it adaptable to different facility layouts and environmental conditions.
Technical Specifications and Customization Options
HeadPowder Engineering Co., Ltd. offers a range of technical specifications to meet the specific requirements of glucose material handling. The pneumatic conveying systems are available in various pipeline configurations, including straight-line, loop, and vertical lift designs, allowing for flexible installation in different facility layouts. The equipment can be customized to handle different material sizes and flow rates, with options for varying air pressure and flow rates. For example, the systems can be equipped with air filters and moisture separators to ensure the air used for conveying is clean and dry, preventing moisture-related issues in the glucose material. Additionally, the equipment can be integrated with sensors and control systems to monitor conveying parameters in real-time, providing operators with data on material flow, pressure, and temperature. This integration enhances process control and allows for immediate adjustments to optimize performance. The company also provides technical support and maintenance services to ensure the equipment operates at peak efficiency throughout its lifespan.
Company Profile and Service Commitment
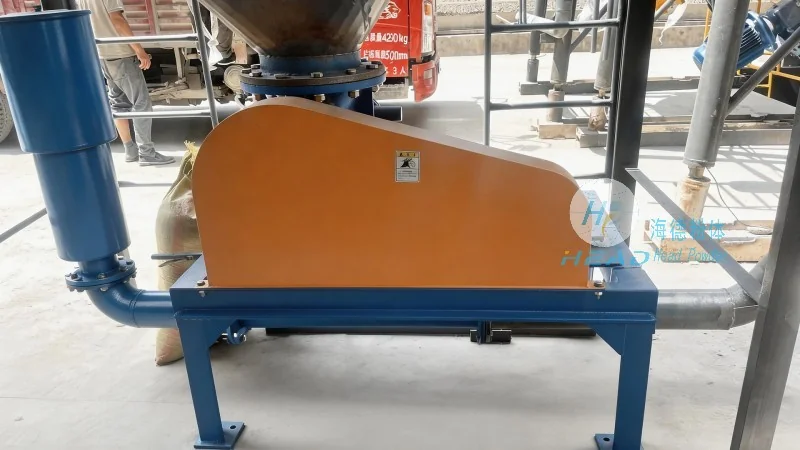
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying equipment based in Shandong, China. With years of experience in the industry, the company specializes in designing and manufacturing high-quality systems tailored for diverse material handling needs. HeadPowder's commitment to quality and innovation has made it a trusted partner for industries dealing with glucose and other bulk materials. The company's team of engineers and technicians work closely with clients to understand their specific requirements and provide customized solutions that enhance operational efficiency and product quality. HeadPowder's products are designed to meet international standards and are backed by a comprehensive warranty and after-sales service. The company's focus on customer satisfaction and technical excellence ensures that clients receive reliable and efficient equipment that meets their production needs. By choosing HeadPowder, industries can benefit from advanced technology, expert support, and cost-effective solutions for their material handling challenges.




