HeadPowder, a leading provider in the field of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed for efficient transport of sintered fly ash powder. This article explores the fundamental principles behind such equipment and highlights key operational scenarios where these systems excel in performance and reliability.
Understanding the Core Principles of Sintered Fly Ash Powder Pneumatic Conveying
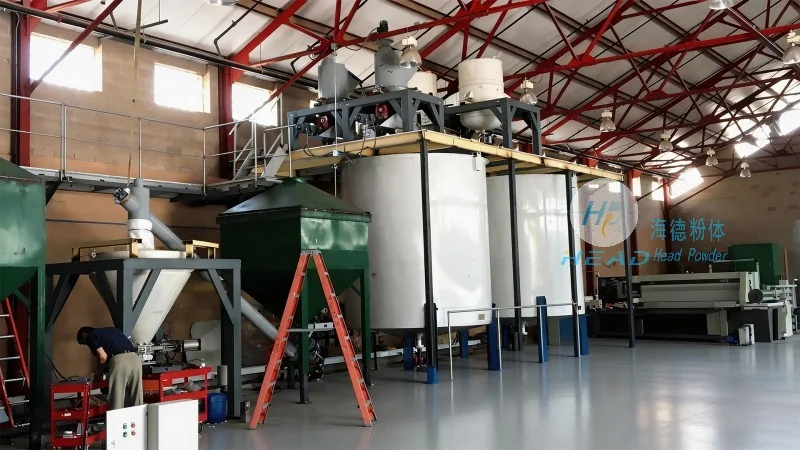
The pneumatic conveying machine for sintered fly ash powder operates on the principle of using compressed air to transport particulate materials through a pipeline system. Unlike traditional mechanical conveyors, this method eliminates the need for moving parts in contact with the material, reducing wear and maintenance requirements. The system typically consists of a hopper to store the fly ash, a blower or compressor to generate the necessary air pressure, and a pipeline network that directs the material from the source to the destination. The air flow creates a negative pressure or positive pressure environment, depending on the design, to draw or push the powder through the system. Key components include the material feed mechanism, which ensures a consistent flow of powder into the air stream, and the separation unit at the discharge end to remove air from the conveyed material, preventing dust emissions and ensuring product purity.
Key Working Scene Characteristics and Applications
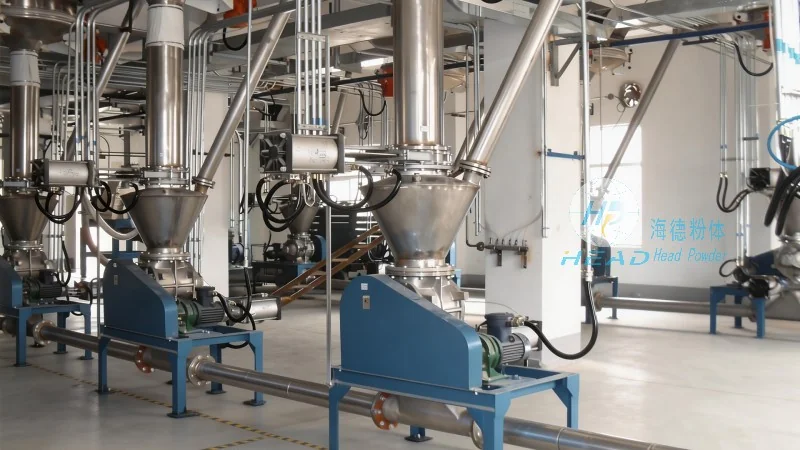
HeadPowder's sintered fly ash powder pneumatic conveying machines are particularly suited for industrial environments where handling fine powders requires high efficiency and minimal contamination. Common operational scenarios include applications in cement production, where sintered fly ash is used as a supplementary cementitious material, and in power generation facilities, where the material is transported from storage silos to processing units. The systems are also utilized in construction material manufacturing plants, where the precise control of powder flow is critical for maintaining product quality. In these scenarios, the equipment's ability to handle abrasive materials like sintered fly ash without significant wear on components is a major advantage. Additionally, the compact design of the conveying lines allows for integration into existing plant layouts, minimizing space requirements and installation costs. The systems are engineered to handle varying particle sizes and moisture content, ensuring consistent performance even under fluctuating operational conditions.
Advantages and Performance Metrics in Real-World Operations
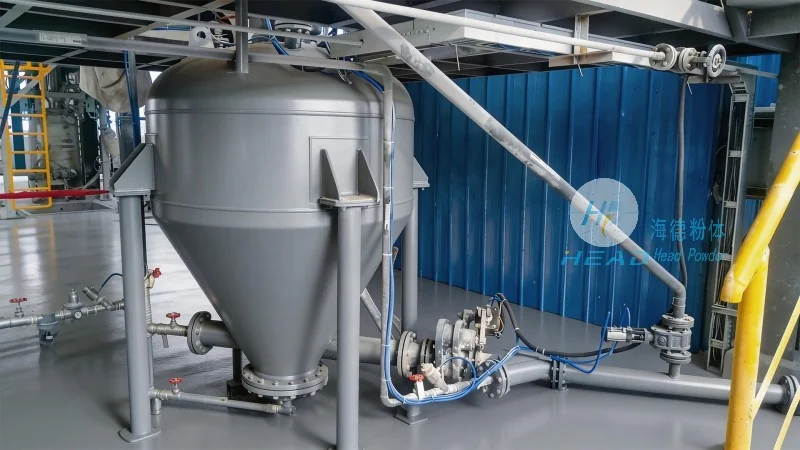
When deployed in real-world industrial settings, HeadPowder's sintered fly ash powder pneumatic conveying machines demonstrate several key advantages. The primary benefit is the reduction in labor costs associated with manual handling of bulk powders, as the automated system can operate continuously with minimal supervision. Additionally, the enclosed pipeline system significantly reduces dust emissions, improving workplace safety and compliance with environmental regulations. The equipment's efficiency in material transport is quantified by its ability to maintain high conveying rates while minimizing energy consumption. For example, in cement plants, the system can achieve conveying capacities of up to several hundred tons per hour with energy consumption that is substantially lower than that of traditional belt conveyors. The reliability of the system is further enhanced by its modular design, which allows for easy maintenance and replacement of components without disrupting the entire operation. This modular approach ensures that downtime is minimized, and the system can quickly resume operation after maintenance activities.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to delivering innovative and reliable pneumatic conveying solutions tailored to the specific needs of industrial clients. The company's expertise in designing and manufacturing sintered fly ash powder pneumatic conveying machines reflects its dedication to improving material handling efficiency and sustainability in various industrial sectors. By combining advanced engineering principles with practical application knowledge, HeadPowder continues to provide high-performance equipment that meets the evolving demands of modern industrial operations. The company's presence in Shandong, China, underscores its strategic position in the global market for industrial material handling solutions, ensuring that clients can access cutting-edge technology and responsive support for their material transport needs.




