The intelligent tonne bag loading station is a specialized system engineered for efficient handling of bulk powder materials. It integrates advanced pneumatic conveying technology with automated material transfer capabilities, designed to seamlessly move powders from large tonne bags into processing lines, storage silos, or other destinations with precision and reliability. The core of this system relies on the pneumatic conveying mechanism, which utilizes compressed air to create a controlled flow that transports powder particles through pipelines, ensuring a smooth and consistent transfer process. This equipment is particularly valuable in industries where bulk powder handling is critical, such as chemical, pharmaceutical, food, and mining sectors.
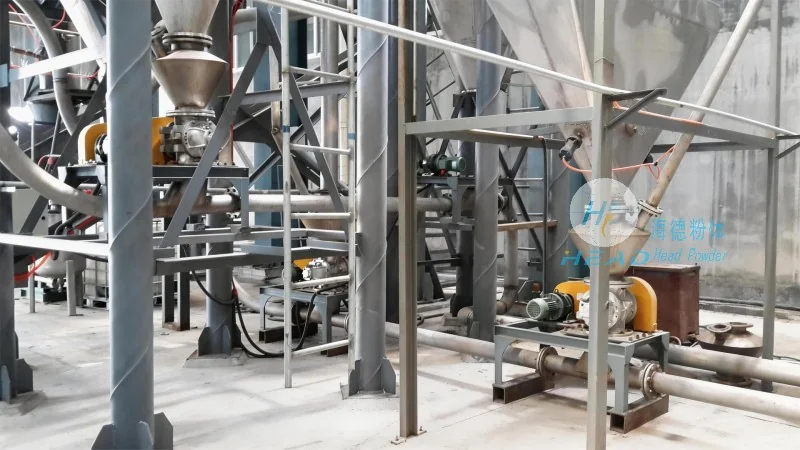
Principle of Pneumatic Conveying in the Loading Station
The pneumatic conveying principle employed in the intelligent tonne bag loading station is based on the movement of powder particles within a gas stream. In operation, compressed air is introduced into the tonne bag, establishing a pressure differential that draws the powder into the conveying pipeline. The air flow then propels the powder through the system, maintaining a stable velocity and pressure to prevent particle segregation or blockages. The design incorporates airlocks, cyclones, and filters to ensure efficient separation of the powder from the air, preserving product purity and system efficiency. The station's control system continuously monitors and adjusts air pressure, flow rate, and other parameters in real-time, optimizing the conveying process for different powder types and bag sizes. This dynamic control ensures consistent performance and minimizes downtime.
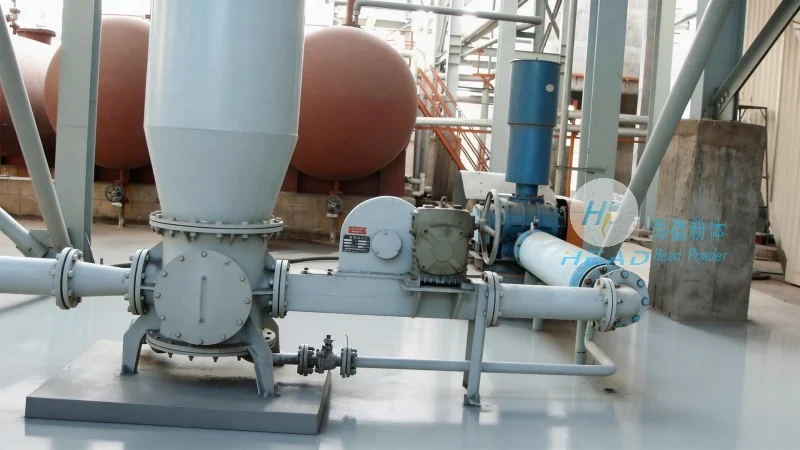
Working Scene Characteristics of the Loading Station
The intelligent tonne bag loading station is tailored for diverse industrial applications where bulk powder handling demands precision and safety. Its compact and modular design facilitates easy integration into existing production lines, enabling manufacturers to enhance operational efficiency and reduce manual labor. The system is particularly suitable for industries dealing with fine or abrasive powders, where manual handling poses risks and inefficiencies. The station's automation capabilities minimize human error and improve safety, as it eliminates direct contact with the powder and reduces the need for heavy lifting. Additionally, the system's adaptability allows it to handle various bag sizes and powder characteristics, making it a versatile solution for different facility layouts and space constraints.
Key Features and Benefits
HeadPowder, a leading manufacturer of material handling solutions, has developed this intelligent tonne bag loading station with a focus on user-friendly operation and high performance. The system features advanced sensors and control panels that provide real-time monitoring of the conveying process, allowing operators to quickly identify and address any issues. The pneumatic conveying technology ensures minimal product degradation, preserving the quality of sensitive powders like pharmaceuticals or food ingredients. The station is constructed with durable materials, such as stainless steel, to withstand corrosive effects from various powders and maintain hygiene standards. Furthermore, the system's energy-efficient design reduces operational costs while minimizing environmental impact. The modular design allows for scalability, enabling users to expand the system as their production needs grow.
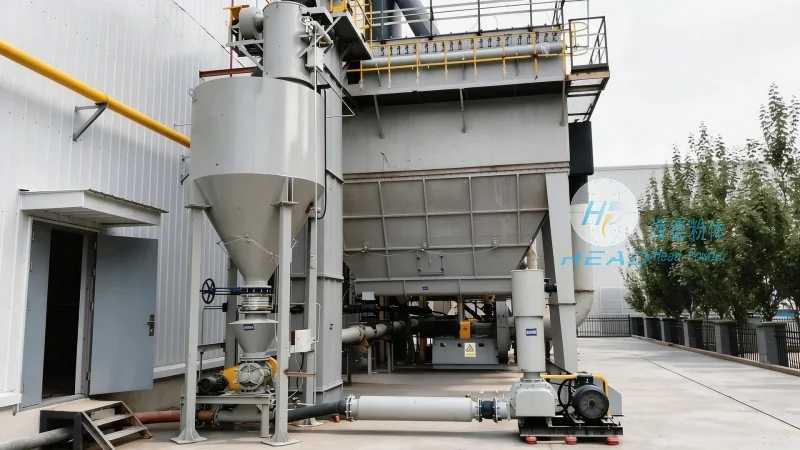
Application Examples and Operational Scenarios
The intelligent tonne bag loading station is widely used in scenarios where large quantities of powder need to be transferred efficiently. For instance, in a chemical plant, the system can handle raw materials like calcium carbonate or sodium bicarbonate, feeding them directly into reactors or storage tanks. In a pharmaceutical facility, the station ensures the safe and hygienic transfer of active pharmaceutical ingredients (APIs), maintaining compliance with regulatory standards. The system is also suitable for food processing plants, where it can handle powders like flour, sugar, or protein supplements, ensuring product integrity and preventing contamination. In mining operations, the station can transfer ore powders from bulk bags to processing equipment, improving the overall efficiency of the extraction and processing chain. Each application benefits from the station's ability to handle different powder characteristics, such as particle size, density, and moisture content, making it a reliable solution for diverse industrial needs.




