HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and implementation of efficient systems for transporting quartz sand powder. With a strong presence in Shandong, China, the company has established itself as a trusted provider of advanced material handling technologies tailored to the unique requirements of various industrial applications.
Understanding the Core Principles of Quartz Sand Powder Material Handling Systems
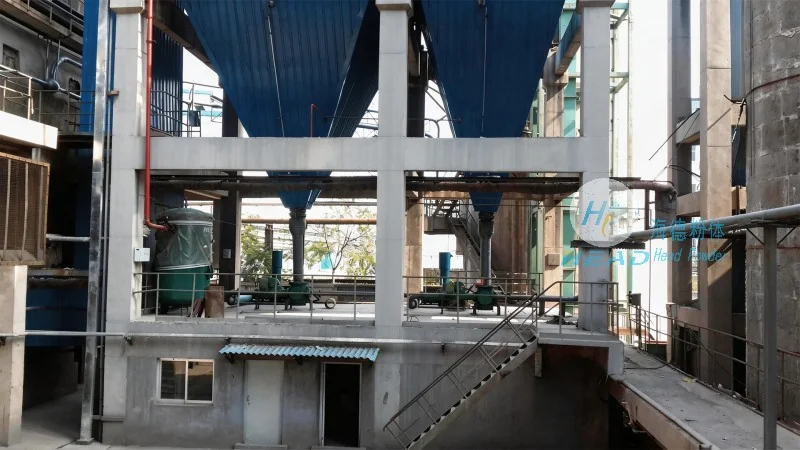
The fundamental principle behind quartz sand powder material handling systems lies in the efficient and reliable transport of fine particulate materials like quartz sand. These systems are engineered to handle the specific challenges associated with quartz sand, such as its abrasive nature, dust generation, and the need for precise control over particle flow. The core components typically include feeders, conveyors, and control mechanisms that work in tandem to ensure smooth and continuous material movement. The design emphasizes minimizing material degradation, preventing equipment wear, and maintaining consistent flow rates, which are critical for maintaining product quality and operational efficiency.
Key Working Scene Characteristics of Quartz Sand Powder Handling Systems
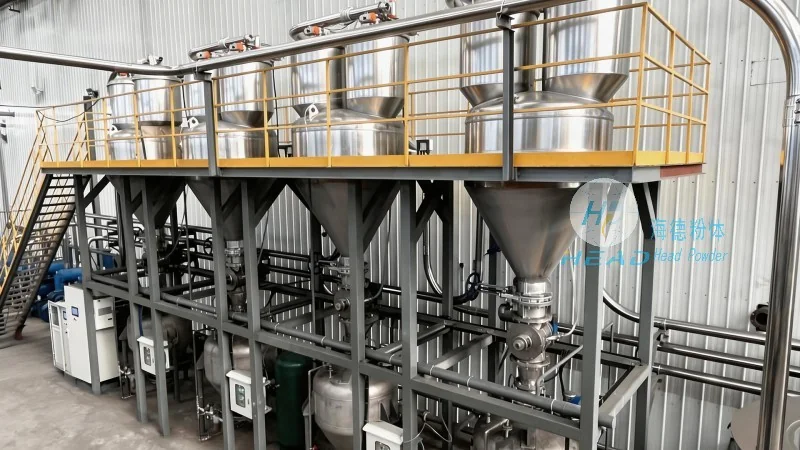
Quartz sand powder material handling systems are deployed in diverse industrial settings, each presenting unique operational characteristics that influence system design and performance. In mining and quarrying operations, these systems are used to transport raw quartz sand from extraction sites to processing facilities, where the material is further refined. The systems must be robust enough to handle large volumes of material and withstand the harsh environmental conditions of mining sites. In construction and manufacturing industries, quartz sand is used as a raw material for concrete, glass, and other products, requiring precise dosing and mixing. The handling systems in these sectors need to integrate seamlessly with existing production lines, ensuring accurate material delivery and minimizing downtime. Additionally, in environmental and recycling applications, quartz sand is processed and reused, necessitating systems that can handle contaminated or mixed materials while maintaining cleanliness and compliance with regulatory standards.
Advanced Features and Applications in Quartz Sand Powder Material Handling
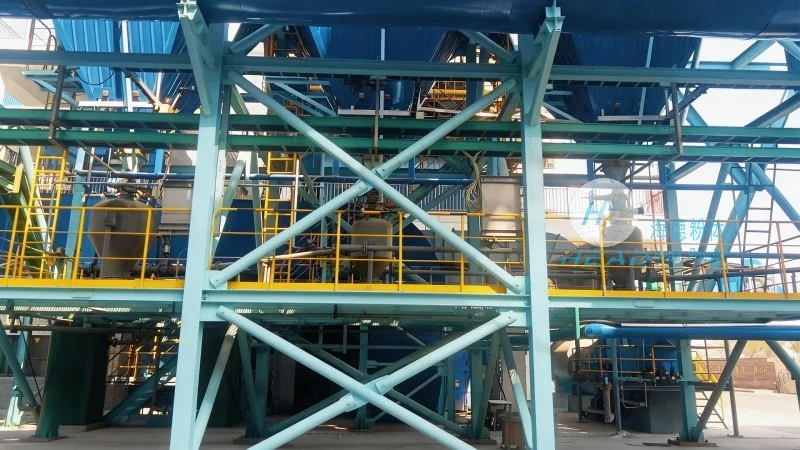
Modern quartz sand powder material handling systems incorporate advanced technologies to enhance performance and adaptability. For instance, automated control systems use sensors and feedback mechanisms to adjust conveyor speeds and feed rates in real-time, optimizing material flow based on demand. Dust suppression and filtration systems are integrated to mitigate environmental impact and ensure workplace safety, which is particularly important given the fine nature of quartz sand. The use of specialized materials in conveyor components, such as wear-resistant belts and liners, extends equipment lifespan and reduces maintenance costs. Moreover, modular design allows for flexible system configurations, enabling companies to scale operations or adapt to changing production needs without significant capital investment. These features collectively contribute to the efficiency and reliability of quartz sand powder handling systems, making them indispensable in industries where consistent material supply and quality control are paramount.




