High-pressure dilute phase powder conveying equipment is a specialized system designed for the efficient and reliable transport of bulk powders over long distances. This technology is fundamental to industries that require the movement of materials such as cement, coal, flour, and other fine particulate substances. The core principle behind this equipment lies in the use of high-pressure air to create a dilute phase flow, where the powder particles are suspended in the air stream, allowing for smooth and continuous transportation. By leveraging this principle, the system ensures minimal material degradation, reduced blockage risks, and enhanced operational efficiency compared to traditional conveying methods.
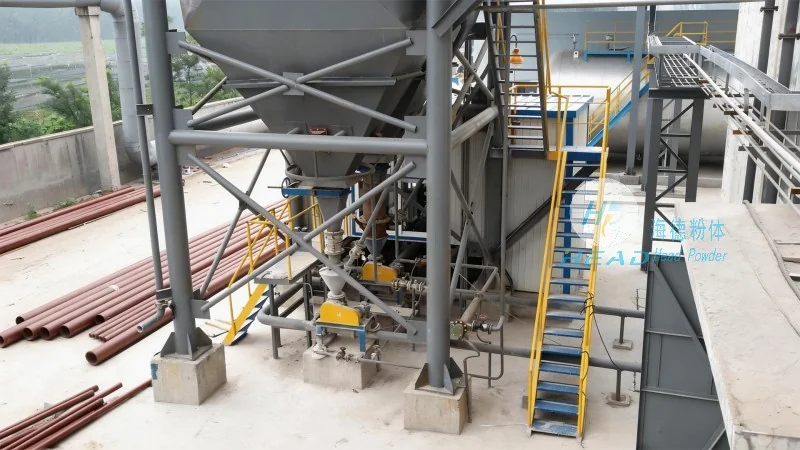
Key Working Scene Characteristics
One of the primary advantages of high-pressure dilute phase powder conveying systems is their adaptability to diverse operational environments. These systems are commonly employed in industrial settings where large volumes of powders need to be moved between processing units, storage silos, and production lines. The equipment is particularly suitable for applications requiring high throughput and long-distance transport, such as in cement plants, coal-fired power stations, and food processing facilities. The design allows for flexible integration into existing production workflows, enabling seamless material transfer without the need for extensive infrastructure modifications. Additionally, the system's ability to handle a wide range of powder types, from fine to coarse particles, makes it a versatile solution for various industrial needs.
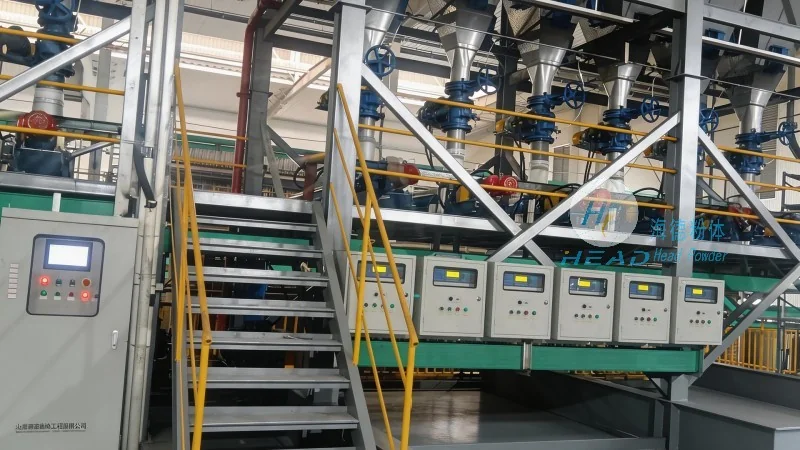
Working Principle of High-Pressure Dilute Phase Conveying
The operation of high-pressure dilute phase powder conveying equipment is based on the principle of pneumatic conveying, where compressed air is used to create a flow that suspends the powder particles. The system typically consists of a compressor, a hopper for material storage, a conveying line, and a receiver for the discharged material. The process begins with the material being fed into the hopper, where it is then drawn into the conveying line by the high-pressure air. As the air flows through the line, it lifts and transports the powder particles in a dilute phase, preventing agglomeration and ensuring consistent flow. The pressure and velocity of the air are carefully controlled to maintain optimal particle suspension and prevent material deposition or blockage in the pipeline. This controlled environment allows for efficient and reliable transport, even over distances of several kilometers.
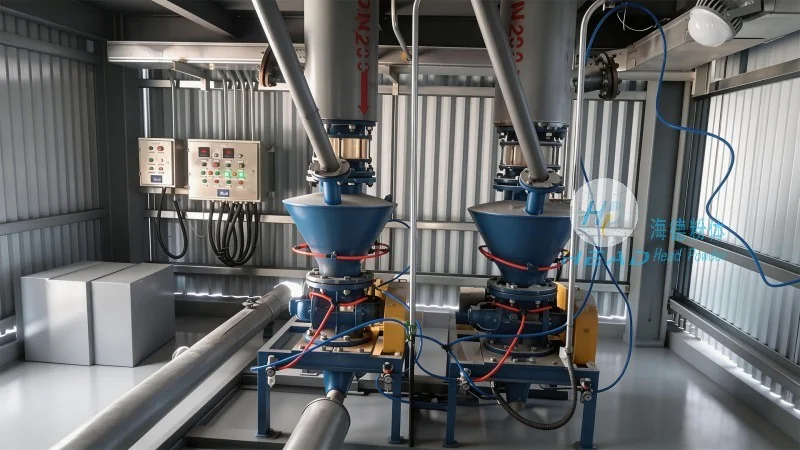
Typical Application Scenarios
High-pressure dilute phase powder conveying equipment is widely used in various industrial applications. For instance, in cement manufacturing, it is used to transport raw materials like limestone and clay from storage silos to the grinding mills. In coal-fired power plants, the system efficiently conveys coal from stockpiles to the boiler feed system, ensuring a steady supply of fuel. Similarly, in the food industry, it is employed to transport flour, sugar, and other fine powders from processing units to packaging lines. The equipment's ability to handle different powder characteristics, such as moisture content and particle size, makes it suitable for a broad range of applications. Furthermore, the system's compact design and low maintenance requirements make it an attractive option for industries seeking cost-effective and reliable material handling solutions.
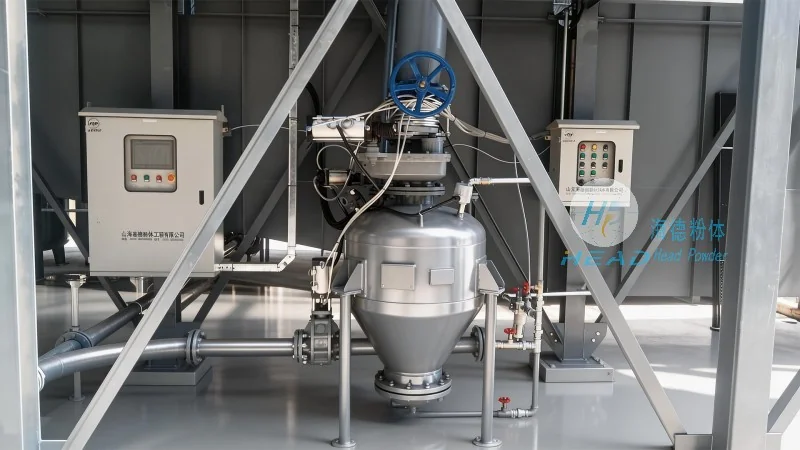
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of high-pressure dilute phase powder conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial material handling sector. Headpowder's products are designed to meet the specific needs of various industries, ensuring optimal performance and reliability. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. By adhering to stringent quality standards and providing comprehensive technical support, headpowder aims to deliver solutions that enhance operational efficiency and reduce costs for its clients. The company's commitment to customer satisfaction and continuous improvement has made it a preferred choice for businesses seeking reliable and efficient powder conveying systems.




