HeadPowder, a leading enterprise in the field of powder conveying technology, specializes in the design, manufacturing, and application of advanced stone powder conveying systems. The company is headquartered in Shandong, China, and has established itself as a trusted provider of efficient and reliable solutions for material handling in various industrial sectors.
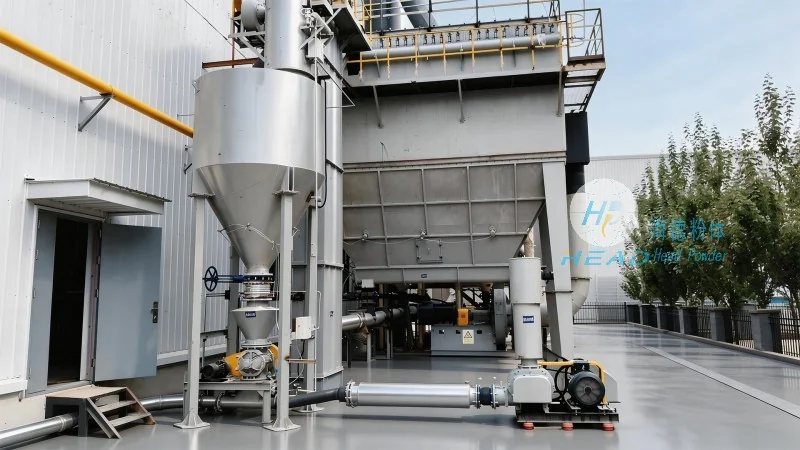
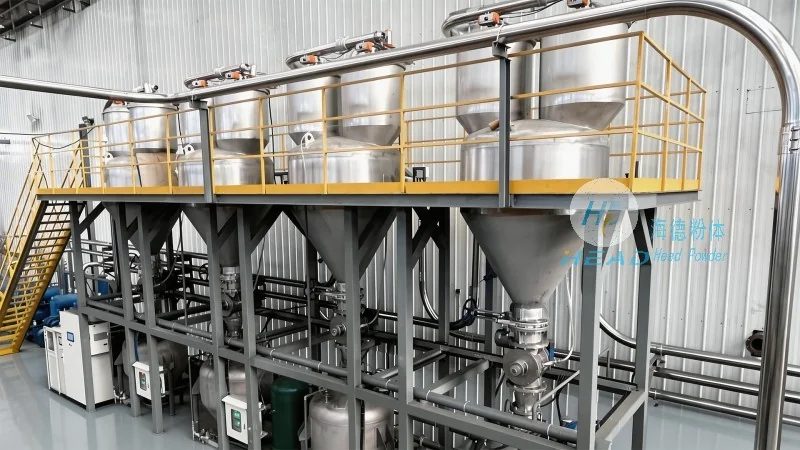
Principle of Stone Powder Conveying Systems
Stone powder conveying systems operate on the fundamental principle of utilizing mechanical or pneumatic forces to transport granular materials, such as crushed stone powders, from one location to another. The core components typically include a feeding mechanism, a conveying pipeline, a drive system, and a control unit. The feeding mechanism ensures a consistent and controlled flow of the stone powder into the system, while the conveying pipeline, often made of durable materials like stainless steel or special polymers, transports the material under pressure or vacuum. The drive system, which may consist of motors and pumps, provides the necessary power to move the material through the pipeline. Advanced systems may incorporate sensors and control algorithms to optimize the conveying process, ensuring minimal material loss and energy efficiency.
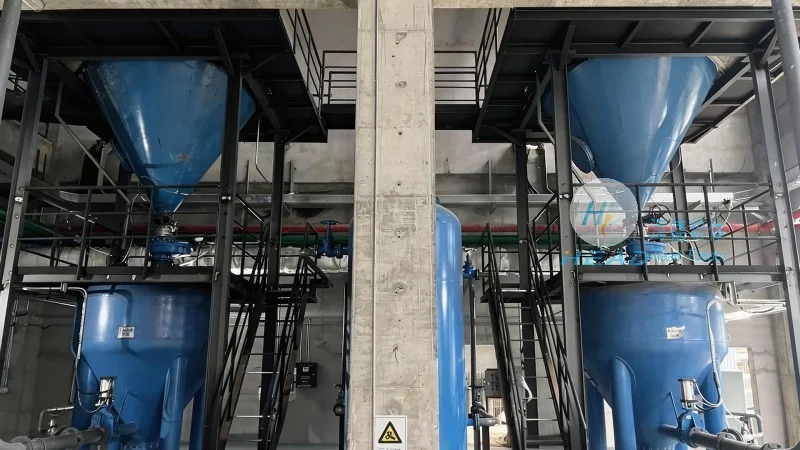
Working Scene Characteristics of Stone Powder Conveying Systems
The application of stone powder conveying systems is characterized by their adaptability to diverse industrial environments and operational requirements. In construction sites, these systems are widely used for transporting crushed stone powders from storage silos to mixing stations, ensuring a steady supply of raw materials for concrete production. The systems are designed to handle high volumes of material with minimal downtime, which is crucial for maintaining project timelines. In mining operations, stone powder conveying systems facilitate the transport of processed materials from processing plants to storage facilities, reducing the need for manual handling and enhancing safety. Additionally, in environmental remediation projects, these systems are employed to convey stone powders used in soil stabilization or erosion control, contributing to sustainable land management practices. The versatility of stone powder conveying systems allows them to integrate seamlessly with existing industrial workflows, improving overall operational efficiency and reducing labor costs.
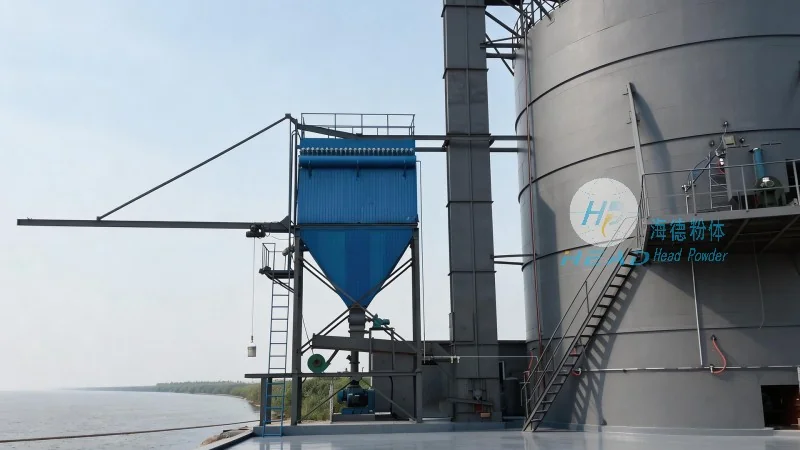
Technical Advantages and Operational Efficiency
Modern stone powder conveying systems are engineered to deliver superior performance through several key technological advancements. One of the primary advantages is the reduction of material degradation during transport, as the systems use gentle handling methods that minimize particle breakage and dust generation. This is particularly important for stone powders, which are often sensitive to impact and abrasion. Additionally, the systems are designed for energy efficiency, utilizing variable speed drives and optimized airflow to reduce power consumption while maintaining consistent material flow rates. The integration of real-time monitoring and control systems allows operators to adjust the conveying parameters dynamically, responding to changes in material volume or pipeline conditions. This adaptability ensures that the system operates at peak efficiency under varying operational loads, further enhancing its cost-effectiveness and reliability.




