Ammonium sulfate, a widely used chemical fertilizer, requires efficient and reliable transportation systems to ensure smooth supply chain operations. Pneumatic conveying equipment has emerged as a critical solution for handling this material, offering advantages such as dust control, reduced labor costs, and enhanced safety. This article explores the fundamental principles of pneumatic conveying systems designed for ammonium sulfate, along with key working scene characteristics that make them suitable for various industrial applications.
Principle of Pneumatic Conveying for Ammonium Sulfate
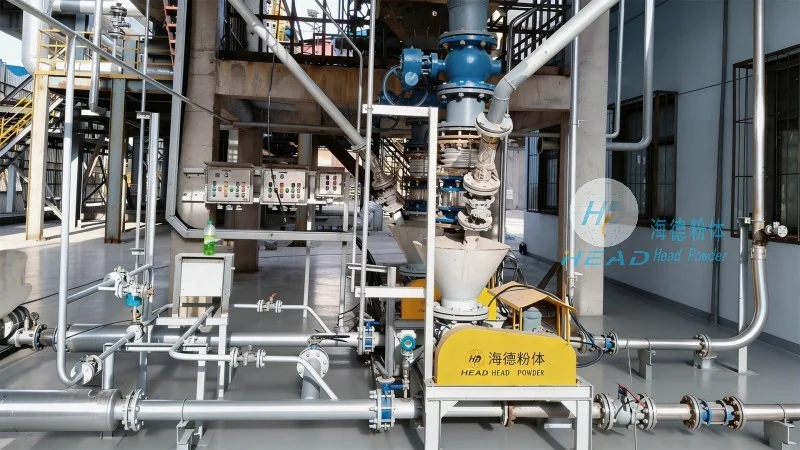
The core principle of pneumatic conveying involves transporting bulk materials like ammonium sulfate through a pipeline using a gas stream, typically air or a combination of air and other gases. The system operates by creating a pressure differential that propels the material forward. There are two main types of pneumatic conveying: dilute-phase and dense-phase. Dilute-phase systems use high-velocity air to suspend the material particles, while dense-phase systems employ lower velocities and higher pressure to move the material in a more compact form. For ammonium sulfate, the choice of system depends on factors like material characteristics, distance, and required flow rate. The equipment typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver to collect the material at the destination. The air supply is managed by a blower or compressor, which generates the necessary pressure and flow to move the material efficiently. Key components such as cyclones, filters, and silencers are also integral to the system, ensuring effective separation of material from air and minimizing noise pollution. The design of the conveying line, including pipe diameter, length, and bends, is crucial for maintaining consistent flow and preventing blockages. Proper maintenance of these components is essential to ensure the system operates at optimal efficiency and longevity.
Working Scene Characteristics of Ammonium Sulfate Pneumatic Conveying Equipment
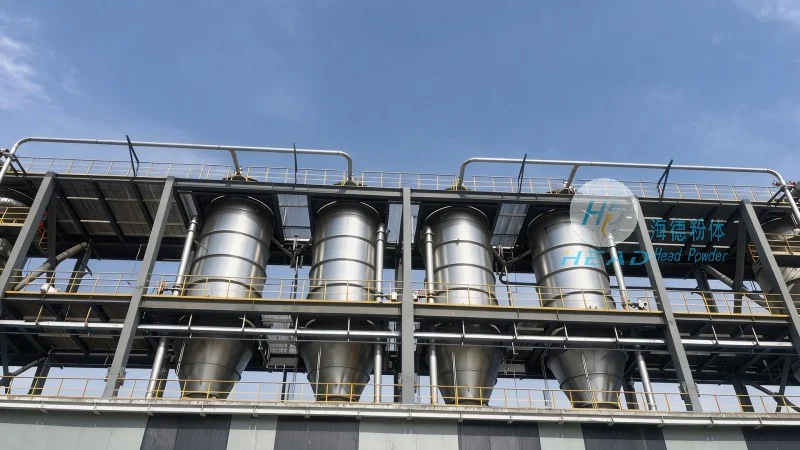
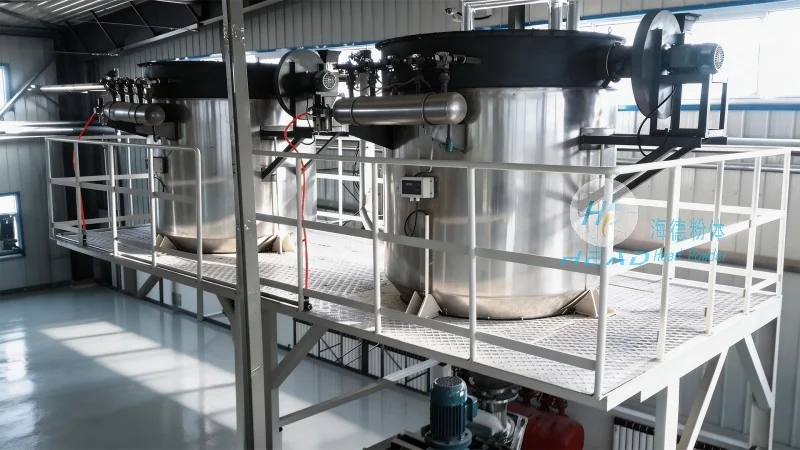
The working scene characteristics of pneumatic conveying systems for ammonium sulfate are tailored to meet the specific demands of industrial environments. These systems are commonly used in fertilizer production facilities, where they facilitate the transfer of ammonium sulfate from storage silos to processing units or packaging areas. The equipment is designed to handle the bulk nature of the material, which can be abrasive and prone to dust generation. Dust control is a critical aspect, as ammonium sulfate is a fine powder that can cause respiratory issues and environmental contamination if not properly managed. The conveying systems incorporate advanced filtration and dust collection mechanisms, such as cyclone separators and bag filters, to ensure compliance with environmental regulations and workplace safety standards. The working environment may involve high temperatures or humidity, which can affect the material's properties and the equipment's performance. Therefore, the equipment is constructed from materials resistant to corrosion and wear, such as stainless steel or special alloys, to withstand the harsh conditions. The system's scalability is another important characteristic, as it can be adjusted to handle varying production volumes. This flexibility allows manufacturers to adapt to changing demand, making the equipment suitable for both small-scale and large-scale operations. Additionally, the equipment is designed for easy integration with existing production lines, minimizing downtime during installation and operation. The working scene may also involve multiple stages of conveying, such as from a storage silo to a mixer, and then to a packaging machine. The equipment's ability to handle these sequential transfers without material loss or degradation is a key advantage. Overall, the working scene characteristics highlight the versatility and reliability of pneumatic conveying systems in handling ammonium sulfate, making them an essential component of modern fertilizer production and distribution.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized pneumatic conveying equipment for bulk materials, including ammonium sulfate. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the chemical and fertilizer industries. HeadPowder's expertise lies in designing and manufacturing customized conveying systems that meet the unique requirements of each client. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled engineering teams to develop cutting-edge solutions. The company's products are known for their durability, efficiency, and compliance with international standards. HeadPowder provides comprehensive services, including design, manufacturing, installation, and after-sales support, ensuring that clients receive end-to-end solutions tailored to their specific needs. The company's focus on customer satisfaction and technical excellence has earned it a reputation for reliability and performance in the industry. With a global presence and a commitment to sustainability, HeadPowder continues to advance the technology of pneumatic conveying, contributing to the efficient and safe handling of bulk materials like ammonium sulfate.




