Efficient and hygienic material handling is crucial in the food processing industry, particularly for products like cereals. The cereal pneumatic conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a reliable solution for transporting bulk materials with precision and minimal risk of contamination. This article explores the working principle and key features of such systems, highlighting their advantages in modern food production.
Working Principle of Cereal Pneumatic Conveying Systems
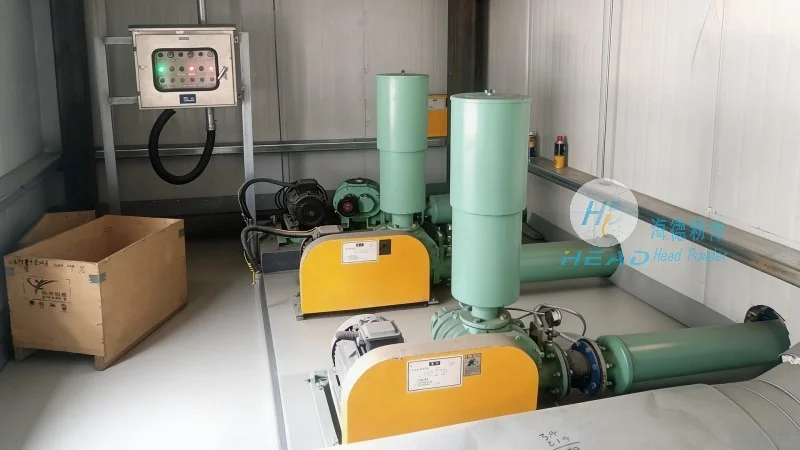
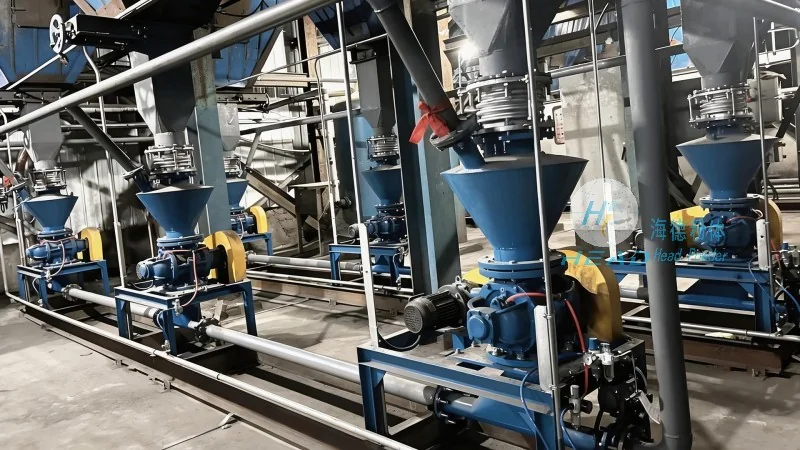
The core of a cereal pneumatic conveying system lies in its ability to transport dry bulk materials, such as cereals, using air as the conveying medium. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems, also known as pressure or pressure-assisted systems, use a blower or compressor to generate air pressure that pushes the material through the pipeline. The material is typically fed into the system via a hopper or rotary valve, where it is mixed with air and propelled forward. Negative pressure systems, or vacuum systems, create a vacuum in the pipeline, drawing the material from the source and pulling it through the system. Both systems rely on the interaction between the material and air to achieve efficient transport. The system components include a feeding device (like a rotary valve or star feeder), a conveying pipeline, a separation unit (cyclone or filter), and a dust collector. The feeding device ensures a consistent flow of material into the system, while the pipeline transports it to the destination. The separation unit separates the material from the air, allowing the material to be discharged and the air to be filtered and recirculated or discharged.
Key Features and Advantages of Cereal Pneumatic Conveying Equipment
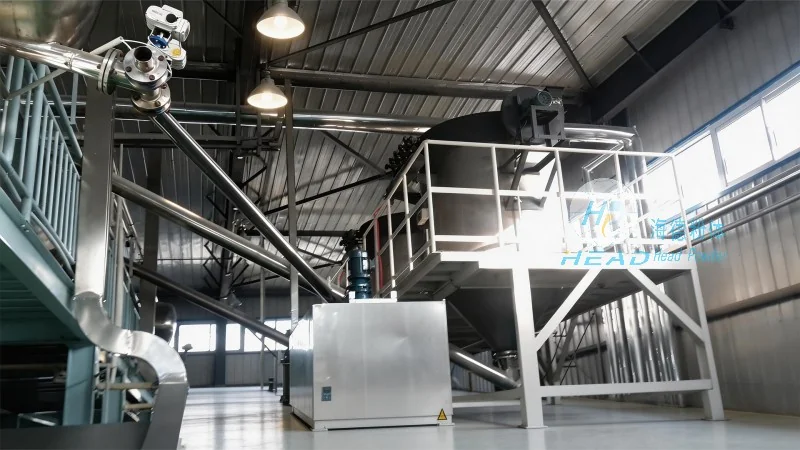
Shandong HeadPowder Engineering Co., Ltd.'s cereal pneumatic conveying systems are designed with several key features that enhance performance and reliability. One of the most significant advantages is the hygienic design, which is critical for food-grade applications. The equipment is constructed from stainless steel and other food-safe materials, ensuring that it meets strict sanitary standards. This design minimizes the risk of contamination and makes cleaning and maintenance straightforward. Another key feature is the high efficiency in material transport. The systems can handle large volumes of cereals with minimal energy consumption, making them cost-effective for industrial use. The low material degradation is another important characteristic. Unlike mechanical conveying methods, which can cause abrasion or breakage, pneumatic systems gently transport the material, preserving its quality and texture. Additionally, the systems offer flexibility in layout, as the conveying pipeline can be arranged in various configurations to suit different production environments. This adaptability allows for seamless integration into existing production lines. The control systems are also advanced, with features like real-time monitoring and automatic adjustments, ensuring optimal operation and reducing downtime. The durability of the equipment is another advantage, with robust components that can withstand continuous operation in demanding industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
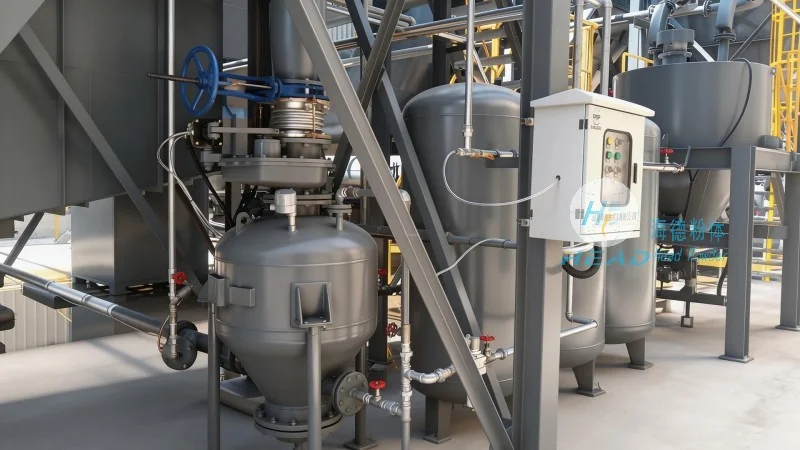
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of pneumatic conveying systems and related equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the food processing industry. HeadPowder's expertise lies in designing and manufacturing systems that meet the specific needs of clients, ensuring that their products are delivered efficiently and safely. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled workforce to produce high-performance equipment. By adhering to international standards and continuously improving its products, HeadPowder aims to provide reliable solutions for material handling challenges in the food sector.




