

Working Principle and Characteristics of Positive Pressure Dilute Phase Pneumatic Conveying Systems
Positive pressure dilute phase pneumatic conveying systems represent a sophisticated method for transporting bulk materials through a pipeline using compressed air. This technology is widely adopted in various industrial sectors due to its efficiency, flexibility, and ability to handle a wide range of materials. Understanding the working principle and key characteristics of such systems is essential for optimizing material handling processes and ensuring operational reliability.
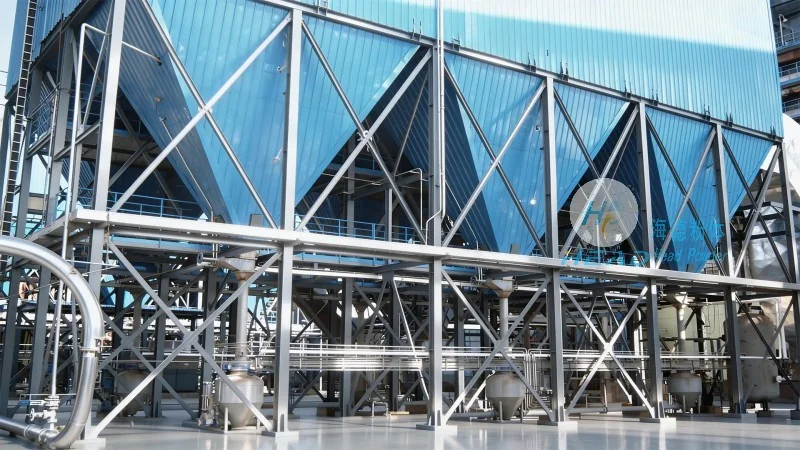
Overview of Positive Pressure Dilute Phase Pneumatic Conveying
At its core, a positive pressure dilute phase pneumatic conveying system operates by injecting compressed air into a material stream, creating a mixture of particles suspended in the air. The system typically consists of a material hopper, a feeder, a pipeline, and a receiver. The compressed air, often supplied by a blower or compressor, is introduced at the inlet of the pipeline, where it mixes with the material being conveyed. This mixture travels through the pipeline under positive pressure, ensuring that the material is continuously transported without the need for additional mechanical components like conveyors or elevators.
Working Principle of Positive Pressure Dilute Phase Pneumatic Conveying
The working principle of a positive pressure dilute phase system involves several critical steps. First, the material is fed from a hopper into a feeder, which controls the flow rate of the material. The feeder then introduces the material into the pipeline where compressed air is already present. The air and material mixture is then accelerated through the pipeline by the pressure differential between the inlet and the outlet. The positive pressure maintained throughout the system prevents air leakage and ensures that the material is carried efficiently to the receiver. The receiver, typically a hopper or a storage tank, collects the material as the air is either vented or recirculated back to the system.
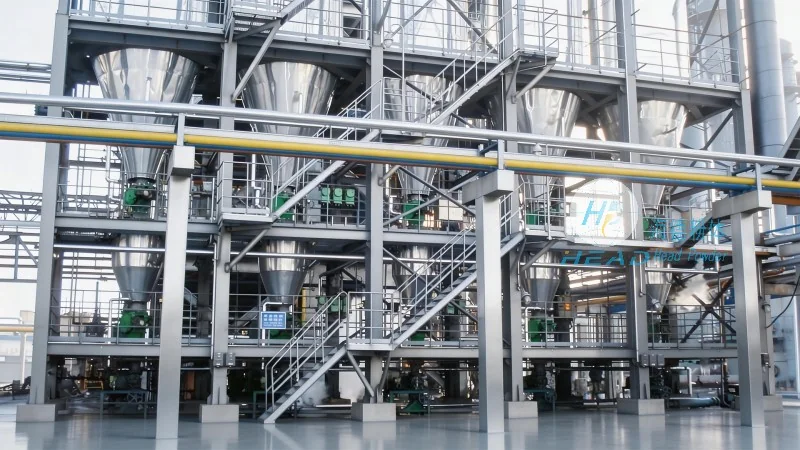
Key Characteristics of Positive Pressure Dilute Phase Pneumatic Conveying Systems
Several distinct characteristics define positive pressure dilute phase pneumatic conveying systems, making them suitable for diverse applications. One of the primary advantages is the ability to handle a wide variety of materials, including powders, granules, and even fine particles, without causing degradation or contamination. The system's flexibility allows for changes in material type or flow rate with minimal adjustments. Additionally, the positive pressure design ensures that the material is conveyed continuously and uniformly, reducing the risk of blockages or uneven flow. Another key characteristic is the system's compactness and space efficiency, as it eliminates the need for large mechanical components and can be installed in confined spaces. The system also offers good control over material transport, with the ability to adjust air pressure and flow rate to optimize performance. Furthermore, positive pressure systems are generally more energy-efficient compared to other conveying methods, as they use compressed air to move materials directly without intermediate steps.
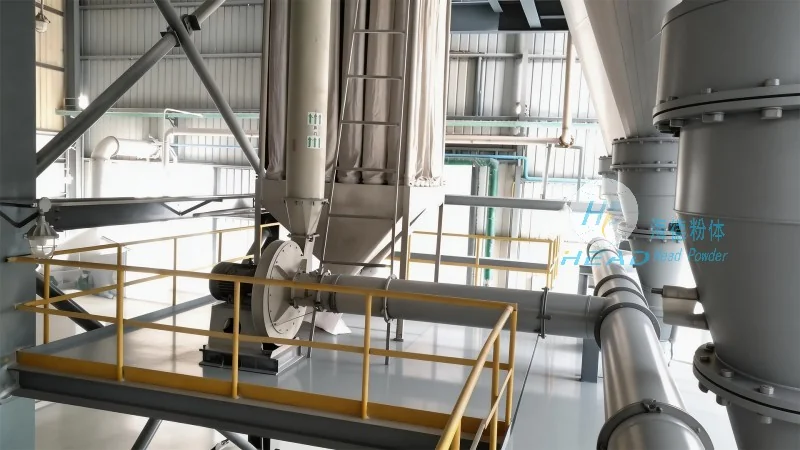
Applications and Benefits in Industrial Settings
Positive pressure dilute phase pneumatic conveying systems are widely used in industries such as food processing, pharmaceuticals, chemicals, and minerals. In food processing, for example, these systems are used to transport powders like flour, sugar, and spices, ensuring hygiene and preventing contamination. In the pharmaceutical industry, the system's ability to handle fine powders without particle degradation is crucial for maintaining product quality. The chemical industry utilizes these systems for transporting raw materials and finished products, while the minerals industry benefits from efficient handling of bulk materials like coal and ore. The benefits of these systems extend beyond material transport, including improved safety by reducing manual handling, enhanced product quality through consistent processing, and increased operational efficiency through automated control.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing positive pressure dilute phase pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's commitment to excellence is reflected in its state-of-the-art manufacturing facilities, rigorous quality control processes, and dedicated technical support team. The company's products are engineered to meet international standards and are backed by a comprehensive warranty and after-sales service, ensuring long-term reliability and customer satisfaction. HeadPowder serves clients globally, providing customized solutions that enhance operational efficiency and reduce costs in material handling processes. The company's expertise in pneumatic conveying technology, combined with its customer-centric approach, makes it a trusted partner for businesses seeking reliable and efficient material transport solutions.