For industrial applications dealing with sintered ash, efficient and reliable material handling is crucial. The sintered ash pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. based in China, offers a sophisticated solution to transport this material with precision and minimal environmental impact.
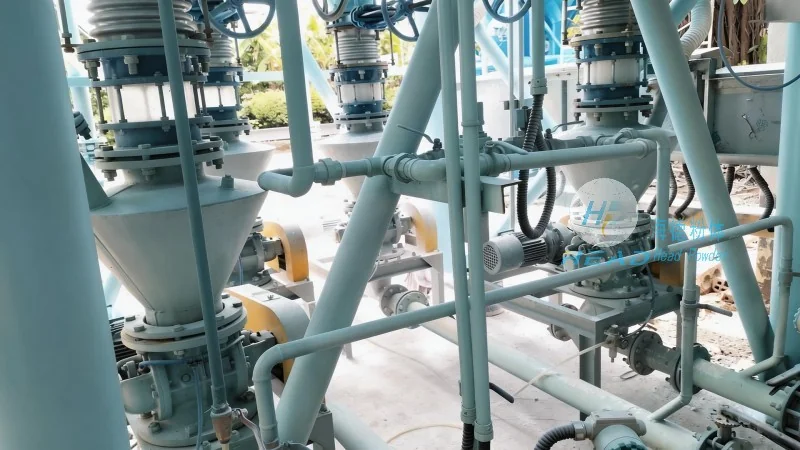
Company Introduction
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of powder handling and conveying systems, specializes in designing and manufacturing advanced pneumatic conveying solutions. HeadPowder, as the company is commonly known, is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality equipment tailored to the unique needs of various industrial sectors.
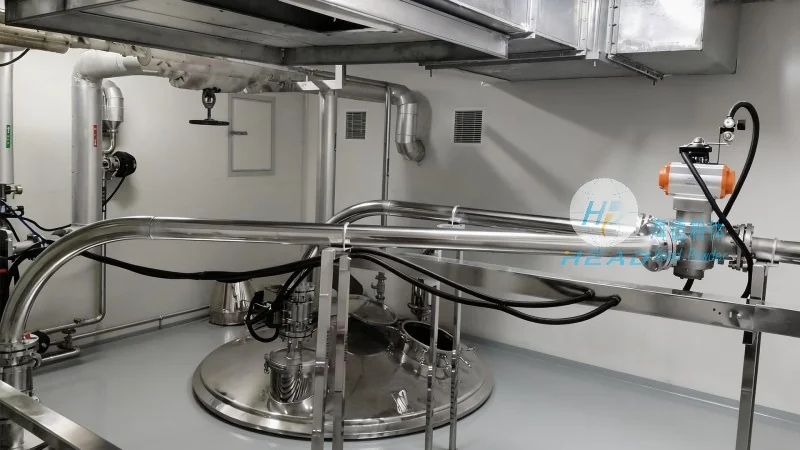
Working Principle of the Sintered Ash Pneumatic Conveying System
The sintered ash pneumatic conveying system operates on the fundamental principle of pneumatic transport, which involves the movement of material particles through a pipeline using a gas stream, typically air. In the case of sintered ash, the system utilizes a combination of positive and negative pressure stages to ensure effective and safe transportation. The process begins with the material being fed into the system, where it is introduced into a hopper or feeder. From there, the material is drawn or pushed by a fan or blower into the conveying line. The air flow, controlled by the system's pressure regulation components, creates a flow that carries the ash particles through the pipeline to the destination point, such as a storage silo or processing unit. The system is designed to handle the specific characteristics of sintered ash, including its particle size distribution, moisture content, and density, ensuring optimal performance and minimal wear on components.
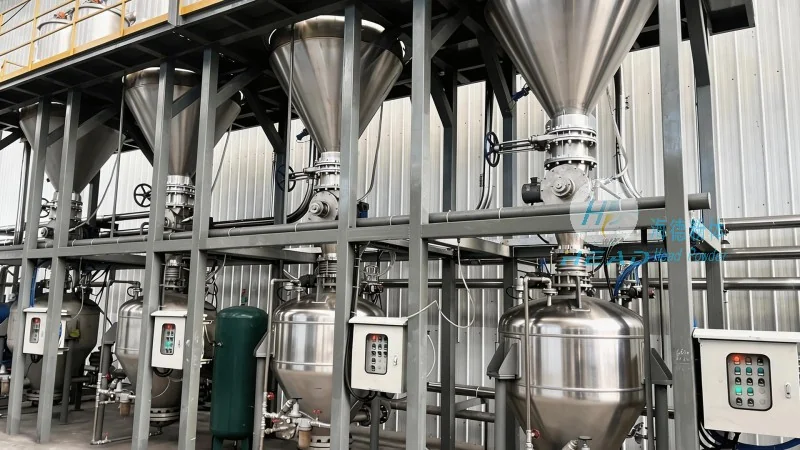
Key Features of the Sintered Ash Pneumatic Conveying System
The sintered ash pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is equipped with several notable features that enhance its functionality and efficiency. One of the primary advantages is its ability to handle abrasive materials like sintered ash without excessive wear on the system components. The system incorporates high-quality materials, such as wear-resistant liners and durable pumps, to extend the lifespan of the equipment. Additionally, the system is designed for low maintenance, with easy access to components for inspection and replacement, reducing downtime and operational costs. Another key feature is its environmental friendliness, as the system minimizes dust emissions compared to traditional methods like bucket elevators or belt conveyors. The enclosed pipeline design ensures that the ash is contained within the system, preventing contamination and protecting the surrounding environment. Furthermore, the system offers flexibility in terms of layout, allowing for horizontal, vertical, or mixed conveying configurations to suit the specific requirements of the industrial facility. The control system is user-friendly, with intuitive interfaces that enable operators to monitor and adjust the conveying parameters in real-time, ensuring consistent performance and optimal material flow.
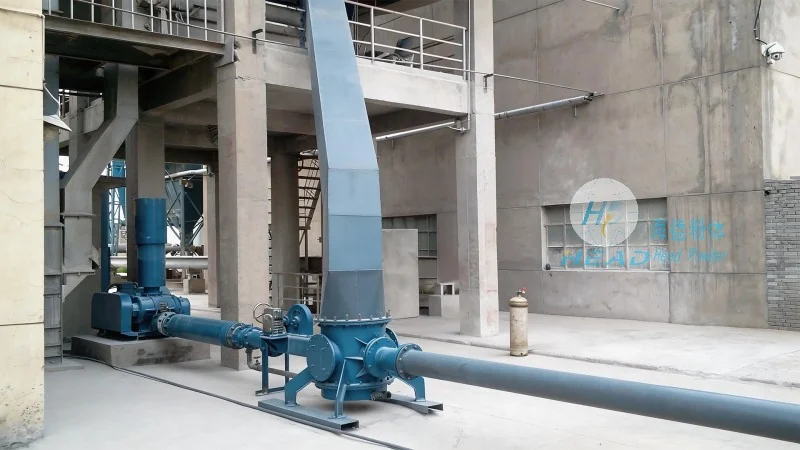
Applications and Benefits
The sintered ash pneumatic conveying system is widely used in various industrial applications where the efficient transport of sintered ash is essential. These applications include power plants, steel mills, and waste management facilities, where the material needs to be moved from storage areas to processing units or disposal sites. The system offers several benefits over traditional conveying methods, including increased efficiency, reduced labor costs, and improved safety. By eliminating the need for manual handling or mechanical equipment, the system minimizes the risk of accidents and injuries. Additionally, the enclosed design of the system reduces dust exposure for workers, contributing to a safer working environment. The system's ability to handle large volumes of material in a continuous manner also improves overall production efficiency, allowing facilities to operate at optimal capacity. Furthermore, the system's low maintenance requirements and long service life result in significant cost savings over time, making it a cost-effective solution for long-term material handling needs.




