

Principles and Features of Cocoa Pneumatic Conveying
Understanding the mechanics and advantages of cocoa pneumatic conveying systems is crucial for industries dealing with cocoa powder and related products. This article delves into the fundamental principles behind these systems and highlights their key characteristics, providing insights into how they operate efficiently and effectively.
Introduction to Cocoa Pneumatic Conveying
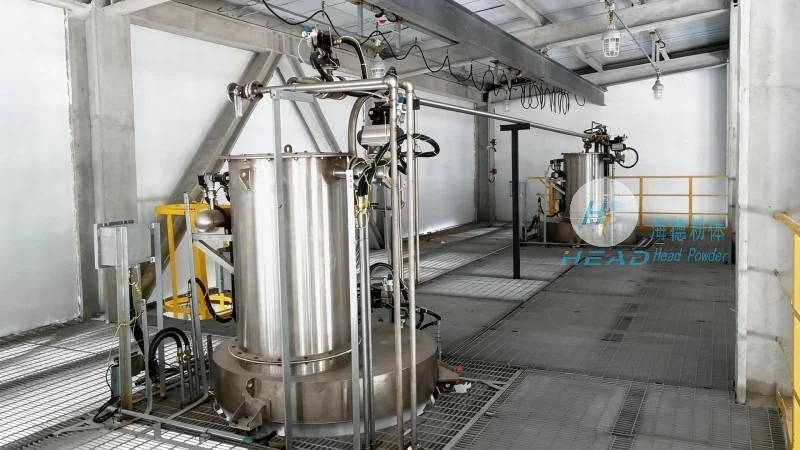
Cocoa pneumatic conveying systems are specialized equipment designed to transport cocoa powder and other fine particulate materials through a pipeline using air pressure. These systems are widely used in the food processing industry, particularly in cocoa processing plants, due to their ability to handle delicate materials without causing degradation or contamination. The core of these systems lies in the combination of air flow and material handling, which enables smooth and controlled movement of cocoa powder from one location to another.
Working Principle of Cocoa Pneumatic Conveying
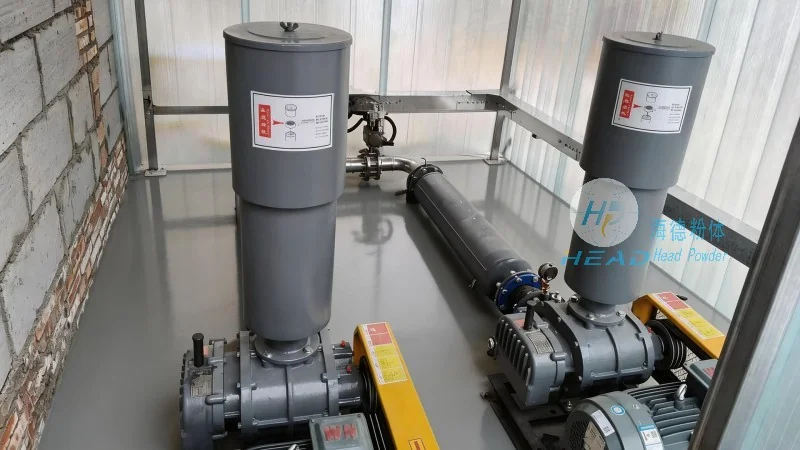
The fundamental principle of cocoa pneumatic conveying involves the use of compressed air to create a flow that propels the cocoa powder through a pipeline. The system typically consists of a hopper where the cocoa powder is stored, a blower or compressor that generates the air pressure, and a pipeline network that transports the material. As the air is introduced into the hopper, it creates a low-pressure zone that draws the cocoa powder into the pipeline. The air then carries the powder through the system, often with the assistance of cyclone separators or filters that separate the material from the air at the discharge point. This process ensures that the cocoa powder is transported efficiently without the need for mechanical components like belts or screws, which could potentially damage the delicate particles. The air pressure is carefully controlled to maintain a consistent flow rate, ensuring that the cocoa powder moves at a uniform speed and avoids any clogging or blockages in the pipeline. This controlled environment is essential for preserving the quality of the cocoa powder, as excessive air pressure or uneven flow can lead to particle breakage or agglomeration.
Key Features of Cocoa Pneumatic Conveying Systems
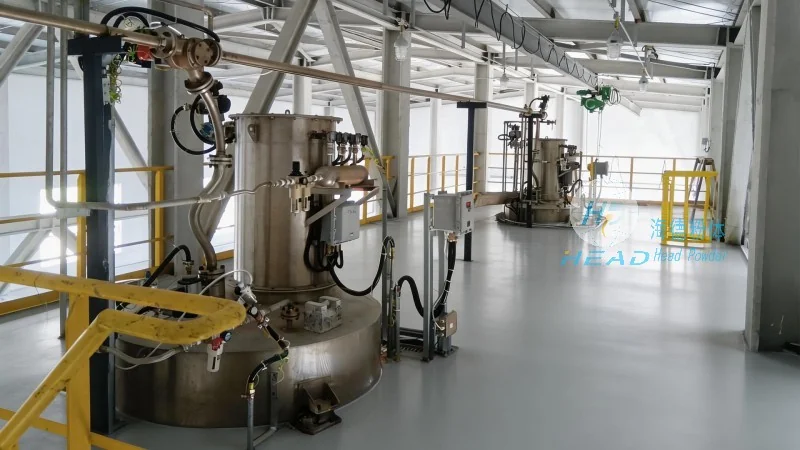
Cocoa pneumatic conveying systems offer several distinct advantages that make them ideal for handling cocoa powder. Firstly, they provide a hygienic and clean method of material transport, as the entire system is enclosed and the material is not exposed to external contaminants. This is particularly important in food processing applications where maintaining product purity is paramount. The enclosed design prevents dust and other particles from entering the system, and the materials used in the construction of the equipment are typically made from food-grade stainless steel, ensuring compliance with industry standards. Secondly, these systems are highly efficient in terms of energy consumption and operational costs. By using air pressure to move the material, they reduce the need for mechanical components that require regular maintenance and replacement, such as belts, screws, or augers. This leads to lower maintenance costs and increased uptime for the system. Thirdly, the systems are flexible and can be easily adapted to different production requirements. They can be scaled up or down depending on the volume of cocoa powder being processed, and the pipeline layout can be modified to accommodate changes in production flow. For example, additional branches can be added to the pipeline to transport cocoa powder to multiple processing units or storage areas. Additionally, the systems are capable of handling a wide range of particle sizes and moisture contents, making them versatile for various cocoa processing applications. Whether dealing with fine cocoa powder or larger cocoa nibs, the system can be adjusted to handle different material characteristics, ensuring optimal performance.
Applications and Benefits in Cocoa Processing
In the cocoa processing industry, cocoa pneumatic conveying systems are used in several critical stages. For instance, they are employed to transport cocoa beans from storage silos to roasting equipment, and then from the roaster to the grinding and milling stages. After grinding, the cocoa mass is conveyed to the drying and pressing units, where the cocoa butter and powder are separated. The cocoa powder is then conveyed to packaging lines or storage silos. The benefits of using these systems in these applications include reduced labor costs, improved product quality, and enhanced safety in the workplace. By eliminating manual handling of cocoa powder, the risk of dust exposure and respiratory issues is minimized, contributing to a safer working environment. Furthermore, the consistent and controlled transport of cocoa powder ensures that the final product meets the required quality standards, which is essential for meeting market demands and regulatory requirements. The uniform flow of cocoa powder also helps in maintaining consistent product characteristics, such as particle size distribution and moisture content, which are critical factors in the final product's taste and texture. This consistency is particularly important in the food industry, where product quality is a key differentiator for brands.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems for the food and powder processing industries. With a focus on innovation and quality, the company has developed advanced solutions tailored to the specific needs of cocoa processing plants. The company's expertise lies in designing and manufacturing customized pneumatic conveying systems that meet the highest standards of hygiene, efficiency, and reliability. By leveraging years of experience in the industry, headpowder has established itself as a trusted partner for businesses seeking to optimize their cocoa processing operations. The company's commitment to customer satisfaction and product excellence has earned it a reputation for delivering solutions that enhance productivity and reduce operational costs. Headpowder's team of engineers and technicians works closely with clients to understand their specific requirements and develop tailored solutions that address their unique challenges. Whether it's a new installation or an upgrade to an existing system, the company provides comprehensive support, including design, manufacturing, installation, and after-sales service. This comprehensive approach ensures that clients receive not just a product, but a complete solution that meets their operational needs and enhances their overall business performance. The company's facilities are equipped with state-of-the-art technology and adheres to strict quality control measures, ensuring that every product meets the highest standards before it is delivered to the client. This commitment to quality has helped headpowder build a strong reputation in the market and maintain long-term relationships with its clients.