

What is an Intelligent Tonne Bag Feeding Station for Powder Pneumatic Conveying System? And What Are
The intelligent tonne bag feeding station is a specialized system designed for the efficient handling and transfer of bulk powders from large tonne bags into pneumatic conveying systems. This technology is crucial in industries such as chemical, food, pharmaceutical, and mining, where the safe and reliable transfer of powders is essential for production continuity and product quality. The system integrates advanced automation and control technologies to ensure precise dosing, minimal material loss, and consistent flow rates, addressing the challenges associated with traditional manual or semi-automated feeding methods.
Key Components and Design Principles of the System
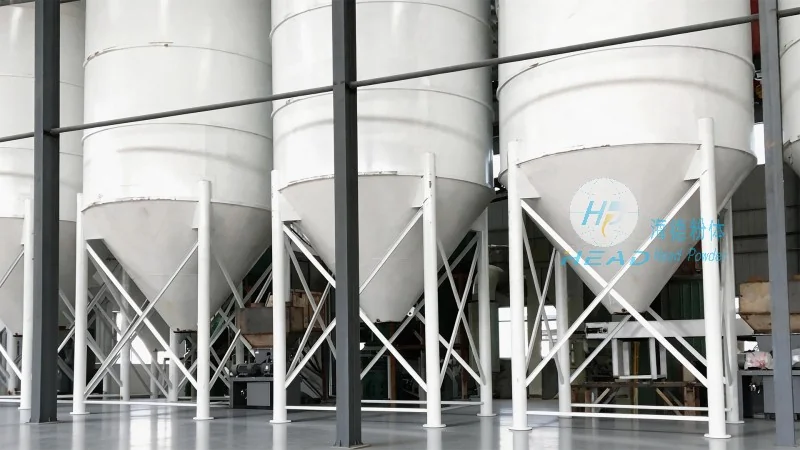
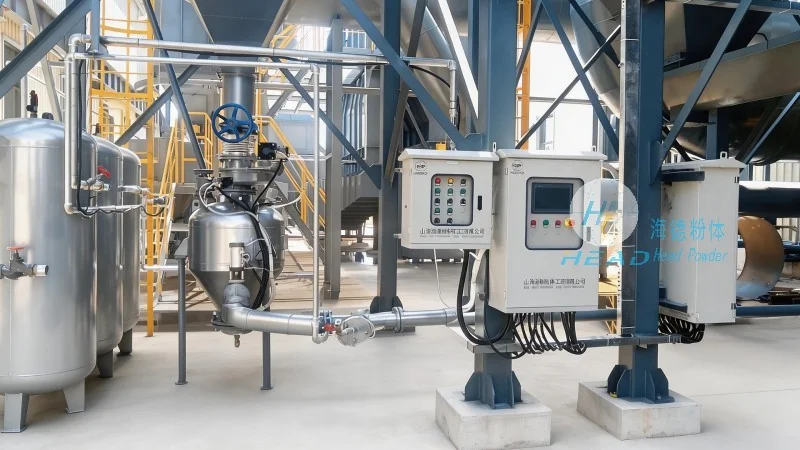
At the core of the intelligent tonne bag feeding station is a combination of robust mechanical components and intelligent control systems. The primary components include a tonne bag discharging mechanism, a powder feeding hopper, a pneumatic conveying pipeline, and an advanced control panel. The design principles are centered on safety, efficiency, and adaptability. Safety features are integrated to prevent dust explosions and material contamination, while the system is engineered to handle a wide range of powder properties, including different particle sizes, moisture contents, and flow characteristics. The control system utilizes sensors and feedback mechanisms to monitor and adjust the feeding process in real-time, ensuring optimal performance under varying operating conditions.
How the System Works: A Step-by-Step Overview
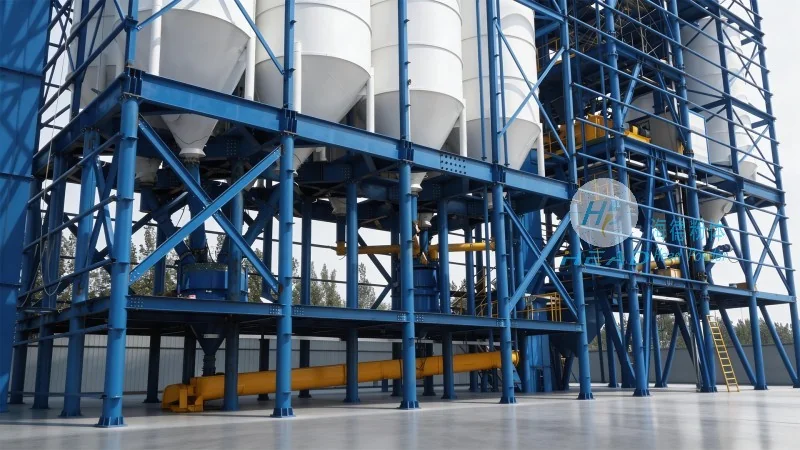
The operation of the intelligent tonne bag feeding station typically involves several key steps. First, the tonne bag is positioned on the discharge platform, and the bag opening mechanism is activated to release the powder into the feeding hopper. The hopper is equipped with a rotary valve or a screw feeder that controls the flow rate of the powder into the pneumatic conveying line. The control panel monitors the pressure and flow rates in the pipeline, adjusting the feeding speed as needed to maintain a stable and consistent flow. The system may also include features such as bag sealing and cleaning mechanisms to prevent material residue and ensure hygiene. Throughout the process, the control system provides real-time data and alerts for any deviations or issues, enabling quick troubleshooting and maintenance.
Advantages of the Intelligent Tonne Bag Feeding Station
Compared to traditional feeding methods, the intelligent tonne bag feeding station offers several significant advantages. Firstly, it enhances operational efficiency by automating the feeding process, reducing labor costs and minimizing downtime. The precise control of powder flow ensures consistent product quality and reduces material waste. Secondly, the system improves safety by eliminating manual handling of powders, which can be hazardous due to dust exposure or material contamination. The advanced control features also help in preventing equipment damage and reducing maintenance costs over time. Additionally, the system is designed for easy integration with existing production lines, allowing for seamless operation and minimal disruption to current workflows.
Applications and Industries Served
The intelligent tonne bag feeding station is widely used in various industries that require the handling of bulk powders. In the chemical industry, it is used for the transfer of raw materials such as powders, granules, and pellets. In the food and beverage industry, it is employed for the handling of ingredients like flour, sugar, and spices, ensuring compliance with hygiene and safety standards. The pharmaceutical industry also utilizes this system for the transfer of active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are critical. In the mining and mineral processing sector, the system is used for the handling of ores and other bulk materials, improving the efficiency of material processing and transportation.
Conclusion and Company Information
The intelligent tonne bag feeding station for powder pneumatic conveying is a sophisticated solution that addresses the challenges of modern bulk material handling. By combining advanced automation, precise control, and robust design, this system ensures efficient, safe, and reliable operation. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to the specific needs of various industries. With a focus on innovation and quality, HeadPowder delivers solutions that enhance productivity, improve product quality, and ensure compliance with industry standards. Based in Shandong, China, the company leverages its expertise and experience to provide comprehensive support and services to its clients worldwide.