

What is a corn kernel material handling system equipment? What are its design principles?
For industries dealing with corn kernels and other bulk materials, efficient material handling systems are crucial for maintaining productivity and ensuring product quality. This article explores the corn kernel material handling system equipment, detailing its components, operational principles, and the underlying design philosophies that make it effective in various industrial settings.
Introduction to Corn Kernel Material Handling Systems
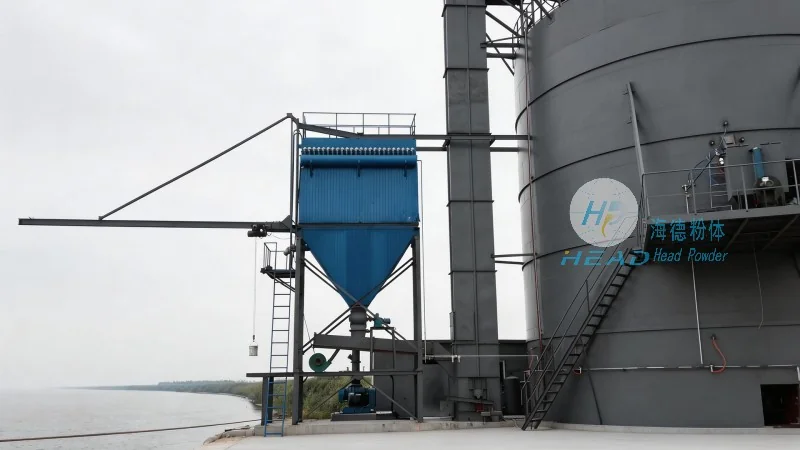
A corn kernel material handling system is a specialized piece of industrial equipment designed to transport, store, and manage corn kernels or similar bulk materials. These systems are integral to agricultural processing, food manufacturing, and feed production industries, where the efficient movement of raw materials is essential for streamlined operations. The system typically integrates multiple components, including conveyors, storage silos, and control mechanisms, to handle the entire material flow from reception to processing.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in China, specializing in the design and production of advanced material handling solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable equipment for corn kernel processing and other bulk material applications. HeadPowder's expertise lies in creating customized systems that meet the specific needs of clients, ensuring optimal performance and durability in demanding industrial environments.
What is a Corn Kernel Material Handling System Equipment?
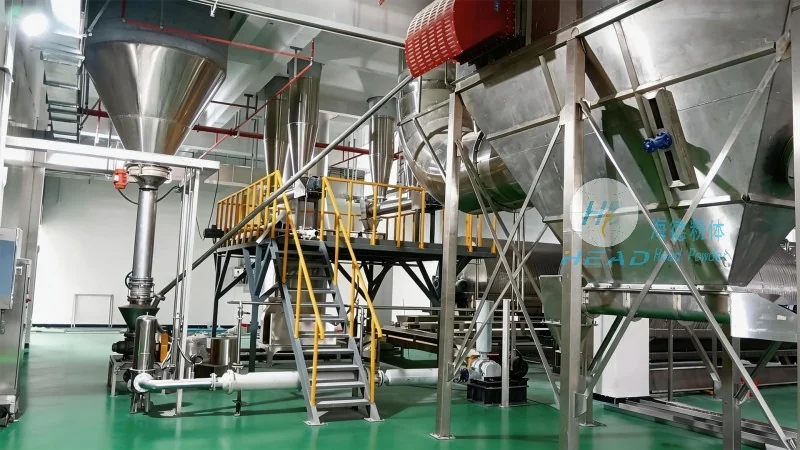
The corn kernel material handling system equipment is a comprehensive setup that facilitates the entire lifecycle of corn kernels—from raw reception to final processing. At its core, the system includes key components such as belt conveyors, bucket elevators, and storage silos. Belt conveyors are commonly used for horizontal or slight incline transport, while bucket elevators are ideal for vertical lifting and transporting corn kernels over longer distances. Storage silos are used to store large quantities of corn kernels, ensuring a steady supply for processing operations. Additionally, the system may incorporate sorting mechanisms, cleaning equipment, and feeding systems to enhance material quality and processing efficiency.
Design Principles of the System
The design of a corn kernel material handling system is guided by several key principles aimed at maximizing efficiency, safety, and durability. First, the system is engineered for high throughput, ensuring that it can handle large volumes of corn kernels without bottlenecks. This is achieved through the use of robust conveyor systems with high-capacity belts and efficient drive mechanisms. Second, the design emphasizes material flow optimization, minimizing the distance and number of transfers required to move corn kernels from one stage to the next. This reduces energy consumption and wear on equipment components. Third, safety is a critical consideration, with features such as emergency stop buttons, protective guards, and proper ventilation to prevent accidents and ensure operator safety. Fourth, the system is built for durability, using high-quality materials that can withstand the abrasive nature of corn kernels and the harsh conditions of industrial environments. Finally, the design allows for easy maintenance and scalability, enabling businesses to adapt the system as their needs evolve.
Components and Functions of the System
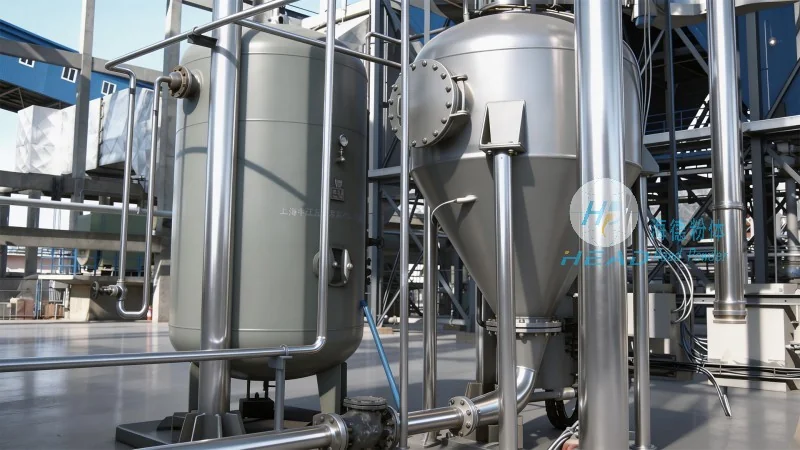
The corn kernel material handling system consists of several interconnected components, each playing a vital role in the overall operation. The primary components include: 1. **Receiving Hopper**: This component is used to receive raw corn kernels from trucks or other delivery vehicles. It typically features a sloped design to allow for smooth material flow into the system. 2. **Belt Conveyor**: The belt conveyor is responsible for transporting corn kernels horizontally or at a slight incline. It uses a motor-driven belt to move the material from the receiving hopper to the storage silo or processing area. 3. **Bucket Elevator**: The bucket elevator is used for vertical lifting and transporting corn kernels. It consists of a rotating drum with buckets attached, which scoop up the corn kernels and lift them to the desired height. 4. **Storage Silo**: The storage silo is a large, cylindrical container used to store large quantities of corn kernels. It is designed to maintain the quality of the material by controlling temperature and moisture levels. 5. **Sorting and Cleaning Equipment**: This component may include screens, magnets, and air classifiers to remove impurities and ensure the quality of the corn kernels before processing. 6. **Control System**: The control system is responsible for monitoring and regulating the operation of all components in the system. It uses sensors and automation to ensure smooth and efficient operation, with the ability to adjust parameters based on real-time conditions.
Common Applications
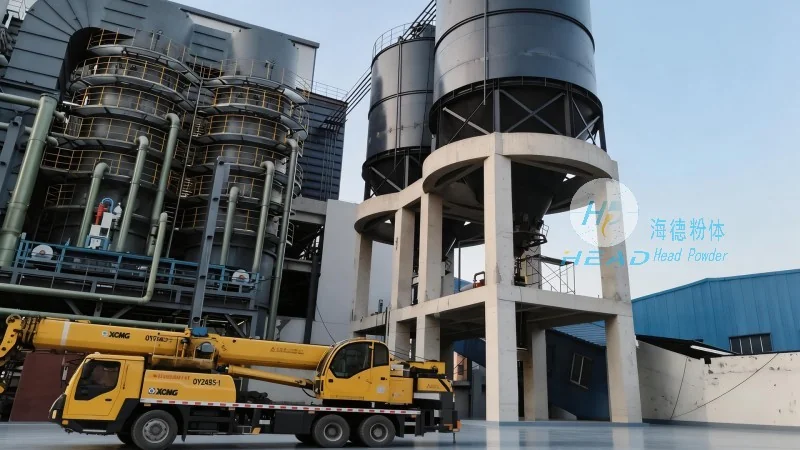
Corn kernel material handling systems are widely used in various industries, including food processing, animal feed production, and biofuel manufacturing. In food processing, the system is used to transport corn kernels to milling or grinding operations, where they are processed into cornmeal, corn flour, or other food products. In animal feed production, the system is used to move corn kernels to feed mills, where they are mixed with other ingredients to create animal feed. In biofuel production, the system is used to transport corn kernels to ethanol plants, where they are processed into bioethanol. The versatility of the system makes it suitable for a wide range of applications, ensuring that businesses can meet their specific material handling needs.
Conclusion
In conclusion, the corn kernel material handling system equipment is a critical component for industries dealing with corn kernels and other bulk materials. With its robust design and efficient operation, the system ensures that businesses can maintain high productivity and product quality. HeadPowder, as a leading manufacturer, offers customized solutions that meet the specific needs of clients, providing reliable and durable equipment for long-term use. By understanding the design principles and components of the system, businesses can make informed decisions about their material handling needs and choose the right equipment to support their operations.