Manganese carbonate is a critical industrial mineral used in various applications, including battery manufacturing, steel production, and chemical synthesis. Efficient handling and transportation of this material are essential for optimizing production processes and ensuring consistent quality. A well-designed material handling system for manganese carbonate plays a pivotal role in streamlining operations, reducing downtime, and enhancing overall productivity. This article explores the fundamental aspects of a manganese carbonate material handling system, including its design principles and key components.
Understanding the Core Components of a Manganese Carbonate Material Handling System
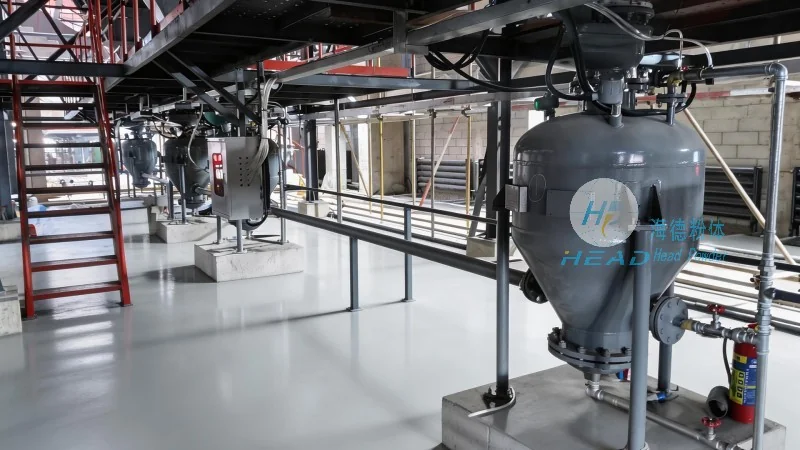
A typical manganese carbonate material handling system comprises several interconnected components that work in tandem to move the material from one location to another. These components include feeders, conveyors, storage silos, and processing equipment. Feeders are responsible for controlling the flow rate of the material, ensuring a consistent and controlled feed to the conveyor system. Conveyors, such as belt conveyors or screw conveyors, transport the material over long distances or vertical heights. Storage silos are used to store large quantities of manganese carbonate, providing a buffer for production fluctuations and ensuring a steady supply. Processing equipment, like crushers or classifiers, may be integrated into the system to prepare the material for further use.
Design Principles Behind Manganese Carbonate Material Handling Systems
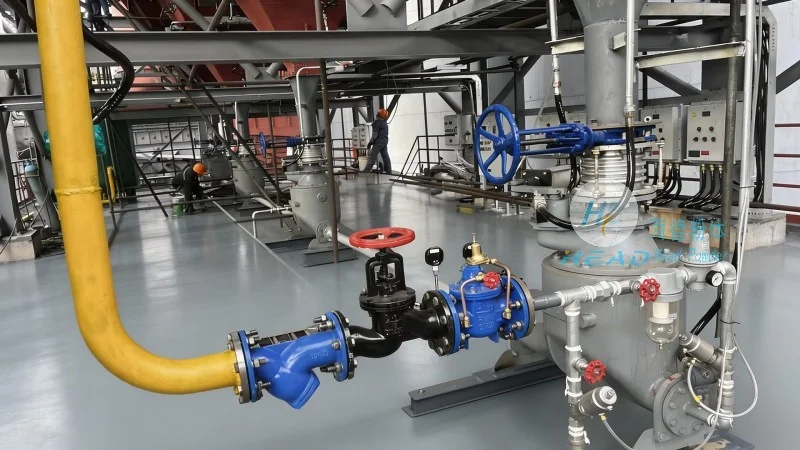
The design of a manganese carbonate material handling system is guided by several key principles to ensure efficiency, safety, and durability. First, the system must be designed to handle the specific physical properties of manganese carbonate, such as its particle size, density, and moisture content. This involves selecting appropriate equipment that can handle the material's characteristics without causing blockages or wear. Second, the system should prioritize safety, incorporating features like dust suppression systems, explosion-proof designs, and proper ventilation to protect operators and the environment. Third, the design must consider operational efficiency, minimizing energy consumption and maximizing throughput. This is achieved through the use of energy-efficient motors, optimized conveyor speeds, and streamlined material flow paths. Finally, the system should be built for durability and long-term reliability, using high-quality materials and robust construction to withstand the demanding conditions of industrial environments.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
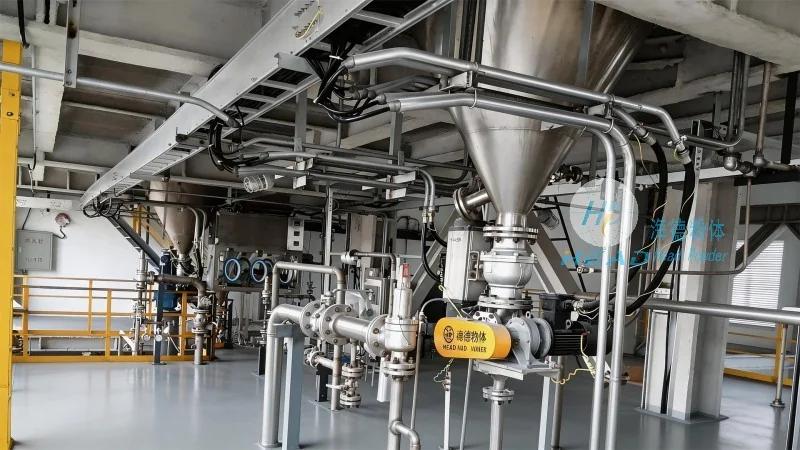
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of material handling systems for various industrial applications. With a strong focus on innovation and customer satisfaction, the company specializes in designing and manufacturing customized solutions tailored to the unique needs of its clients. HeadPowder's expertise lies in the development of efficient and reliable material handling systems, including those for manganese carbonate and other industrial minerals. The company's commitment to quality and precision ensures that its products meet the highest industry standards, providing long-term performance and durability. HeadPowder's facilities are equipped with advanced technology and skilled personnel, enabling the company to deliver superior products and services to its global clientele.
Key Features and Applications of Manganese Carbonate Material Handling Systems
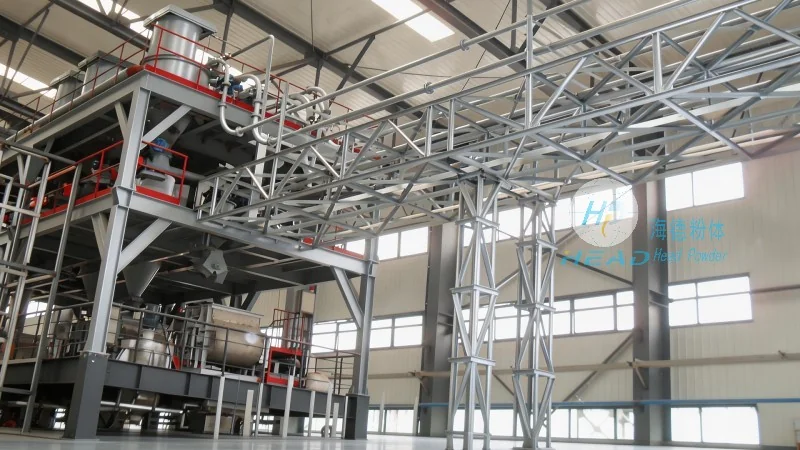
Manganese carbonate material handling systems are designed to meet the diverse needs of industrial processes. Key features include adjustable feed rates, variable speed conveyors, and integrated control systems that allow for real-time monitoring and adjustment. These systems are also equipped with safety features such as emergency stop buttons, overload protection, and dust collection systems. The applications of these systems are widespread, ranging from small-scale laboratory operations to large-scale industrial production facilities. In battery manufacturing, for example, manganese carbonate is used as a key component in lithium-ion batteries, and efficient material handling is crucial for maintaining consistent battery performance. In steel production, manganese carbonate is used as a deoxidizer and alloying agent, and the system ensures that the material is delivered to the furnace in the correct quantity and quality. Overall, manganese carbonate material handling systems play a vital role in enhancing the efficiency and reliability of industrial processes.




