Calcined ash powder conveying systems are specialized equipment designed to handle and transport calcined ash, a byproduct of coal combustion. These systems are crucial in industrial settings where efficient material handling is essential for maintaining operational efficiency and safety. The design of such systems involves careful consideration of material properties, environmental regulations, and operational requirements to ensure reliable and cost-effective performance.
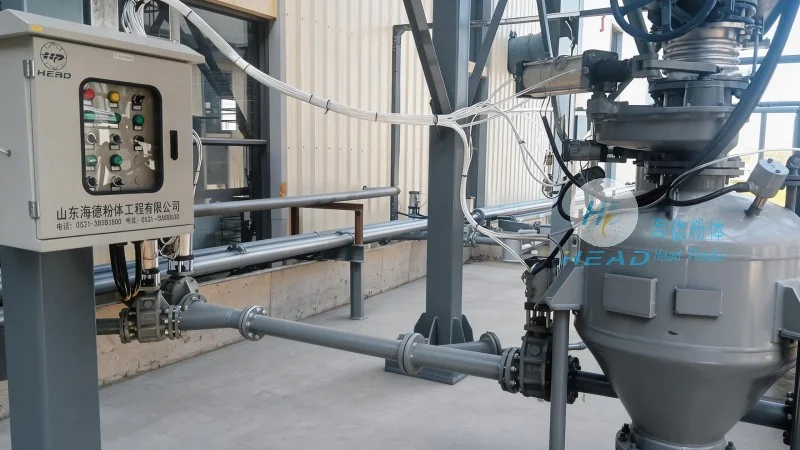
Understanding the Core Components of a Calcined Ash Powder Conveying System
At the heart of a calcined ash powder conveying system lies a series of interconnected components that work in tandem to move the material from its source to its destination. The primary components typically include a feeding mechanism, a conveying device (such as a screw conveyor, pneumatic conveyor, or bucket elevator), a control system, and a dust collection or filtration unit. Each component is engineered to address specific challenges associated with calcined ash, including its fine particle size, potential moisture content, and abrasive nature.
The Design Principles Behind Efficient Calcined Ash Powder Conveying
The design principles for calcined ash powder conveying systems are centered on maximizing efficiency, minimizing material loss, and ensuring compliance with environmental standards. Engineers at Shandong HeadPowder Engineering Co., Ltd. employ a systematic approach that begins with an analysis of the material's physical and chemical properties. This analysis helps determine the most suitable conveying method and equipment configuration. For instance, if the ash is dry and free-flowing, a screw conveyor may be preferred, while a pneumatic system might be more appropriate for wet or sticky ash. The system's design also incorporates features like aeration and vibration to prevent clogging and ensure smooth material flow.
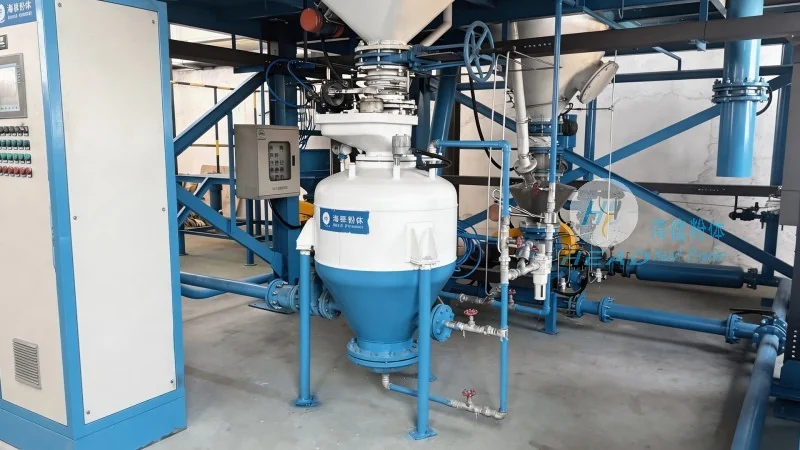
Key Features of a Professional Calcined Ash Powder Conveying System
Professional systems from Shandong HeadPowder Engineering Co., Ltd. are equipped with several key features that enhance their performance and reliability. These features include robust construction to withstand the abrasive nature of calcined ash, advanced control systems for precise flow regulation, and integrated dust suppression mechanisms to minimize environmental impact. Additionally, the systems are designed for easy maintenance and cleaning, with accessible components that allow for quick inspections and repairs. The company's expertise in material handling technology ensures that each system is tailored to meet the specific needs of the client, whether it's for a power plant, waste management facility, or industrial processing plant.
How the System Operates: A Step-by-Step Overview
The operation of a calcined ash powder conveying system involves several stages, each carefully engineered to ensure optimal performance. The process typically starts with the ash being fed into the system via a hopper or feeder. The material is then transported through the conveying device, which may use mechanical force (like a screw or belt) or pneumatic pressure (for air-based systems). As the ash moves through the system, it is continuously monitored for flow rates and any signs of blockage. The control system adjusts the speed or pressure as needed to maintain consistent operation. Finally, the ash is discharged at the desired location, often into a storage silo or for further processing. This step-by-step operation ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity.
Benefits of Using a High-Quality Calcined Ash Powder Conveying System
Investing in a high-quality calcined ash powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for industrial operations. These systems improve material handling efficiency by reducing the time and labor required to transport ash from one location to another. They also enhance safety by minimizing the risk of dust exposure and material spills, which can lead to health hazards and environmental contamination. Additionally, the systems are designed to be energy-efficient, reducing operational costs over time. By using advanced materials and engineering techniques, the company ensures that its systems provide long-term reliability and low maintenance requirements, making them a cost-effective solution for industrial clients.
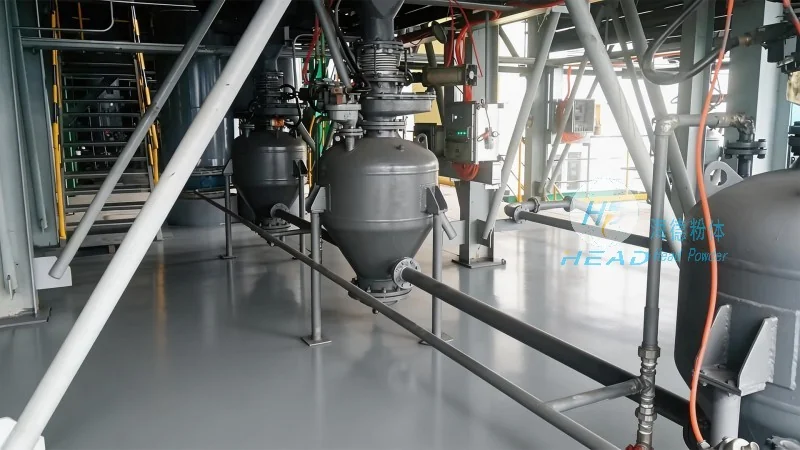
Customization and Application Flexibility
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial facility has unique requirements when it comes to calcined ash handling. Therefore, the company offers customized solutions tailored to the specific needs of its clients. Whether the ash is being transported over short or long distances, or in large or small quantities, the system can be designed to meet these requirements. The company's engineers work closely with clients to understand their operational challenges and provide solutions that integrate seamlessly with existing infrastructure. This flexibility ensures that the calcined ash powder conveying system not only meets but exceeds the expectations of the client, providing a reliable and efficient material handling solution.
Conclusion: The Importance of a Well-Designed Calcined Ash Powder Conveying System
In conclusion, a calcined ash powder conveying system is a critical piece of equipment for any industrial facility that handles calcined ash. The design principles and components of such a system are carefully engineered to ensure efficient, safe, and environmentally responsible material handling. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these systems, leveraging their expertise in material handling technology to meet the diverse needs of their clients. By investing in a high-quality conveying system, industrial facilities can improve their operational efficiency, reduce costs, and ensure compliance with environmental regulations, ultimately contributing to a more sustainable and productive operation.




