Understanding negative pressure dilute phase material handling is crucial for industries that rely on efficient and reliable transport of powders and granules. This method, also known as negative pressure pneumatic conveying, offers a solution for transporting bulk materials over moderate distances with minimal pressure differentials. In this article, we delve into the fundamental concepts of this technology and explore the key design principles that underpin its successful implementation.
What is Negative Pressure Dilute Phase Pneumatic Conveying?
Negative pressure dilute phase conveying is a type of pneumatic transport system where the conveying air is drawn into the system, creating a negative pressure environment. Unlike positive pressure systems that push air and material through a pipeline, negative pressure systems use suction to draw material from the source and transport it to the destination. This approach is particularly effective for applications requiring gentle handling of delicate materials, as it minimizes particle degradation and maintains product integrity.
Key Components of a Negative Pressure Dilute Phase System
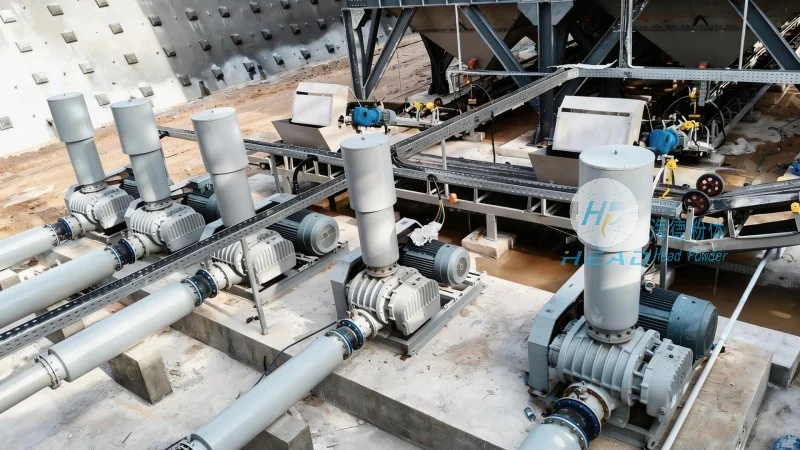
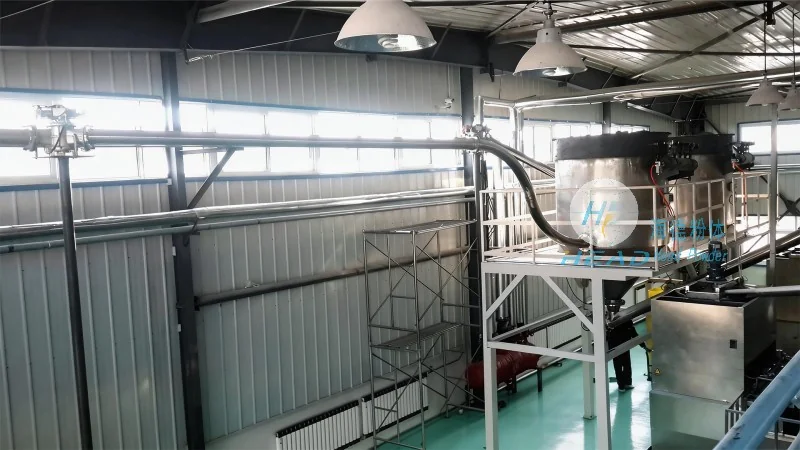
The core components of a negative pressure dilute phase system include the material feed hopper, the conveying pipeline, the receiver vessel, and the vacuum pump. The feed hopper is designed to store and meter the material, ensuring a consistent flow into the system. The pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The receiver vessel collects the conveyed material and may include a dust collection system to ensure environmental compliance. The vacuum pump generates the necessary suction to draw material through the pipeline, with the system operating at pressures below atmospheric levels.
How the System Works: The Conveying Process
The operation of a negative pressure dilute phase system involves several sequential steps. First, the material is introduced into the feed hopper, where it is metered and falls into the conveying pipeline. Simultaneously, the vacuum pump creates a negative pressure in the pipeline, drawing air and material particles into the system. As the material travels through the pipeline, it is suspended in the air stream and transported to the receiver vessel. The air flow continues to the receiver, maintaining the negative pressure and ensuring complete material transfer. The system then returns to the initial state, ready for the next cycle of material transport.
Design Principles for Optimal Performance
Designing an effective negative pressure dilute phase system requires careful consideration of several factors to ensure efficiency, reliability, and cost-effectiveness. Key design principles include selecting appropriate pipeline dimensions to maintain the material-air ratio within optimal ranges, ensuring adequate vacuum pump capacity to handle the system's resistance, and incorporating proper material handling features to prevent blockages or material degradation. Additionally, the system must be designed to minimize pressure drops and energy consumption, which are critical for long-term operational efficiency.
Applications and Industries
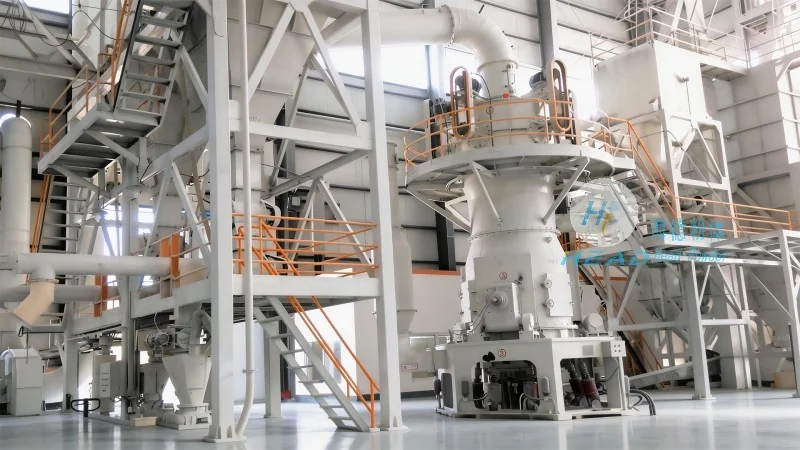
Negative pressure dilute phase conveying is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and minerals processing. Its ability to handle delicate materials, such as powders and granules, makes it ideal for applications where product quality and integrity are paramount. The technology is particularly suited for moderate transport distances, typically up to several hundred meters, and is often preferred in environments where positive pressure systems may pose safety or environmental risks.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of material handling solutions specializing in pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, HeadPowder offers comprehensive services, including system design, manufacturing, installation, and maintenance. The company's expertise in negative pressure dilute phase technology enables it to deliver tailored solutions that meet the unique needs of its clients. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing capabilities and a skilled workforce to produce high-quality equipment that meets international standards.




