Exploring the Sodium Hexafluorophosphate Powder Handling System and Its Core Design Principles
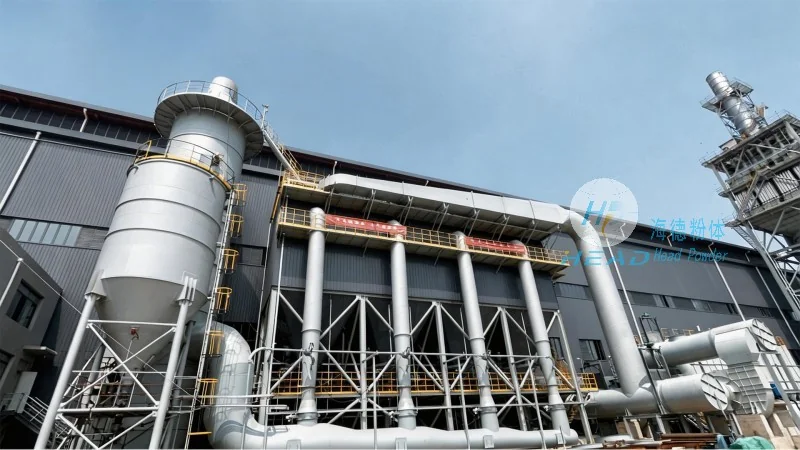
Overview of the Sodium Hexafluorophosphate Powder Handling System
The Sodium Hexafluorophosphate (NaPF₆) powder handling system is a specialized industrial equipment designed to handle, transport, and store this chemical compound efficiently and safely. As a critical component in industries such as lithium-ion battery manufacturing and high-tech material production, this system ensures optimal performance by addressing the unique challenges of fine powder handling. The system is engineered to manage issues like dust generation, material flow control, and environmental safety, making it essential for maintaining operational efficiency and product quality. Manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced powder handling solutions, the system is tailored to meet the specific requirements of handling NaPF₆, which includes its fine particle size, hygroscopic nature, and potential reactivity under certain conditions.
Key Components and Their Functions
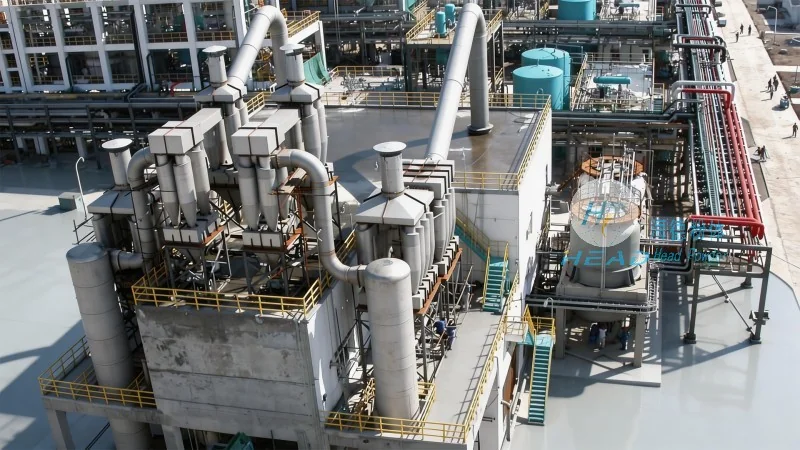
The Sodium Hexafluorophosphate powder handling system comprises several integrated components that work in concert to achieve reliable operation. These include a storage hopper for material containment, a feeder mechanism to regulate the flow rate of the powder, a conveyor system for transporting the material to processing units, and a dust collection system to ensure compliance with environmental and safety standards. Each component is selected based on the material's properties, with features like anti-static coatings, vibration mechanisms, and adjustable feeder speeds incorporated to prevent blockages and maintain consistent material flow. The system also incorporates explosion-proof and dust explosion-proof features to mitigate risks associated with handling potentially reactive powders, ensuring adherence to industrial safety regulations.
Design Principles for Efficient Material Handling
The design of the Sodium Hexafluorophosphate powder handling system is guided by several fundamental principles aimed at maximizing efficiency, safety, and reliability. A primary focus is on preventing material buildup and blockages, which can arise from the fine particle size and cohesive properties of the powder. To achieve this, the system utilizes anti-static measures, vibration technology, and variable feeder speeds to maintain consistent flow. Additionally, the design incorporates explosion-proof and dust explosion-proof features to address safety concerns, ensuring that the equipment can operate in environments where dust accumulation poses risks. The system is also engineered with corrosion-resistant materials to withstand the chemical properties of NaPF₆ and prevent product contamination.
Flow Control and Material Transport
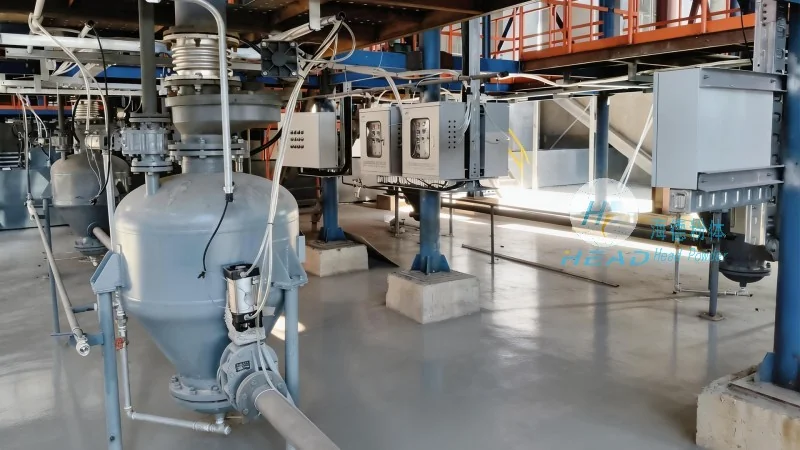
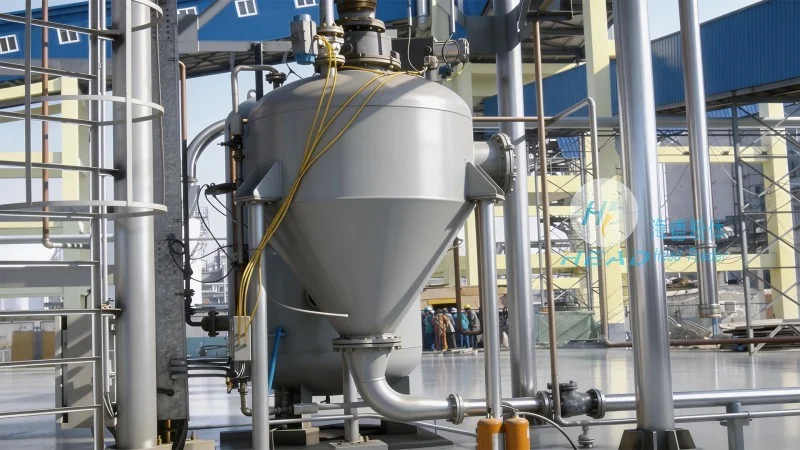
Effective flow control is a critical aspect of the Sodium Hexafluorophosphate powder handling system. The system employs advanced technologies such as rotary valves, screw conveyors, and pneumatic conveying systems to regulate the movement of the powder. These mechanisms are designed to minimize pressure drops and prevent material degradation, ensuring the powder remains in its optimal state throughout the handling process. Integrated control systems allow for precise adjustment of flow rates, which is essential for maintaining consistent product quality and preventing overloading or underloading of downstream processing equipment. The flexibility of these systems enables seamless integration into various production lines, supporting both small-scale and large-scale industrial applications.
Environmental and Safety Compliance
Given the potential hazards associated with handling Sodium Hexafluorophosphate, the system places a strong emphasis on environmental and safety measures. Dust collection and filtration systems are integrated to capture and neutralize airborne particles, preventing workplace contamination and environmental pollution. Safety interlocks and emergency stop mechanisms are also included to protect operators from risks like material spills or equipment malfunctions. The design ensures that the system operates within regulatory standards, providing a safe working environment and minimizing the risk of accidents or incidents. These features are crucial for maintaining operational continuity and ensuring long-term reliability in industrial settings.
Integration and Scalability in Industrial Processes
The Sodium Hexafluorophosphate powder handling system is typically integrated into larger industrial production lines, serving as a critical link between material storage and processing units. The modular design allows for easy installation and customization to meet specific operational needs, making it adaptable to different production scales. The system is engineered to be compatible with various downstream processes, such as mixing, grinding, and packaging, ensuring seamless operation and minimal downtime. This integration capability enhances overall production efficiency and supports the scalability of industrial operations. The system's ability to handle varying production volumes and material types makes it a versatile solution for companies operating in the chemical and battery manufacturing sectors.
Conclusion: The Importance of a Well-Designed Powder Handling System
In conclusion, the Sodium Hexafluorophosphate powder handling system is a sophisticated piece of equipment that plays a vital role in the efficient and safe management of this important chemical compound. The design principles and components of the system are carefully engineered to address the unique challenges of handling fine powders, ensuring optimal performance, safety, and environmental compliance. As industrial processes continue to evolve, the importance of such specialized equipment will only increase, making it essential for companies to invest in high-quality, well-designed powder handling systems to maintain competitiveness and operational excellence. The system's ability to deliver consistent performance and reliability makes it an indispensable asset for manufacturers relying on Sodium Hexafluorophosphate in their production processes.




