For industrial applications involving the handling of stone powder granules, selecting the right equipment is crucial for efficiency and safety. This article explores the concept of stone powder granule pneumatic conveying equipment and delves into its design principles, providing insights into how such systems operate and why they are essential in material processing industries.
Introduction to Stone Powder Granule Pneumatic Conveying Equipment
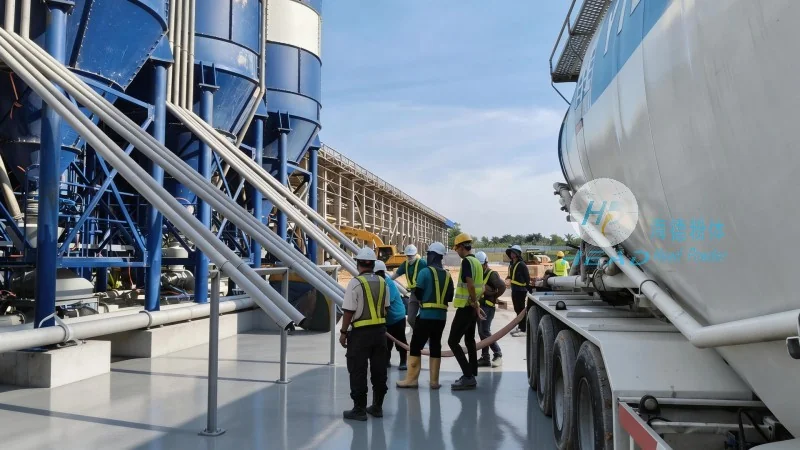
Stone powder granule pneumatic conveying equipment is a specialized system designed to transport dry, free-flowing materials like stone powder granules through a pipeline using air or other gases. Unlike traditional mechanical conveyors, which rely on mechanical components like belts or screws, pneumatic systems utilize the force of moving air to move materials, making them ideal for applications where dust control, flexibility, and minimal product degradation are required.
HeadPowder, a leading manufacturer in the field, offers advanced solutions tailored to the unique challenges of stone powder handling. The company’s expertise lies in designing systems that ensure reliable, efficient, and safe transportation of these granules, addressing the specific needs of various industrial sectors.
Key Components of Pneumatic Conveying Systems
A typical stone powder granule pneumatic conveying system consists of several key components that work in tandem to achieve effective material transport. These components include:
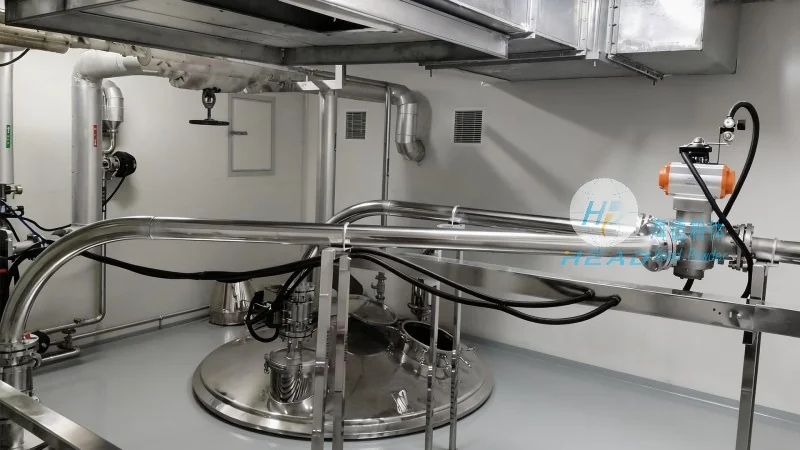
- Feeder: The feeder is responsible for introducing the stone powder granules into the conveying line. It ensures a consistent flow of material, preventing blockages and maintaining system efficiency.
- Conveying Line: The pipeline through which the stone powder granules are transported. The design of the line, including its diameter, length, and bends, is critical to minimize pressure drop and ensure smooth material movement.
- Air Supply System: This system generates the necessary air or gas flow to move the material. It includes compressors, filters, and regulators to maintain the required pressure and air quality.
- Separation and Collection System: At the end of the conveying line, this system separates the stone powder granules from the air stream and collects them in a designated container. Proper design is essential to prevent product loss and maintain air quality.
Design Principles for Optimal Performance
The design of a stone powder granule pneumatic conveying system follows several key principles to ensure optimal performance, reliability, and cost-effectiveness. These principles include:
1. Material Properties Consideration: The characteristics of the stone powder granules, such as particle size, density, and moisture content, are critical factors in system design. These properties determine the required air velocity, pressure, and equipment specifications to prevent blockages and ensure efficient transport.
2. Pressure Drop Management: Minimizing pressure drop is essential to reduce energy consumption and maintain system efficiency. Proper line sizing, use of smooth bends, and efficient feeder design help in managing pressure drop effectively.
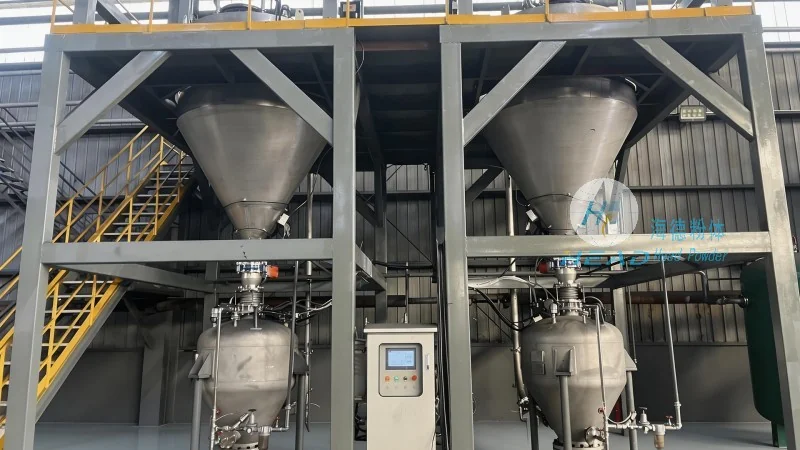
3. Air Velocity Optimization: The air velocity within the conveying line must be optimized to ensure that the stone powder granules are fully entrained and transported without causing excessive wear on the system components.
4. System Integration and Flexibility: Modern pneumatic conveying systems are designed to be flexible and adaptable to changing production needs. This includes features like multiple inlets and outlets, variable speed controls, and the ability to integrate with other processing equipment.
Benefits of Using Stone Powder Granule Pneumatic Conveying Equipment
Implementing a stone powder granule pneumatic conveying system offers several benefits for industrial operations. These include:
- Improved Efficiency and Productivity: Pneumatic systems can transport materials over long distances with minimal downtime, enhancing overall production efficiency.
- Enhanced Safety and Dust Control: By containing the material within a closed system, these equipment reduce dust emissions and improve workplace safety.
- Reduced Maintenance Costs: Compared to mechanical conveyors, pneumatic systems have fewer moving parts, leading to lower maintenance requirements and longer equipment lifespan.
- Flexibility in Layout: The ability to route the conveying line in various directions makes it easier to adapt to existing plant layouts or future expansions.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., based in China, is a trusted provider of high-quality stone powder granule pneumatic conveying equipment. With years of experience in the industry, HeadPowder combines advanced engineering with practical application knowledge to deliver systems that meet the specific requirements of clients.
The company’s products are designed to handle a wide range of stone powder granules, from fine powders to larger granules, ensuring versatility and reliability. HeadPowder’s commitment to quality and customer satisfaction has made it a preferred choice for businesses seeking efficient and reliable material handling solutions.




