When discussing the efficient and reliable transport of RARE Earth crystal powders, understanding the core structural components of pneumatic conveying systems is crucial. These systems are engineered to handle the unique properties of RARE Earth powders, which often include high value, fine particle sizes, and sensitivity to handling conditions. The main structures that form the backbone of such systems are designed to ensure optimal performance, material integrity, and operational safety.
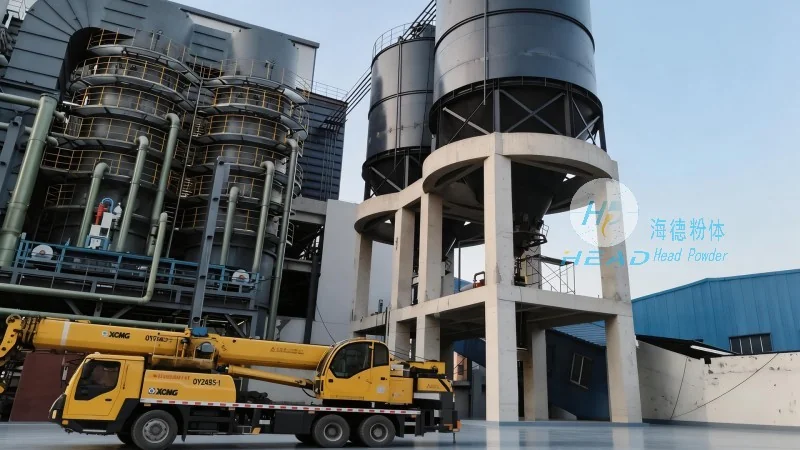
Key Structural Components of RARE Earth Crystal Powder Pneumatic Conveying Systems
The primary structural elements of a RARE Earth crystal powder pneumatic conveying system typically include the material feeding unit, the conveying pipeline network, the air supply and control system, and the material discharge and collection equipment. Each component plays a vital role in the overall functionality and efficiency of the process.
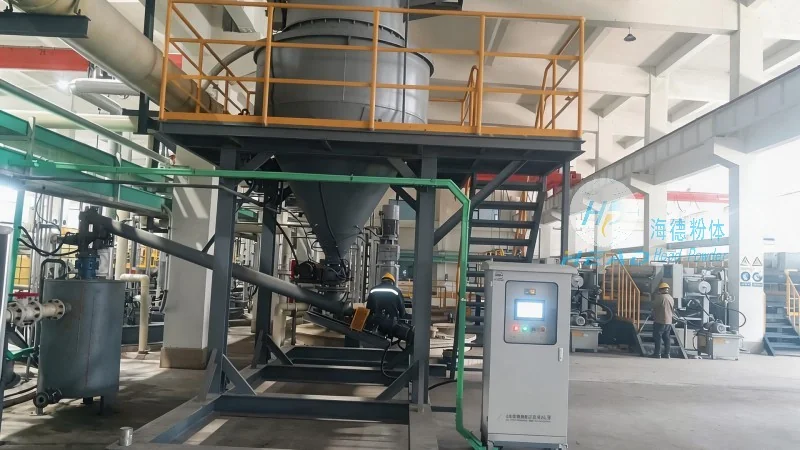
Firstly, the material feeding unit is responsible for introducing the RARE Earth crystal powder into the system. This unit must be designed to handle the specific characteristics of the powder, such as its flowability and potential for bridging or caking. Common feeding mechanisms include rotary valves, screw feeders, or pressure vessels, which ensure a consistent and controlled feed rate. The choice of feeding equipment is critical as it directly impacts the uniformity of the material flow and the prevention of blockages in the pipeline.
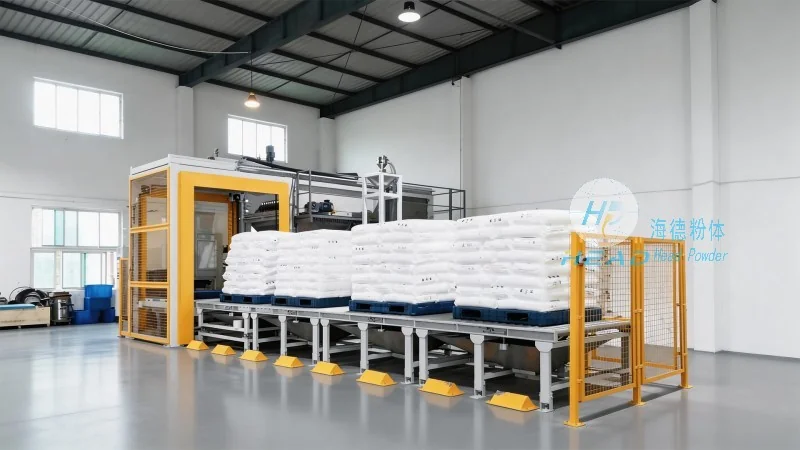
Secondly, the conveying pipeline network forms the core of the system, transporting the powder and air mixture from the feed point to the discharge point. The pipeline is typically made of materials resistant to corrosion and wear, such as stainless steel or specialized plastic composites, to withstand the abrasive nature of RARE Earth powders. The design of the pipeline, including the use of bends, elbows, and expansion joints, is carefully considered to minimize pressure losses and prevent material deposition or clogging. Proper pipeline sizing and the incorporation of cleaning mechanisms, like air blowers or mechanical scrapers, are essential for maintaining system efficiency over time.
Thirdly, the air supply and control system provides the necessary motive force to move the powder through the pipeline. This system includes a blower or compressor, air filters, and pressure regulators. The air is often preheated or conditioned to prevent moisture absorption or agglomeration of the RARE Earth powder, which could lead to operational issues. The control system monitors and adjusts the air flow rate and pressure in real-time, ensuring stable conveying conditions and protecting the equipment from overloading or underperformance.
Finally, the material discharge and collection equipment is responsible for receiving the RARE Earth powder at the end of the conveying process. This unit may include a cyclone separator, a bag filter, or a silo, which separates the powder from the air and collects it in a controlled manner. The design of the discharge system must prevent dust emissions and ensure the safe handling of the material, as RARE Earth powders can be hazardous if not managed properly. Additionally, the collection equipment is often equipped with dust suppression and ventilation systems to maintain a safe working environment.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider in the field of RARE Earth crystal powder processing and conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of the RARE Earth industry. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses requiring reliable and efficient material handling solutions. HeadPowder's expertise lies in understanding the specific challenges associated with RARE Earth powders, such as their high value and sensitivity to handling, and developing customized structural solutions that address these challenges effectively.
The company's facilities are located in Shandong, China, where it leverages advanced manufacturing technologies and a team of experienced engineers to develop cutting-edge conveying systems. HeadPowder's commitment to customer satisfaction and product excellence is reflected in its comprehensive service offerings, which include system design, installation, and maintenance support. By collaborating closely with clients, HeadPowder ensures that each pneumatic conveying system is optimized for the specific application, material characteristics, and operational requirements, delivering superior performance and longevity.




