Principles and Classification Applications of Organic Fertilizer Granule Pneumatic Conveying
Release time:2026-09-14 10:40:10
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Organic fertilizer granule pneumatic conveying is a key technology in the modern agricultural and fertilizer processing industry. This method involves transporting granular organic fertilizers through a pipeline system using air as the conveying medium. The process is efficient, clean, and suitable for various types of organic fertilizer production lines. Understanding the working principles and classification applications of this technology is crucial for optimizing fertilizer processing and distribution.
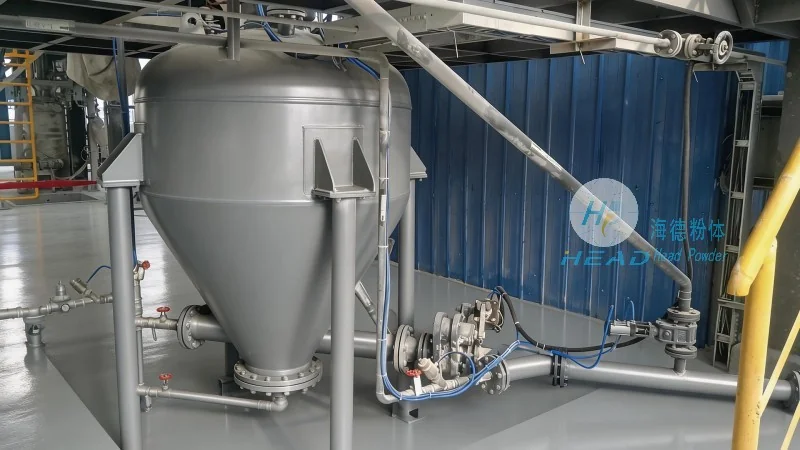
Working Principles of Pneumatic Conveying for Organic Fertilizer Granules
The core of organic fertilizer granule pneumatic conveying lies in the use of air pressure to move granular materials. The system typically consists of a material hopper, a blower or air compressor, a conveying pipeline, and a receiving hopper. When the system is activated, the blower generates a high-velocity air stream. This air stream carries the organic fertilizer granules through the pipeline, ensuring they are transported from the source to the destination without direct contact with mechanical components. The process can be either positive pressure (where air is pushed through the system) or negative pressure (where air is drawn through the system). For organic fertilizers, positive pressure systems are often preferred due to their ability to handle dusty or fine particles effectively, minimizing material degradation and ensuring consistent product quality.
Classification of Pneumatic Conveying Systems for Organic Fertilizers
Pneumatic conveying systems for organic fertilizer granules are categorized based on several factors, including the conveying pressure, system design, and application requirements. The main types include:
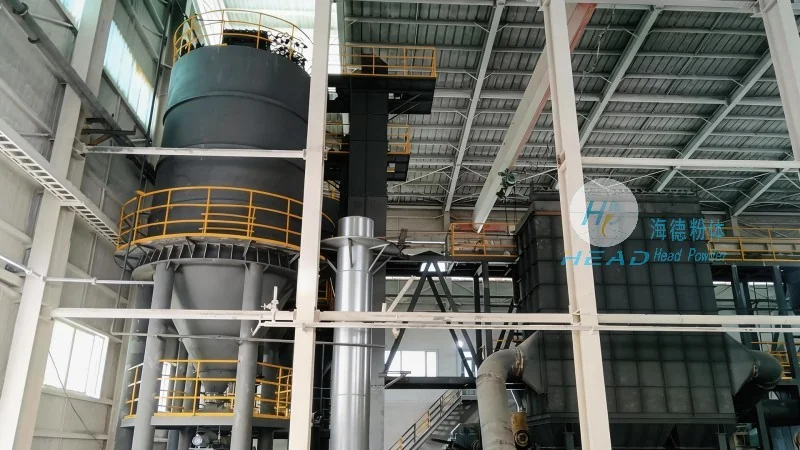
- Positive Pressure Systems: These systems use a blower to push air and material through the pipeline. They are ideal for long-distance conveying and can handle a wide range of particle sizes, from fine powders to larger granules. Positive pressure systems are commonly used in large-scale fertilizer production facilities where high throughput is required.
- Negative Pressure (Vacuum) Systems: In these systems, a vacuum pump creates a suction effect to draw material and air into the pipeline. They are suitable for shorter conveying distances and are often used in applications where dust control is a priority. Negative pressure systems are less common for organic fertilizers due to their lower capacity compared to positive pressure systems, but they are effective for handling sensitive materials that require gentle handling.
- Combination (Closed Loop) Systems: These systems use both positive and negative pressure components to create a closed loop, reducing air consumption and improving energy efficiency. They are particularly useful for recycling or re-conveying materials within a facility, such as returning excess fertilizer to a mixer or granulator.
Applications of Pneumatic Conveying in Organic Fertilizer Processing
The application of pneumatic conveying in organic fertilizer processing covers multiple stages, from raw material handling to final product packaging. Here are some key applications:
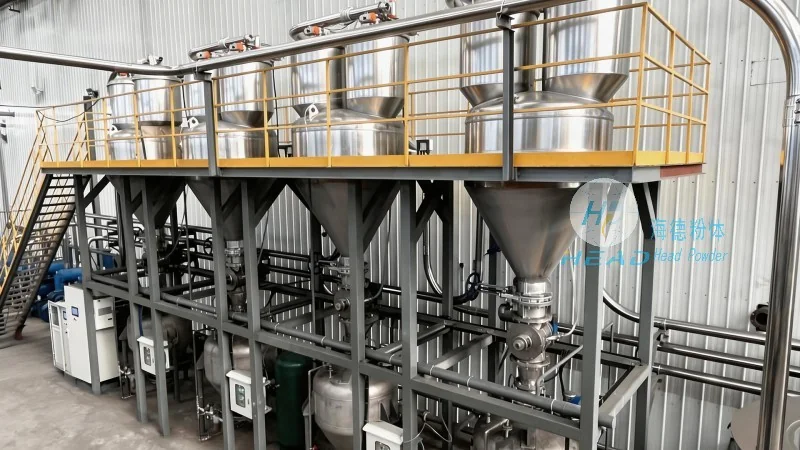
- Raw Material Conveying: Organic fertilizers are often produced from raw materials like compost, manure, and mineral additives. Pneumatic conveying systems efficiently transport these raw materials from storage silos or trucks to the processing plant. This ensures a continuous supply of raw materials, reducing downtime and improving production efficiency.
- Intermediate Processing: During the granulation process, organic fertilizer granules may need to be moved between different processing units, such as from a dryer to a screening machine or from a mixer to a packaging line. Pneumatic conveying allows for smooth and dust-free transfer of granules, maintaining product integrity and preventing contamination.
- Product Packaging and Distribution: After final processing, organic fertilizer granules are conveyed to packaging machines or storage silos. Pneumatic systems can deliver the product directly to packaging lines, ensuring accurate and consistent filling of bags or containers. This reduces manual handling and improves safety in the packaging area.
Advantages of Using Pneumatic Conveying for Organic Fertilizers
Implementing pneumatic conveying systems for organic fertilizer granules offers several advantages over traditional mechanical conveying methods:
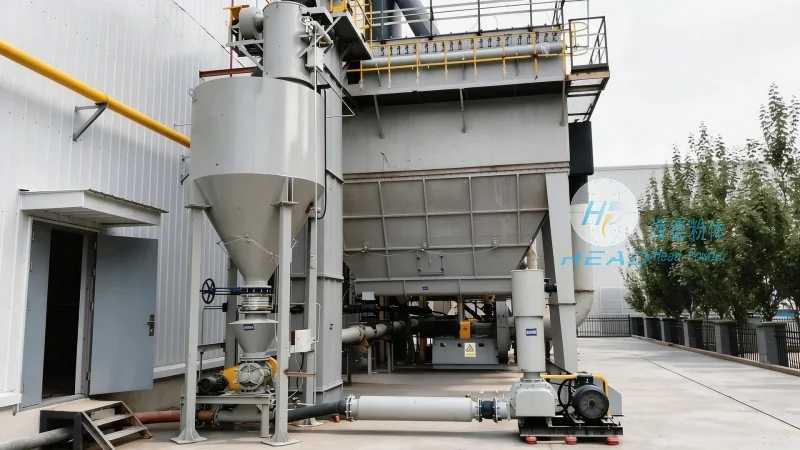
- Efficiency and Speed: Pneumatic systems can convey materials at high speeds, significantly reducing processing time compared to belt or screw conveyors. This leads to increased production capacity and lower operational costs.
- Cleanliness and Hygiene: As the material is transported in a closed pipeline, there is minimal exposure to the environment, reducing the risk of contamination from dust, moisture, or other external factors. This is particularly important for organic fertilizers, which may contain sensitive nutrients or microbial components.
- Space Efficiency: Pneumatic conveying systems require less floor space compared to traditional conveyors, making them suitable for facilities with limited space or complex layouts.
- Flexibility and Scalability: These systems can be easily modified or expanded to accommodate changes in production volume or product specifications. They can handle a wide range of particle sizes and moisture contents, making them versatile for different organic fertilizer formulations.
HeadPowder Engineering: Experts in Organic Fertilizer Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in providing comprehensive pneumatic conveying solutions tailored to the unique needs of organic fertilizer manufacturers. With years of experience in the industry, HeadPowder has developed advanced systems that optimize efficiency, reliability, and cost-effectiveness for fertilizer processing. The company’s expertise includes custom-designed positive pressure and combination systems, ensuring that each solution is tailored to the specific requirements of the client.
HeadPowder’s team of engineers and technicians works closely with clients to understand their production processes, material characteristics, and operational goals. By leveraging cutting-edge technology and rigorous testing, HeadPowder delivers systems that meet or exceed industry standards for performance and durability. The company’s commitment to quality and customer satisfaction has made it a trusted partner for many fertilizer producers worldwide.




