Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing advanced pneumatic conveying systems for industrial applications, including the soda ash material pneumatic conveying machine. This equipment is designed to efficiently transport soda ash, a critical raw material in various industries such as chemical manufacturing, food processing, and water treatment. The machine utilizes air as the primary transport medium, offering a dust-free and reliable solution compared to traditional methods.
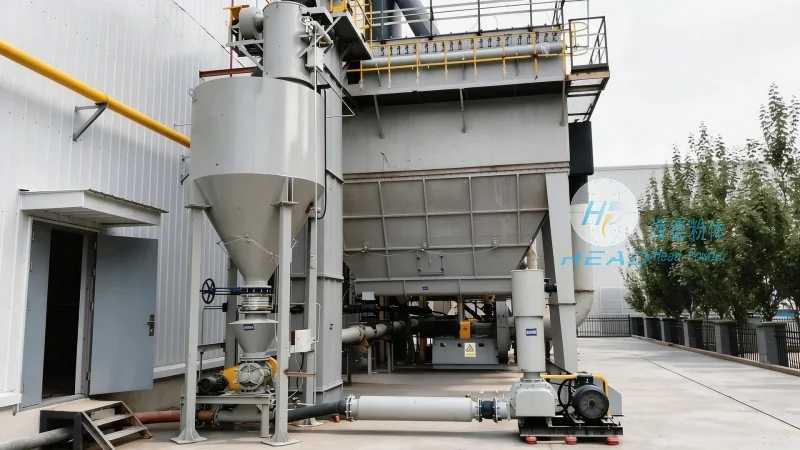
Key Components and Structure
The soda ash material pneumatic conveying machine consists of several critical components that work in tandem to ensure smooth operation. These include the hopper for material storage, the air compressor to generate the necessary air pressure, the conveying line where the material is transported, and the receiver where the material is deposited. Each component is engineered to withstand the specific demands of handling soda ash, ensuring durability and long-term performance.
Working Principle
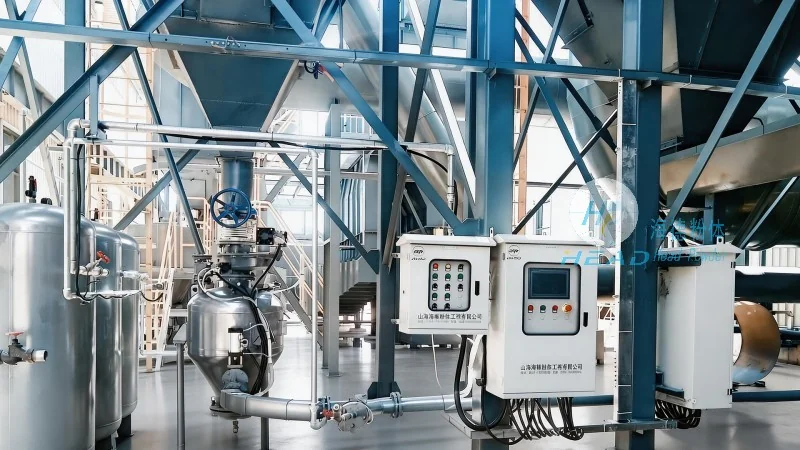
The operation of the soda ash material pneumatic conveying machine is based on the principle of pneumatic transport. When the machine is activated, the air compressor generates high-pressure air. This air is then introduced into the hopper, creating a vacuum or pressure differential that draws the soda ash particles into the conveying line. The air flow carries the material through the pipeline to the receiver, where the material is deposited. The system can operate in either positive or negative pressure modes, depending on the specific requirements of the application.
Operation Process
The operation process of the soda ash material pneumatic conveying machine begins with material loading into the hopper. The material is then fed into the conveying line as the air compressor starts and maintains the required air pressure. The material travels through the pipeline at a controlled speed, ensuring minimal wear and tear on the equipment. Upon reaching the receiver, the material is discharged, and the system can be adjusted to handle varying flow rates and material quantities. The entire process is automated, allowing for consistent and reliable material transport.
Advantages and Benefits
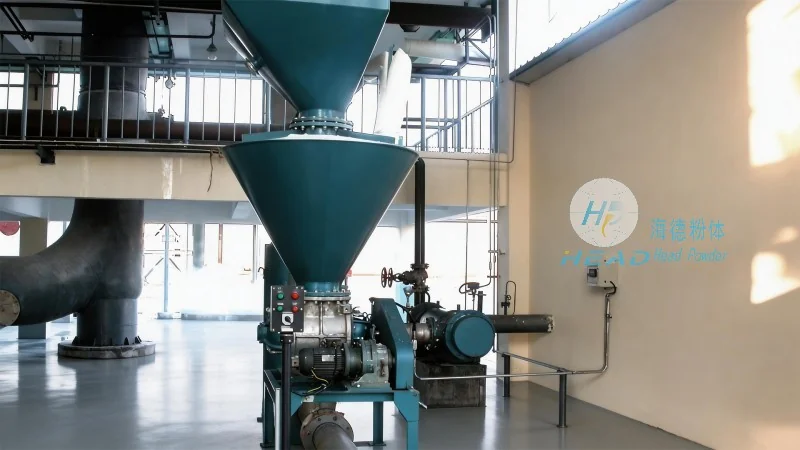
Using a soda ash material pneumatic conveying machine offers several advantages over traditional transport methods. The primary benefit is the elimination of dust and the ability to transport material in a closed system, which enhances safety and environmental compliance. Additionally, the system is compact and can be integrated into existing industrial setups with minimal modifications. The equipment also provides high efficiency in material transport, reducing labor costs and improving overall productivity. The durability of the components ensures long service life, making it a cost-effective solution for industrial operations.
Application Scenarios
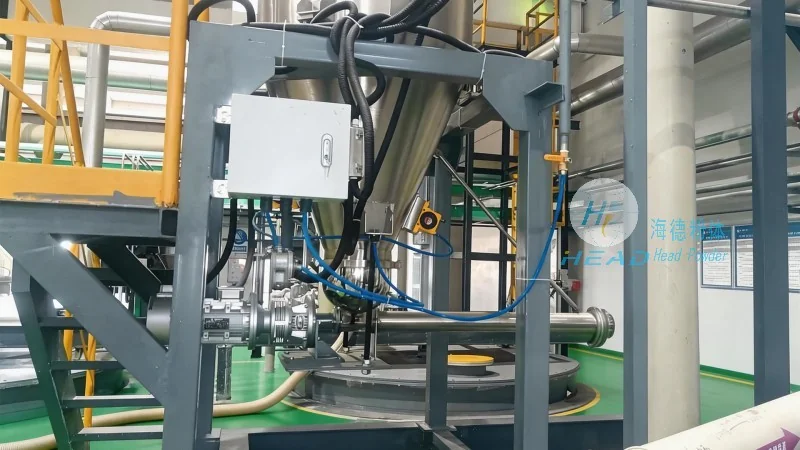
The soda ash material pneumatic conveying machine is widely used in various industrial applications where soda ash is a key raw material. These include chemical manufacturing, food processing, and water treatment facilities. In chemical plants, it is used to transport soda ash for production processes, while in food processing, it helps in the handling of soda ash used as a food additive. The versatility of the machine makes it suitable for different scales of operation, from small-scale production to large industrial facilities.
Maintenance and Safety Considerations
To ensure optimal performance and longevity of the soda ash material pneumatic conveying machine, regular maintenance is crucial. This includes checking the air compressor for proper operation, inspecting the conveying line for blockages or wear, and cleaning the hopper and receiver to prevent material buildup. Safety considerations are also paramount, as the system operates under pressure and with moving parts. Proper training for operators and adherence to safety protocols are essential to prevent accidents and ensure the safe operation of the equipment.




