In the realm of industrial material handling, particularly for coal powder, the pneumatic conveying machine stands out as a sophisticated solution that merges efficiency with operational precision. This equipment is engineered to transport fine coal powder from its source to the processing or storage area, offering a seamless and reliable method that addresses the unique challenges posed by this material. As industries strive for enhanced productivity and safety, understanding the operation process and working principle of such machinery becomes essential for optimizing material flow and reducing operational costs.
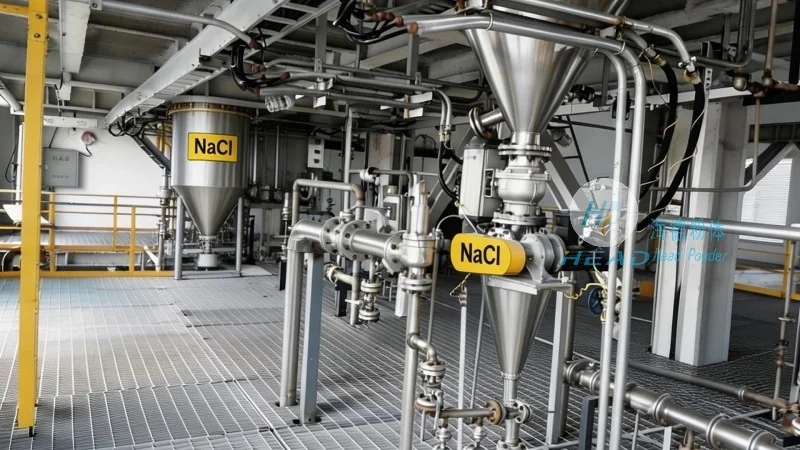
Company Overview: HeadPowder Engineering
HeadPowder Engineering, headquartered in Shandong, China, is a reputable manufacturer specializing in the design and production of pneumatic conveying systems tailored for coal and other fine powders. With years of experience and a commitment to innovation, the company has built a strong reputation in the industry for delivering high-quality equipment that meets international standards. Their team of engineers and technicians leverages advanced technology and rigorous testing to ensure that each machine is built to withstand the demands of continuous operation in demanding environments. By focusing on customer needs and providing tailored solutions, HeadPowder Engineering has become a trusted partner for businesses seeking reliable material handling solutions.
Key Components and Their Functional Roles
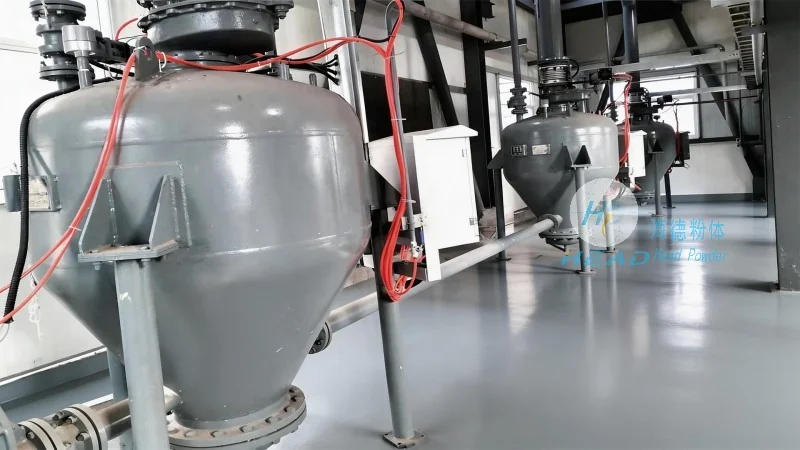
The coal powder pneumatic conveying machine comprises several integral components, each playing a critical role in the overall operation. The hopper serves as the primary storage unit, where coal powder is collected from the source and fed into the system. The air compressor or blower is the heart of the machine, generating the necessary air pressure to create the conveying stream. The pipeline system, typically made of durable materials like stainless steel or PVC, transports the coal powder-air mixture from the hopper to the discharge point. The control system, equipped with sensors and valves, regulates the air flow and pressure, ensuring stable and controlled operation. Additionally, the system may include filters and cyclones to separate the coal powder from the air at the discharge end, preventing dust emissions and maintaining air quality.
The Operation Process: A Detailed Step-by-Step
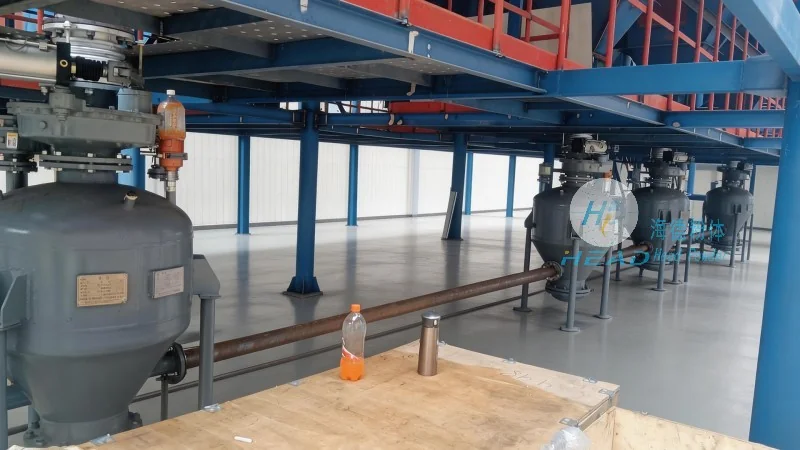
The operation of a coal powder pneumatic conveying machine follows a systematic sequence that ensures consistent and efficient material transport. Initially, coal powder is fed into the hopper from the storage silo. The control system then activates the air compressor, which starts generating a high-pressure air stream. This air is introduced into the pipeline, creating a flow that draws the coal powder particles into the system. As the air and powder mixture travels through the pipeline, it is guided towards the discharge point, where a cyclone or filter separates the coal powder from the air. The separated powder is then collected in the receiving container, while the air is either recirculated or discharged through a filter. The process is continuous, allowing for uninterrupted material transport from the source to the destination, with the control system continuously monitoring and adjusting parameters to maintain optimal performance.
Working Principle: The Physics Behind the Process
The working principle of the coal powder pneumatic conveying machine is rooted in the fundamental physics of pneumatic transport. It operates on the principle of creating a pressure differential between the inlet and outlet of the pipeline. The air compressor provides the necessary pressure to overcome the resistance of the pipeline and the gravitational force acting on the coal powder particles. The coal powder, being fine and lightweight, is easily entrained by the air stream, forming a slurry-like mixture that moves through the system. The velocity of the air stream is crucial; it must be sufficient to lift and transport the powder particles without causing excessive wear or energy consumption. The control system ensures that the air flow rate and pressure are maintained at optimal levels, preventing issues such as blockages or uneven flow. This principle allows for the efficient and safe transport of coal powder over long distances and varying elevations, making it suitable for a wide range of industrial applications.
Advantages and Practical Applications
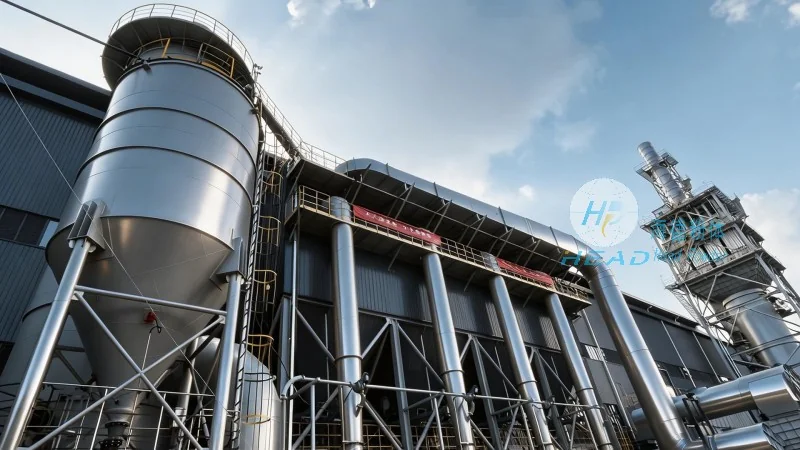
Employing a coal powder pneumatic conveying machine offers several distinct advantages over traditional material handling methods. One of the primary benefits is the reduction of dust contamination, as the material is transported in a closed system, minimizing environmental impact and health risks. Additionally, the equipment features fewer moving parts compared to mechanical conveyors, leading to lower maintenance costs and increased reliability. The closed system also helps in maintaining the quality of the coal powder, preventing moisture absorption or degradation during transport. These advantages make the pneumatic conveying machine ideal for use in power plants, coal processing facilities, and other industrial settings where the handling of coal powder is a critical operation. HeadPowder Engineering's machines are designed to meet the specific requirements of these applications, ensuring high performance, durability, and compliance with industry standards.




