Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a professional manufacturer and supplier specializing in the design, development, and production of advanced pneumatic conveying systems. With a focus on precision and efficiency, the company delivers high-quality solutions tailored to various industrial applications, including bulk material handling and transportation. Headpowder's commitment to innovation and customer satisfaction has established it as a trusted name in the field of material handling technology.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading enterprise in the field of material handling technology. The company is headquartered in Shandong, China, and has built a strong reputation for its innovative and reliable pneumatic conveying systems. With years of experience and a dedicated team of engineers, headpowder provides comprehensive solutions for industries that require efficient and controlled bulk material transport. The company's mission is to enhance operational efficiency and reduce costs for its clients through advanced technology and expert service.
Introduction to Metering Bin Pump Pneumatic Conveying System
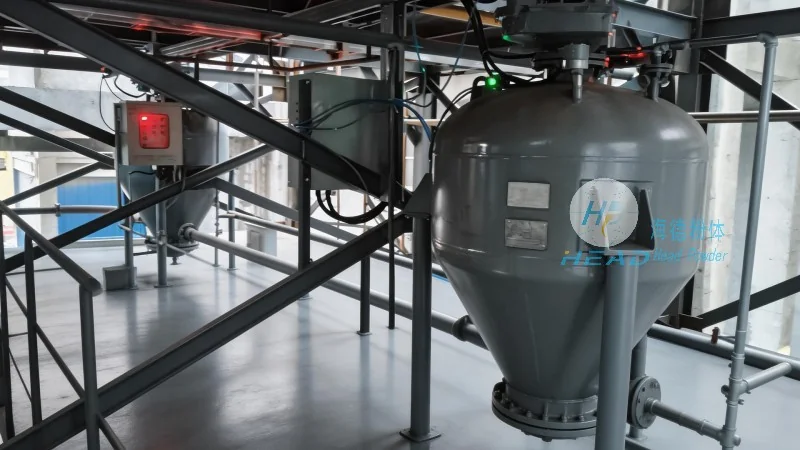
The metering bin pump material pneumatic conveying system is a sophisticated piece of equipment designed to transport bulk materials through a pressurized air system. This system integrates a metering bin, a pump mechanism, and a conveying pipeline, enabling the reliable and controlled movement of powders and granules from a storage silo or hopper to the desired destination. The system operates under positive pressure, ensuring that the material is conveyed without the need for mechanical components like screws or belts, which can be prone to wear and maintenance issues.
System Components and Their Functions
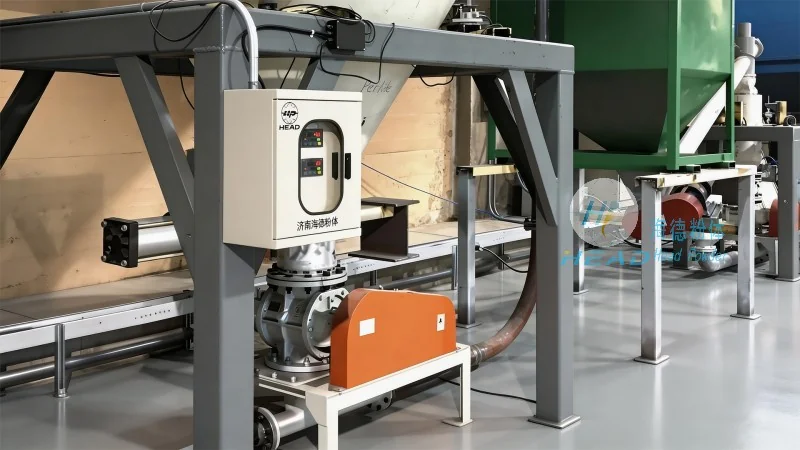
The metering bin pump system consists of several key components, each playing a critical role in the overall operation. The metering bin serves as the storage and feeding unit, holding the bulk material and regulating its flow into the pump. The pump mechanism, typically a diaphragm or rotary type, is responsible for mixing the material with compressed air and propelling it through the pipeline. The conveying pipeline transports the material from the pump to the destination, while the control system manages the pressure, flow rate, and other operational parameters.
Operation Process of the Metering Bin Pump System
The operation of the metering bin pump system begins with the loading of material into the metering bin. The material is then fed into the pump chamber, where it is mixed with a controlled amount of compressed air. The pump then applies pressure to this mixture, forcing it through the conveying pipeline to the end point. The system's control panel allows operators to adjust the flow rate and pressure, ensuring that the material is delivered at the desired rate. The process is continuous and automated, minimizing the need for manual intervention and reducing the risk of errors.
Working Principle Explained
The working principle of the metering bin pump system is based on the principles of fluid dynamics and air pressure. When the material is introduced into the pump chamber, it is combined with a controlled amount of air, forming a homogeneous mixture. The pump then uses its internal components to compress the mixture and propel it through the pipeline. The system's positive pressure environment prevents material from settling or clogging in the pipeline, maintaining a smooth and continuous flow. This approach is particularly effective for handling materials that are prone to dust, moisture, or abrasiveness, as it minimizes the risk of material degradation during transport.
Key Features and Benefits
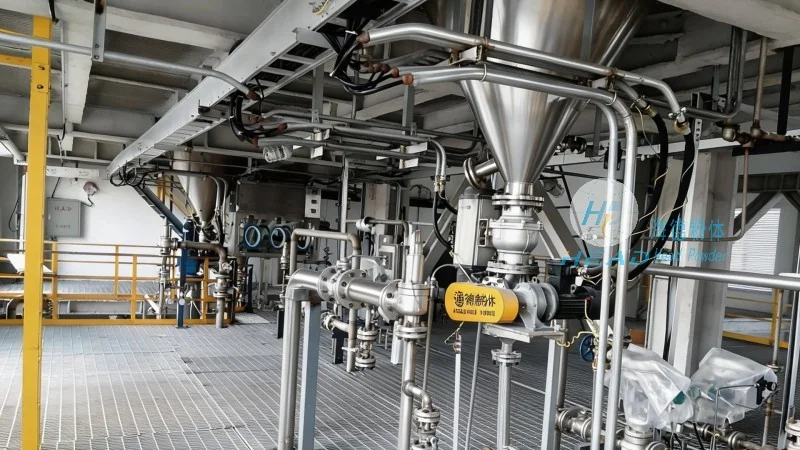
Key features of the metering bin pump material pneumatic conveying system include its ability to handle a wide range of materials, from fine powders to coarse granules. The system is also designed for high efficiency, with minimal energy consumption and low maintenance requirements. The use of a metering bin ensures that the material is fed at a consistent rate, preventing overloading or underfeeding of the pump. Additionally, the system's modular design allows for easy integration into existing industrial setups, making it a versatile solution for various production processes.
Applications in Various Industries
Applications of the metering bin pump system span multiple industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, the system is used to transport ingredients like flour, sugar, and spices with minimal contamination and loss. In pharmaceutical manufacturing, the system ensures that powders are handled in a sterile and controlled environment, meeting stringent quality standards. The chemical industry benefits from the system's ability to handle abrasive and corrosive materials without damage to the equipment. In mining operations, the system is used to transport ore and other bulk materials from processing plants to storage facilities, improving operational efficiency and reducing labor costs.
Customization and After-Sales Support
Headpowder's expertise in designing and manufacturing metering bin pump systems ensures that clients receive customized solutions that meet their specific operational needs. The company's team of engineers and technicians works closely with clients to understand their material characteristics, flow requirements, and production goals, developing systems that optimize performance and reliability. With a focus on quality and customer support, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive after-sales services, including maintenance, repair, and technical support, to ensure the long-term functionality of the equipment.
Advantages Over Traditional Conveying Methods
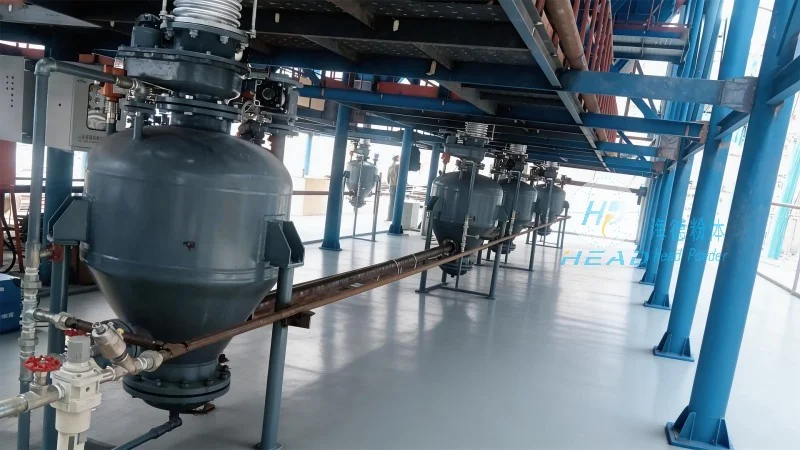
Compared to traditional conveying methods such as screw conveyors or belt conveyors, the metering bin pump system offers several advantages. The positive pressure operation eliminates the risk of material spillage and dust emissions, making it more environmentally friendly. The system also reduces the need for mechanical parts, leading to lower maintenance costs and longer equipment life. Additionally, the precise control over material flow allows for better process control and consistency in production.
Future Trends and Innovations
As technology advances, the metering bin pump material pneumatic conveying system continues to evolve, incorporating new features and improvements. Headpowder remains committed to staying at the forefront of this technology, investing in research and development to enhance the performance and efficiency of its systems. Future innovations may include the integration of smart sensors and automation technologies, further improving the system's reliability and operational efficiency. The company's focus on sustainability and energy efficiency also drives the development of more eco-friendly solutions for its clients.




