Positive pressure dilute phase material handling equipment is a critical component in modern industrial material transport systems, designed to efficiently move bulk materials over long distances with minimal pressure differentials. This equipment operates under positive pressure conditions, ensuring that the material is conveyed in a dilute phase, which enhances flow characteristics and reduces the risk of blockages. The technology is widely used in various industries, including mining, cement, chemical processing, and food processing, where reliable and efficient material transport is essential for operational efficiency and cost-effectiveness.
Company Introduction
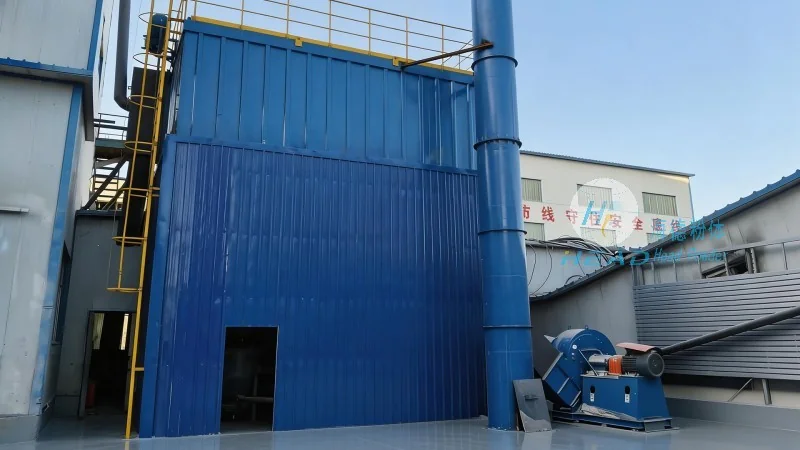
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and supply of advanced material handling solutions. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the industry. HeadPowder's commitment to quality and performance is reflected in its comprehensive product portfolio, which includes a range of positive pressure dilute phase equipment tailored to meet diverse industrial needs. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to deliver high-quality solutions to global markets.
Key Features of Positive Pressure Dilute Phase Equipment
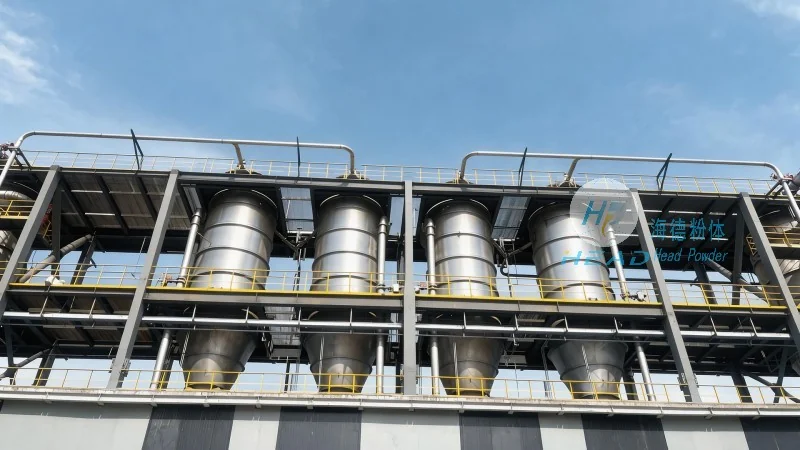
The core of positive pressure dilute phase material handling equipment lies in its ability to maintain a consistent positive pressure throughout the conveying system. This is achieved through a series of components that work in tandem to ensure smooth material flow. The equipment typically includes a positive displacement blower or compressor, which generates the necessary pressure to move the material. The material is then introduced into the system, often through a hopper or feeder, and mixed with air or gas to form a dilute phase. This dilute phase is then conveyed through a pipeline network, which may include bends, valves, and other components, to the destination point. The system is designed to maintain the material in a suspended state, preventing it from settling or clogging the pipeline.
Operation Process Overview
The operation of positive pressure dilute phase material handling equipment involves several key steps that ensure efficient and reliable material transport. The process begins with the loading of the material into the hopper or feeder. The material is then fed into the conveying system, where it is mixed with air or gas to form a dilute phase. The positive pressure generated by the blower or compressor then propels the material through the pipeline. The system is equipped with sensors and controls that monitor pressure, flow rate, and other parameters to ensure optimal performance. At the destination point, the material is discharged into a storage silo or processing unit. The entire process is automated, with minimal human intervention required, enhancing operational efficiency and reducing labor costs.
Working Principle Explained
The working principle of positive pressure dilute phase material handling equipment is based on the principles of fluid dynamics and particle suspension. The equipment operates by creating a positive pressure environment that forces the material to move through the pipeline. The material is suspended in a gas stream, which allows it to flow like a fluid. This suspension is maintained by the velocity of the gas and the size of the particles. The positive pressure ensures that the material does not settle or accumulate in the pipeline, preventing blockages and ensuring consistent flow. The system is designed to handle a wide range of materials, including powders, granules, and fine particles, with varying properties such as density, moisture content, and abrasiveness.
Advantages of Positive Pressure Dilute Phase Conveying
Positive pressure dilute phase material handling equipment offers several advantages over traditional conveying methods. One of the primary benefits is its ability to handle a wide variety of materials, including those that are difficult to convey using other methods. The dilute phase operation reduces the risk of clogging and blockages, which can lead to downtime and increased maintenance costs. Additionally, the equipment is energy-efficient, as it requires less pressure differentials compared to other systems. The positive pressure also ensures that the material is conveyed in a clean and hygienic manner, which is particularly important in industries such as food and pharmaceuticals. The system is also flexible, allowing for easy integration with existing industrial processes and modifications to accommodate changing production needs.
Applications in Different Industries
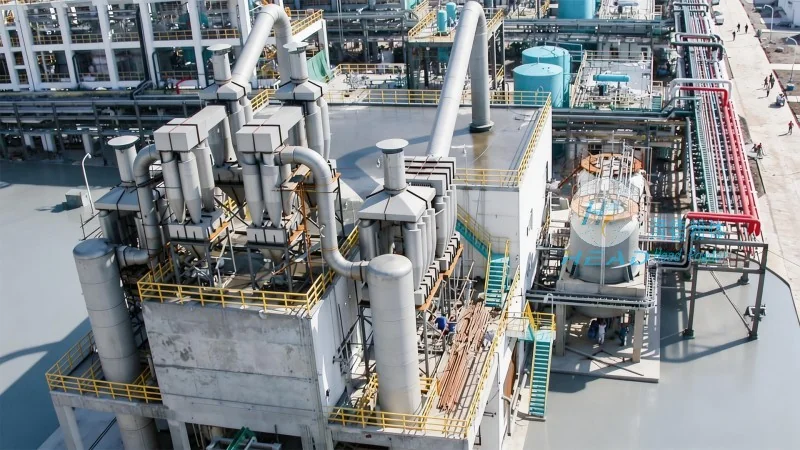
Positive pressure dilute phase material handling equipment is used in a variety of industries due to its versatility and efficiency. In the mining industry, it is used to transport ore and other minerals from the mine to processing facilities. In the cement industry, it is used to convey raw materials such as limestone and clay to the kilns. In the chemical processing industry, it is used to transport powders and granules for various production processes. In the food processing industry, it is used to convey ingredients such as flour, sugar, and spices, ensuring a clean and hygienic process. The equipment is also used in the pharmaceutical industry to transport raw materials and finished products, maintaining strict quality and safety standards.
Maintenance and Operational Considerations
Proper maintenance and operational considerations are essential to ensure the long-term performance and reliability of positive pressure dilute phase material handling equipment. Regular maintenance, including cleaning of the hopper, feeder, and pipeline, is necessary to prevent material buildup and clogging. The blower or compressor should be checked regularly for proper operation and efficiency. The system's controls and sensors should be calibrated to ensure accurate monitoring of pressure and flow rates. Additionally, the material being conveyed should be monitored for changes in properties, such as moisture content or particle size, which can affect the system's performance. By following proper maintenance procedures and operational guidelines, the equipment can operate efficiently and reliably, minimizing downtime and maximizing productivity.
Conclusion
Positive pressure dilute phase material handling equipment is a vital technology in modern industrial material transport, offering efficient, reliable, and flexible solutions for a wide range of applications. With its ability to handle diverse materials and maintain consistent performance, this equipment has become an essential component in many industrial processes. HeadPowder, as a leading manufacturer, continues to innovate and improve its products to meet the evolving needs of the industry, providing high-quality solutions that enhance operational efficiency and reduce costs for its customers.




