Carbon black and coal powder are essential raw materials in various industrial applications, and efficient material handling is crucial for maintaining production efficiency and quality. Pneumatic conveying systems, particularly those designed for carbon black and coal powders, offer a reliable solution for transporting these fine particles. This article explores the operation process and working principle of such equipment, highlighting key components and the technology behind its functionality.
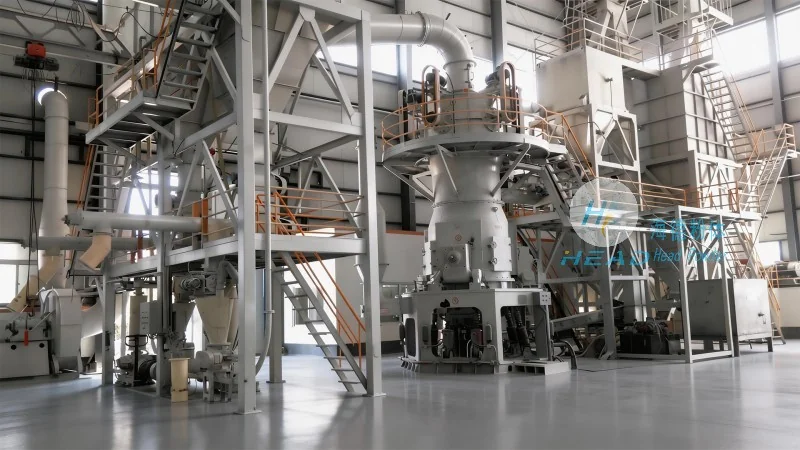
Key Components of the Pneumatic Conveying System
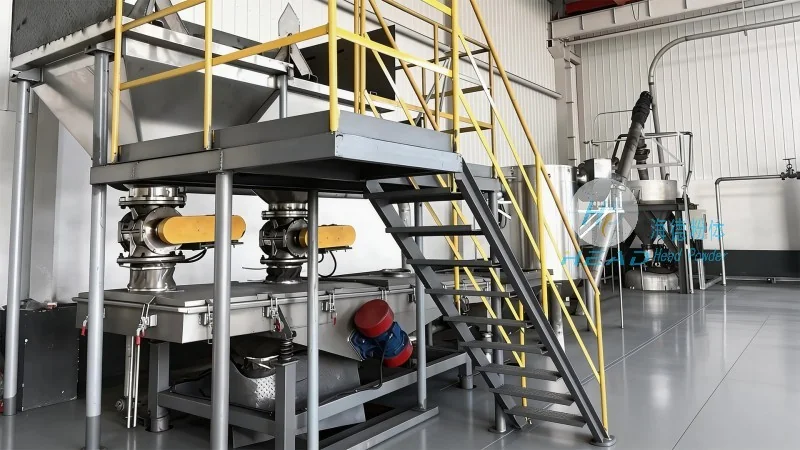
The carbon black coal powder pneumatic conveying machine typically consists of several core components that work in tandem to achieve efficient material transport. These include a hopper for material storage, a rotary valve or feeder to control the flow of powder, a conveying line (often equipped with a filter or separator), a blower or air compressor to generate the necessary air pressure, and a discharge outlet for the material. Each component plays a critical role in ensuring smooth and consistent operation.
Operation Process of the Pneumatic Conveying Machine
The operation process of the carbon black coal powder pneumatic conveying machine begins with the loading of carbon black or coal powder into the hopper. The material is then fed into the conveying line through a controlled feeder, such as a rotary valve, which regulates the flow rate to match the system's capacity. Simultaneously, the blower or air compressor generates a high-pressure air stream that is introduced into the conveying line. As the air flows through the line, it carries the powder particles along, creating a dense phase or dilute phase flow depending on the system design. The conveying line may include bends, filters, or separators to prevent blockages and ensure clean material transport. Finally, the material is discharged from the outlet, completing the transport cycle.
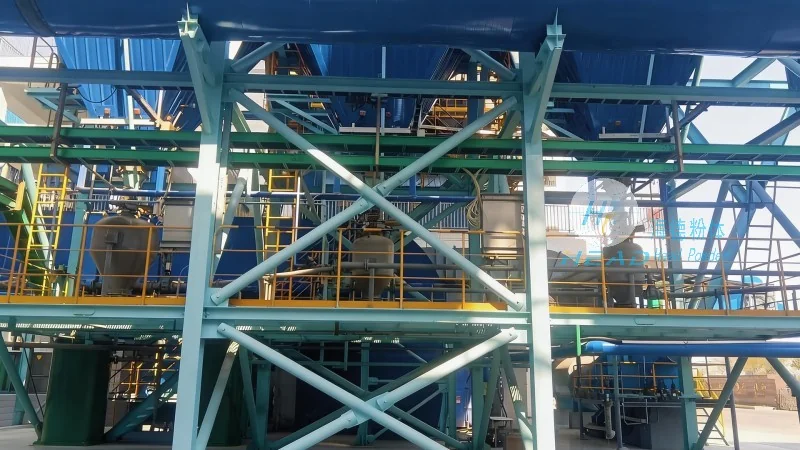
Working Principle of the Pneumatic Conveying System
The working principle of the carbon black coal powder pneumatic conveying machine is based on the principle of fluidization and particle suspension. When the air is introduced into the conveying line at a sufficient velocity, it creates a turbulent flow that lifts and transports the powder particles. The key to efficient operation lies in maintaining the correct air-to-material ratio, which ensures that the particles remain suspended without settling or causing blockages. The system's design, including the size of the conveying line, the velocity of the air, and the type of feeder, all contribute to achieving optimal performance. Additionally, the use of filters and separators helps maintain the purity of the material and protects the equipment from wear and tear.
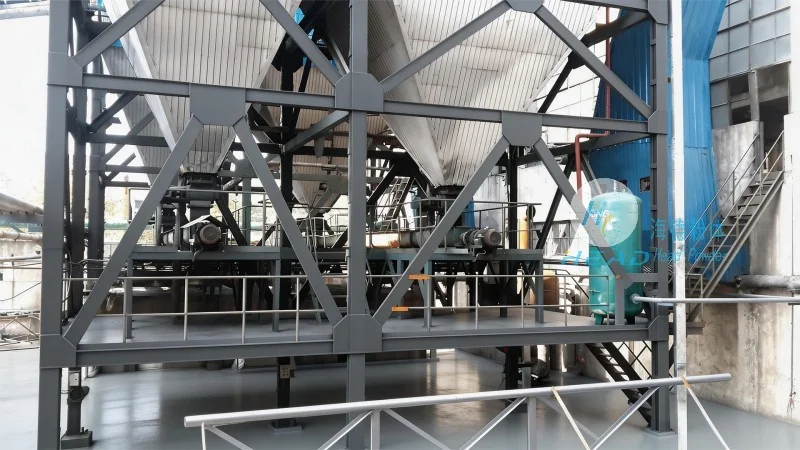
Advantages of Using Pneumatic Conveying for Carbon Black and Coal Powders
Implementing a pneumatic conveying system for carbon black and coal powders offers several advantages over traditional methods like belt conveyors or bucket elevators. These systems are capable of handling fine, abrasive powders without causing excessive wear, as the material is transported in a closed environment. The enclosed design also prevents dust emissions, improving workplace safety and environmental compliance. Furthermore, pneumatic conveying systems can transport materials over longer distances with minimal energy consumption compared to other methods. The flexibility of these systems allows for easy integration into existing production lines and the ability to handle varying material loads without significant adjustments.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of industrial conveying equipment. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries, including chemical, pharmaceutical, and mining. HeadPowder's expertise lies in developing efficient and reliable solutions for material handling, ensuring that clients achieve optimal performance and cost-effectiveness. The company's products are engineered to meet international standards and are backed by a commitment to customer satisfaction and technical support.
Conclusion
In summary, the operation process and working principle of carbon black coal powder pneumatic conveying machines involve a coordinated system of components working together to transport fine powders efficiently and safely. The technology offers significant advantages over traditional methods, including reduced dust emissions, improved material handling, and enhanced operational flexibility. For industries relying on carbon black and coal powders, investing in a well-designed pneumatic conveying system is a strategic choice for maintaining production efficiency and quality. As a trusted provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to deliver high-quality solutions that meet the evolving needs of industrial applications.




