HeadPowder, a leading provider of industrial material handling solutions, specializes in air-powered conveyors designed specifically for the transportation of rare earth mineral powders. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern rare earth processing facilities.
Understanding the Core Principle of Air-Powered Conveying Systems
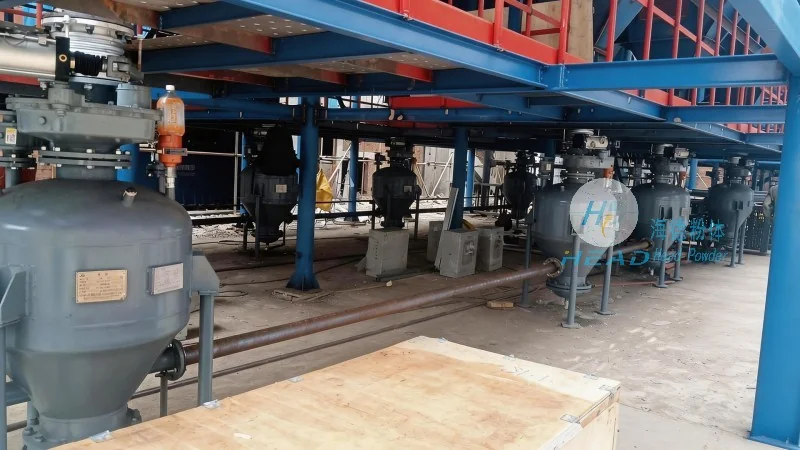
The air-powered conveyor, also known as a pneumatic conveyor, operates on the principle of using compressed air to move bulk materials through a pipeline. In the context of rare earth mineral powders, this technology efficiently transports fine, dry powders without the need for mechanical components like belts or buckets. The system typically consists of a blower, a hopper for material storage, and a series of pipes that direct the material to its destination. Compressed air is introduced into the system, creating a flow that lifts and propels the powder particles through the pipeline. This method is particularly effective for materials that are prone to caking or that require a dust-free environment, as it minimizes contact with external surfaces and reduces the risk of contamination.
Key Working Scene Characteristics of Rare Earth Mineral Powder Air-Powered Conveyors
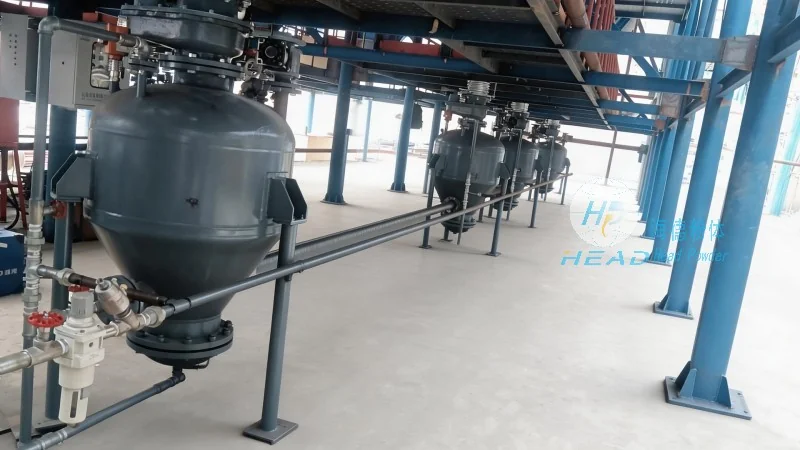
The application of air-powered conveyors in rare earth processing environments is defined by several critical characteristics that enhance operational efficiency and material integrity. Firstly, the system's ability to handle fine powders with high accuracy is crucial. Rare earth minerals often exist as micron-sized particles, and the air flow in the conveyor is carefully controlled to ensure uniform transport without segregation or loss. Secondly, the dust control features are paramount. In facilities where air quality is a concern, the sealed pipeline design of pneumatic conveyors prevents dust emissions, aligning with environmental regulations and maintaining a safe working environment. Thirdly, the flexibility of the system allows for multiple discharge points from a single inlet, enabling complex material routing within a processing plant. This is particularly valuable in rare earth processing, where materials may need to be directed to different refining or storage stages. Additionally, the low maintenance requirements of pneumatic conveyors reduce downtime and operational costs, making them a cost-effective solution for continuous production lines.
HeadPowder's Expertise in Designing Custom Air-Powered Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, leverages decades of experience in engineering and manufacturing to develop tailored air-powered conveyor systems for the unique demands of rare earth mineral processing. The company's engineers work closely with clients to assess their specific material characteristics, such as particle size distribution, moisture content, and flowability, to design a conveyor that maximizes efficiency and minimizes material degradation. HeadPowder's solutions are built with high-quality materials, including corrosion-resistant components for handling potentially acidic or reactive rare earth compounds, ensuring long-term durability and reliability. The company also provides comprehensive support, including installation, maintenance, and technical training, to ensure that clients can operate their air-powered conveyors at peak performance. By combining advanced engineering with a deep understanding of the rare earth industry, HeadPowder delivers systems that not only meet but exceed the operational standards required in modern processing facilities.
Conclusion: The Advantages of Air-Powered Conveyors in Rare Earth Processing
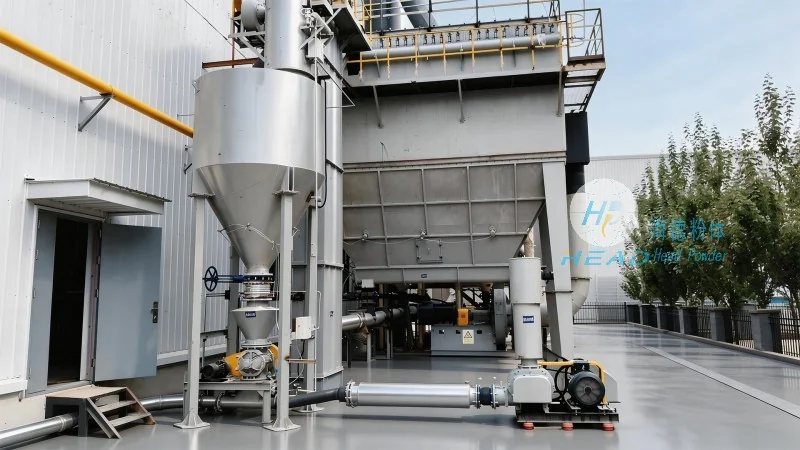
In conclusion, air-powered conveyors for rare earth mineral powders represent a sophisticated and efficient solution for material handling in the rare earth industry. By leveraging the principles of pneumatic transport, these systems offer advantages such as dust-free operation, precise material control, and flexibility in system design. HeadPowder's commitment to quality and customization ensures that clients receive tailored solutions that address their specific processing needs. As the rare earth industry continues to evolve, the importance of reliable and efficient material handling equipment becomes increasingly critical, and air-powered conveyors remain a cornerstone of modern rare earth processing operations.




