Automatic inlet and outlet material pneumatic conveying equipment, also known as pneumatic conveying systems, represent a sophisticated solution for material handling in various industrial settings. These systems are designed to efficiently transport bulk materials from one location to another using air pressure or vacuum, eliminating the need for traditional mechanical conveyors like belts or buckets. The technology behind these systems is rooted in the principles of fluidization and particle movement under controlled air flow, making them versatile for a wide range of applications.
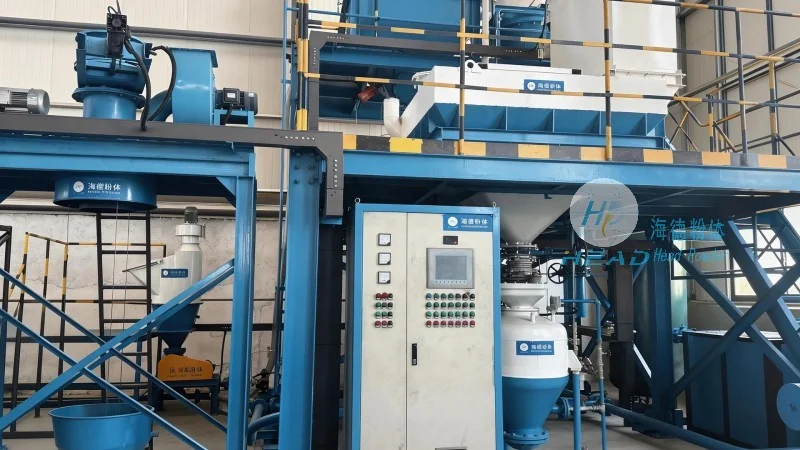
Core Principles of Pneumatic Conveying Systems
The fundamental principle of pneumatic conveying is the use of air as a medium to transport solid particles. In a typical system, material is introduced into a hopper or feeder, where it is then drawn into a pipeline by a vacuum or pressure source. The air flow creates a suspension of particles, allowing them to be carried through the system. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems use a vacuum to pull material from the source. The choice between these systems depends on the distance, height, and material characteristics being handled.
Key Components and Their Functions
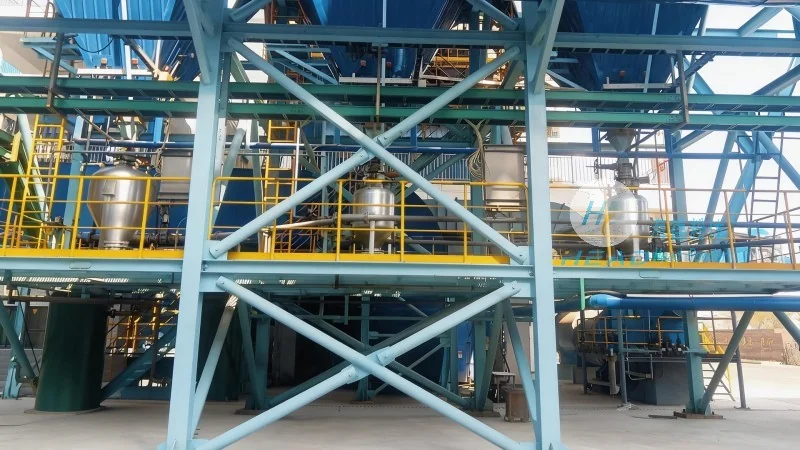
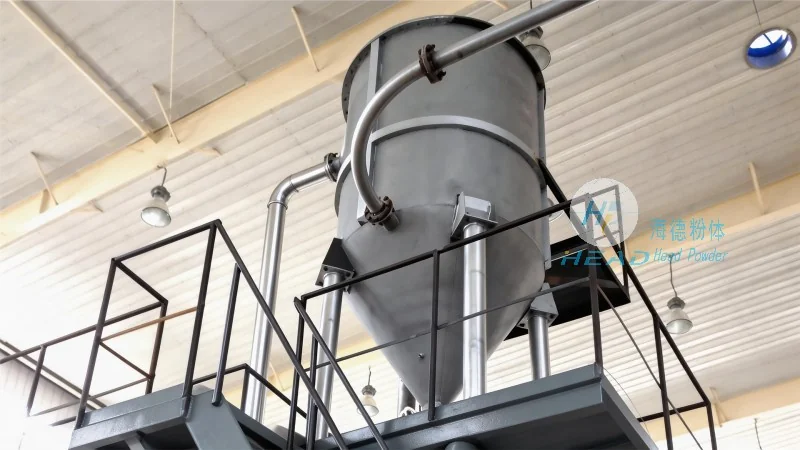
Automatic inlet and outlet material pneumatic conveying equipment consists of several critical components that work in tandem to ensure efficient operation. The primary components include the hopper or feeder, which stores and feeds the material; the air supply system (either a compressor for pressure systems or a vacuum pump for vacuum systems); the conveying pipeline, which transports the material; and the receiver or discharge unit, where the material is deposited. Additionally, control systems such as valves, sensors, and controllers are integrated to regulate the flow and ensure safe operation. These components are engineered to handle different material types, including powders, granules, and even bulk solids, with varying particle sizes and flow properties.
Application Scenarios and Industry Use Cases
The versatility of automatic inlet and outlet material pneumatic conveying equipment makes it suitable for a wide array of industrial applications. In the pharmaceutical industry, these systems are used to transport raw materials and finished products with high precision and minimal contamination, ensuring compliance with stringent quality standards. In the food processing sector, they are employed to handle dry ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry utilizes pneumatic conveying for transporting powders and granules, such as catalysts and reagents, where dust control and material integrity are paramount. Additionally, in the mining and construction industries, these systems are used to transport bulk materials like sand, gravel, and cement, improving operational efficiency and reducing labor costs. The equipment is also widely used in the packaging and manufacturing industries for material transfer between processing units, enhancing overall production throughput.
Advantages of Implementing Pneumatic Conveying Solutions
Automatic inlet and outlet material pneumatic conveying equipment offers several advantages over traditional material handling methods. One of the key benefits is the ability to transport materials over long distances and vertical heights without the need for complex infrastructure. This reduces installation costs and minimizes the risk of material spillage or damage. The systems are also highly flexible, allowing for easy reconfiguration to accommodate changes in production processes or material types. Furthermore, pneumatic conveying is a clean and dust-free method, which is particularly important in industries where dust control is critical, such as food and pharmaceutical manufacturing. The equipment is also energy-efficient compared to mechanical conveyors, as it uses less power to transport materials over the same distance. Additionally, the automated nature of these systems reduces labor requirements and improves safety by minimizing human interaction with potentially hazardous materials.
Customization and Integration with Existing Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to specific customer needs. The company's expertise lies in understanding the unique requirements of each industry and developing solutions that optimize material flow, reduce downtime, and enhance overall operational efficiency. Their systems are designed to integrate seamlessly with existing production lines, ensuring minimal disruption during installation and operation. The company's team of engineers works closely with clients to assess their material handling challenges and propose the most suitable pneumatic conveying solutions, whether for new installations or upgrades to existing systems. By leveraging advanced technology and years of industry experience, Shandong HeadPowder Engineering Co., Ltd. provides reliable and efficient pneumatic conveying equipment that meets the highest standards of performance and safety.
Conclusion and Future Outlook
Automatic inlet and outlet material pneumatic conveying equipment continues to play a vital role in modern industrial operations, offering a efficient and flexible solution for material handling. As industries continue to evolve and demand higher standards of efficiency and safety, the importance of advanced material handling technologies like pneumatic conveying will only increase. The continued innovation in this field, driven by companies like Shandong HeadPowder Engineering Co., Ltd., ensures that these systems will remain a cornerstone of industrial material transport, supporting the growth and success of businesses across various sectors. With their focus on quality, customization, and customer satisfaction, these systems are poised to meet the evolving needs of the industry and contribute to the advancement of industrial processes worldwide.




