Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in cotton seed material handling systems. The company is located in Shandong, China, and has established itself as a key player in providing advanced solutions for agricultural material transportation. With a focus on innovation and quality, HeadPowder offers equipment designed to meet the specific needs of cotton seed processing industries.
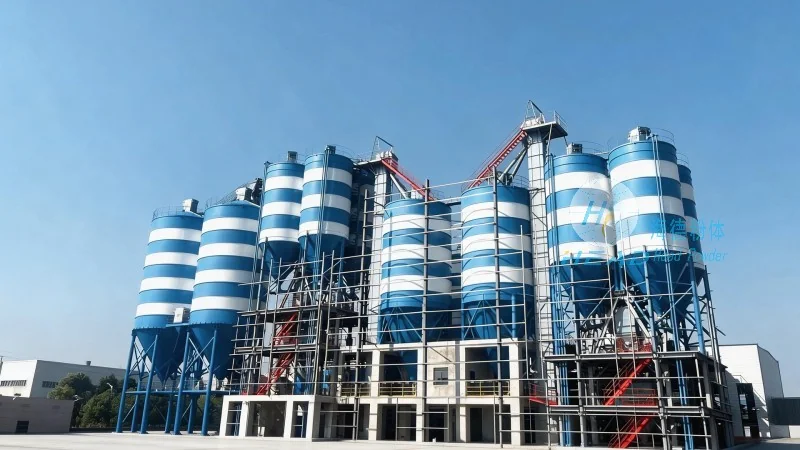
Principle of Cotton Seed Material Handling System Equipment
The cotton seed material handling system equipment operates on the principle of mechanical and hydraulic integration, ensuring efficient movement of cotton seeds through various stages of processing. The system typically includes components such as conveyor belts, rotary feeders, and control panels that work in tandem to manage the flow of material. Mechanical transmission systems, often powered by electric motors, drive the conveyor mechanisms, while sensors monitor the material level and speed to maintain optimal performance. This integrated approach minimizes energy consumption and maximizes throughput, making it suitable for high-volume operations in cotton seed processing plants.
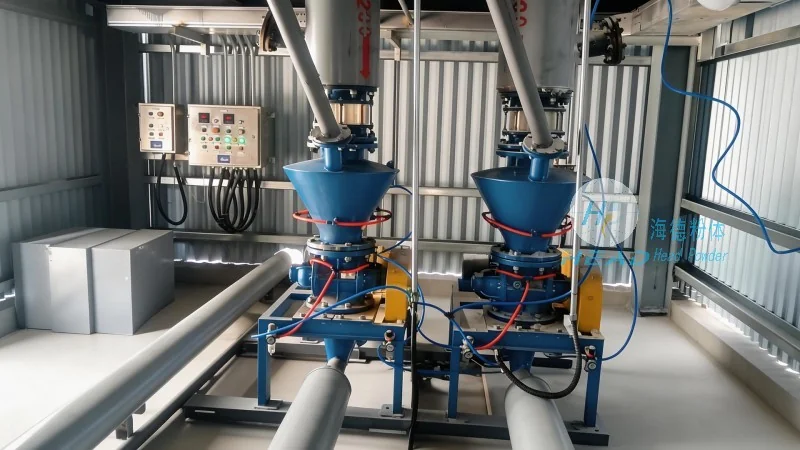
Working Scene Characteristics of the System
In agricultural processing facilities, the cotton seed material handling system is designed to operate in both indoor and outdoor environments, adapting to varying conditions. The equipment's modular design allows for easy installation and integration with existing processing lines, reducing downtime during setup. High-capacity models are available to handle large volumes of cotton seeds, ensuring consistent production rates. The system's durability and low maintenance requirements make it ideal for long-term use, with components constructed from corrosion-resistant materials to withstand the demands of continuous operation. Additionally, the system's user-friendly control interfaces enable operators to adjust settings quickly, enhancing operational flexibility and efficiency.
Application in Cotton Seed Processing
The cotton seed material handling system is crucial in the processing workflow, from seed collection to storage and further processing. It ensures that cotton seeds are transported safely and efficiently from storage bins to processing units, such as cleaning or oil extraction equipment. The system's ability to handle different seed sizes and moisture levels makes it versatile for various processing requirements. By maintaining a consistent flow rate, the equipment reduces the risk of material buildup or blockages, which can lead to production delays. The integration of sensors and control systems also allows for real-time monitoring of the material flow, enabling operators to address issues promptly and maintain optimal performance.
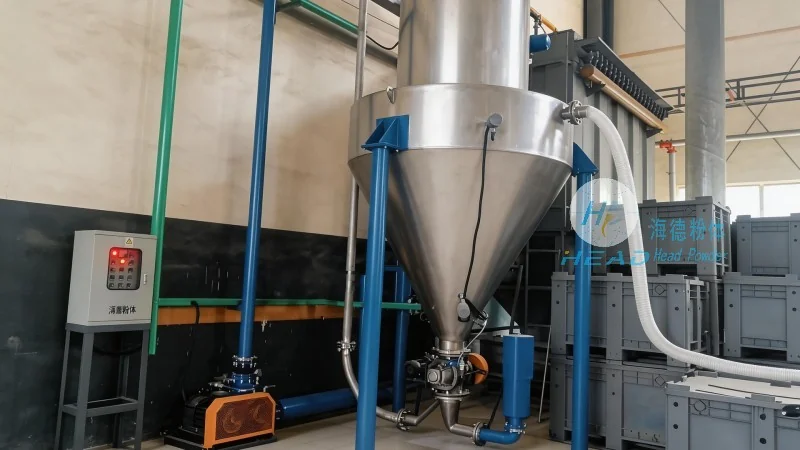
Advantages in Agricultural Processing
Implementing the cotton seed material handling system offers several advantages for agricultural processing facilities. The high efficiency of the equipment reduces labor costs by automating the material transportation process, while the modular design allows for scalability to accommodate growing production needs. The durability of the components ensures long-term reliability, minimizing the need for frequent replacements and repairs. Furthermore, the system's compatibility with existing infrastructure makes it a cost-effective solution for upgrading or expanding processing capabilities. By optimizing material flow, the system contributes to overall production efficiency, helping facilities meet market demands with consistent quality and output.




