Desulfurizer material handling systems are critical components in industrial processes, particularly in power plants and chemical facilities where sulfur dioxide (SO₂) removal is essential for environmental compliance and operational efficiency. These systems are designed to transport and manage desulfurizer materials, such as limestone or other alkaline reagents, to the desulfurization units. Understanding the underlying principles and the specific working scene characteristics of these systems is vital for optimizing performance and ensuring reliable operation.
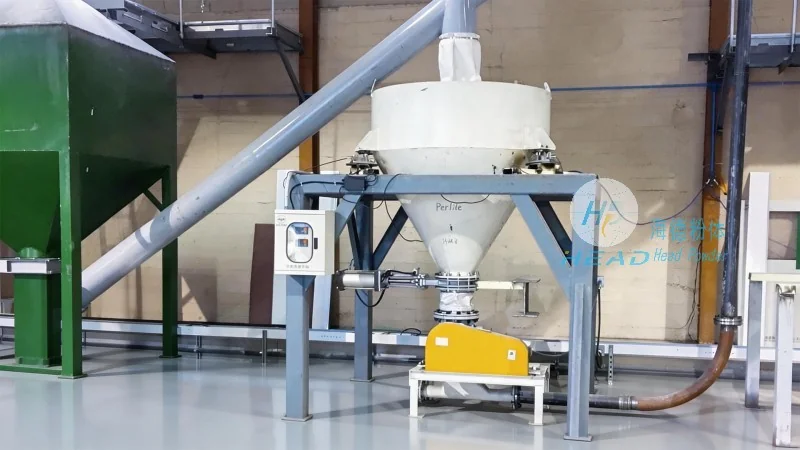
Core Principles of Desulfurizer Material Handling Systems
The fundamental principle of desulfurizer material handling systems revolves around the efficient and controlled transport of bulk materials from storage to the point of use. The systems typically incorporate several key components, including feeders, conveyors, and storage silos, all working in tandem to maintain a consistent flow of material. The design emphasizes minimizing material degradation, preventing dust generation, and ensuring precise dosing to match the plant's desulfurization requirements. Advanced systems may incorporate sensors and control mechanisms to adjust the flow rate in real-time, responding to changes in gas flow or SO₂ concentration. This dynamic control is crucial for maintaining optimal desulfurization efficiency and reducing operational costs.
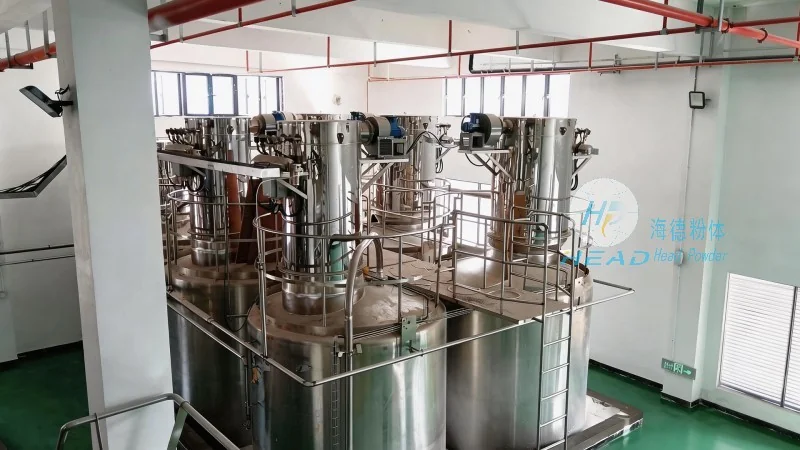
Working Scene Characteristics and Application Environments
Desulfurizer material handling systems operate in diverse industrial settings, each with unique characteristics that influence system design and performance. In power plants, for instance, these systems must handle large volumes of limestone or other reagents, often at high temperatures and under high-pressure conditions. The working environment may involve exposure to corrosive gases and particulate matter, requiring robust materials and protective measures. In chemical processing facilities, the systems may need to handle a wider range of materials, including different types of alkaline reagents or byproducts, necessitating flexible and adaptable equipment. The working scene also includes considerations for space constraints, as plants often have limited room for material handling infrastructure. Additionally, the systems must comply with safety regulations, including dust control and explosion-proof designs, to protect both personnel and equipment. The operational characteristics vary based on the scale of the plant, with larger facilities requiring more extensive and automated material handling solutions.
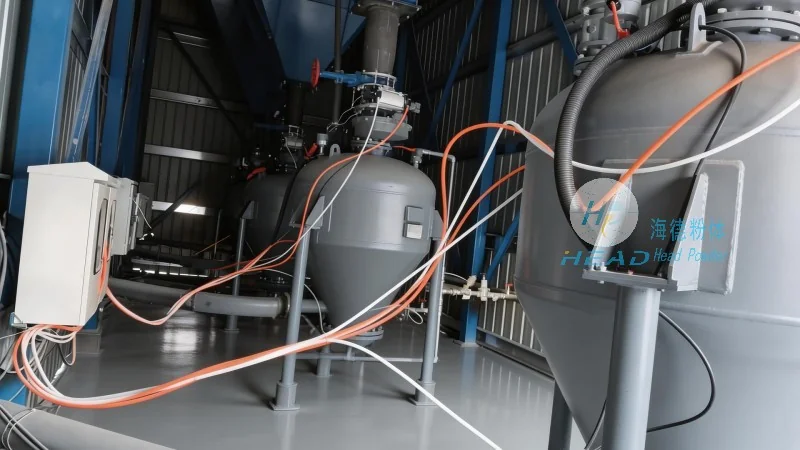
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized engineering solutions for material handling and processing in industrial applications. With a focus on innovation and quality, the company has established itself as a trusted partner for clients seeking reliable desulfurizer material handling systems. HeadPowder's expertise lies in designing and manufacturing equipment tailored to the specific needs of power plants and chemical facilities, ensuring optimal performance and compliance with environmental standards. The company's commitment to customer satisfaction and technical excellence has earned it a strong reputation in the industry, with a track record of successful project implementations across China and beyond. HeadPowder's team of engineers and technicians work closely with clients to understand their operational requirements, providing customized solutions that enhance efficiency and reduce downtime. The company's facilities are equipped with state-of-the-art technology and quality control measures, ensuring that each system meets the highest standards of performance and durability.




