HeadPowder, a leading provider in the field of powder handling technology, specializes in the design and implementation of efficient calcium oxide powder conveying systems. This article explores the fundamental principles behind such systems and highlights the key characteristics of their operational environments.
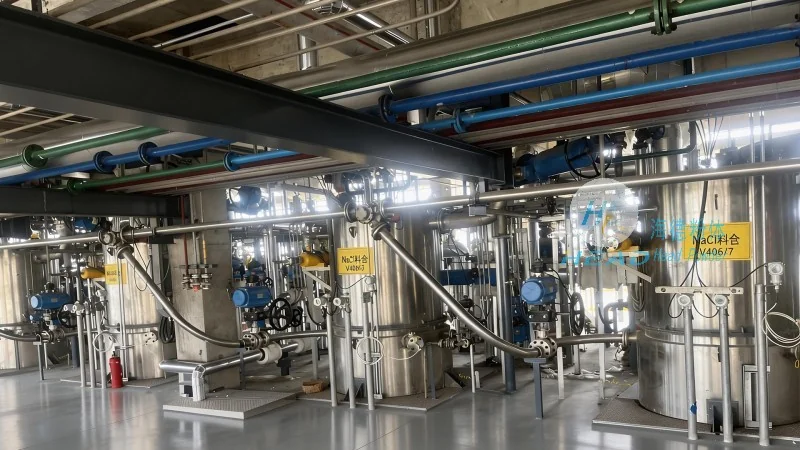
Company Profile and Background
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is dedicated to advancing powder processing solutions. With years of expertise in material handling, the company has developed advanced systems tailored to the unique requirements of calcium oxide and other fine powders. The company's commitment to innovation ensures that their products meet the highest standards of efficiency, reliability, and safety in industrial applications.
The Principle of Calcium Oxide Powder Conveying Systems
Calcium oxide, commonly known as quicklime, is a fine powder with high reactivity and specific handling challenges. The primary principle of calcium oxide powder conveying systems is to transport this material from storage to processing units without compromising its quality or causing operational hazards. These systems typically employ a combination of mechanical and pneumatic technologies to achieve seamless material transfer.
At the core of the system is the selection of appropriate conveying equipment, such as screw conveyors, pneumatic ducts, or vacuum pumps, which are chosen based on the material's properties, flow characteristics, and the distance to be covered. The design also incorporates features like airlocks, rotary valves, and dust collection systems to prevent material degradation and ensure environmental compliance. The system's control mechanisms, including variable speed drives and pressure sensors, allow for precise regulation of the conveying process, optimizing both performance and energy consumption.
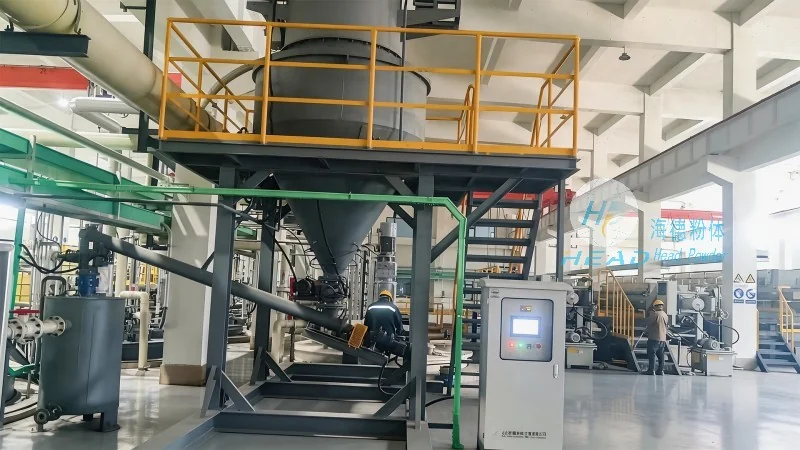
Key Working Scene Characteristics
The operational environment of calcium oxide powder conveying systems varies significantly across different industrial applications. Understanding these characteristics is crucial for selecting the right system and ensuring optimal performance.
Industrial Production Lines
In large-scale manufacturing facilities, calcium oxide is often used as a raw material in processes like steel production, chemical synthesis, and water treatment. The conveying system must integrate seamlessly with existing production lines, maintaining consistent material flow rates and minimizing downtime. The system's robust construction and low maintenance requirements are critical in these high-throughput environments.
Construction and Infrastructure Projects
Calcium oxide is also utilized in construction applications, such as soil stabilization and concrete production. In these scenarios, the conveying system may need to handle larger volumes of material over longer distances, often involving outdoor or semi-outdoor installations. The system's resistance to environmental factors, including temperature fluctuations and moisture, is essential for reliable operation in construction sites.
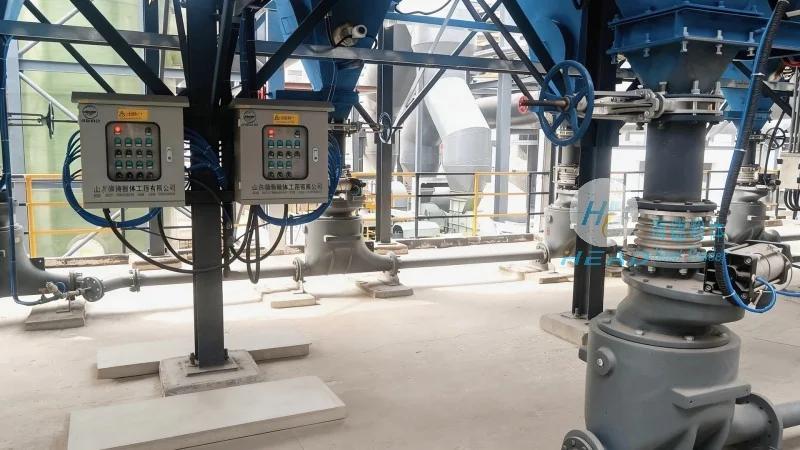
Research and Laboratory Settings
In research and development laboratories, the handling of calcium oxide requires systems that prioritize precision and safety. These systems typically involve smaller-scale conveying equipment with enhanced filtration and containment features. The ability to control the flow of material at a micro level is vital for experimental accuracy and to prevent exposure to the material's dust, which can be harmful if inhaled.
Advantages and Practical Applications
The calcium oxide powder conveying systems offered by HeadPowder Engineering Co., Ltd. are engineered to address the specific challenges associated with handling this reactive powder. By combining advanced materials, intelligent control systems, and ergonomic design, these systems provide several key advantages. They ensure minimal material loss, reduce the risk of dust explosions, and enhance overall operational efficiency. The systems are also designed for easy integration with existing infrastructure, making them suitable for both new installations and retrofits.
Whether used in industrial production, construction, or research, the calcium oxide powder conveying systems from HeadPowder are built to deliver consistent performance and reliability. The company's expertise in powder handling technology ensures that each system is tailored to meet the unique demands of the application, providing a cost-effective and sustainable solution for material transport.




