HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and implementation of efficient alumina powder conveying systems. These systems are engineered to meet the demanding requirements of various industrial applications, ensuring reliable and safe transport of abrasive powders like alumina. The company, headquartered in Shandong, China, leverages advanced technology and expertise to deliver tailored solutions that enhance operational efficiency and product quality.
Principles of Alumina Powder Conveying
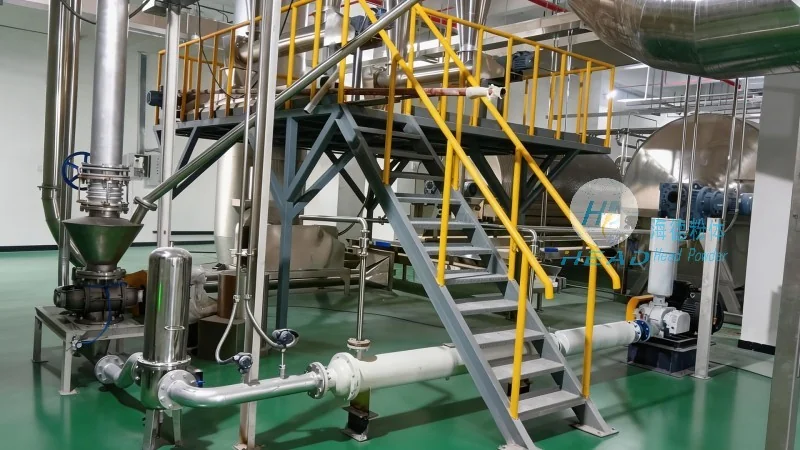
The core principle of an alumina powder conveying system lies in the effective management of material flow from source to destination. Key components typically include feeders, conveyors (such as pneumatic or mechanical systems), and control mechanisms. Pneumatic conveying, for instance, utilizes compressed air to transport dry powders through pipelines, offering advantages like low maintenance and the ability to handle fine particles. Mechanical conveyors, on the other hand, rely on mechanical forces (e.g., belts, screws) to move bulk materials. The choice of system depends on factors such as material properties, process requirements, and environmental considerations. HeadPowder’s systems are designed to optimize these principles, ensuring consistent and controlled powder transport.
Key Components and Their Functions
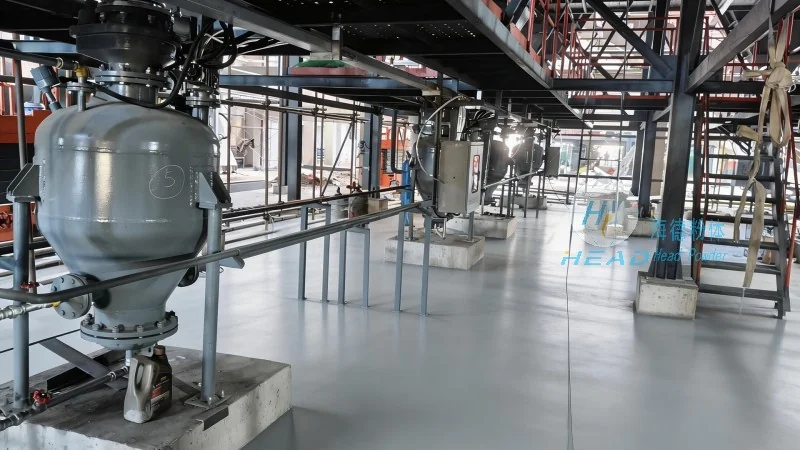
Several critical components contribute to the functionality of an alumina powder conveying system. The material feeder is responsible for accurately metering the powder, preventing overfeeding or underfeeding that could disrupt the conveying process. Conveyors, whether pneumatic or mechanical, are the primary means of transporting the material. For pneumatic systems, the air flow rate and pressure are carefully controlled to maintain a stable flow rate. In mechanical systems, the speed and torque of the conveyor are adjusted to handle the bulk density and flow characteristics of alumina. Control systems, including sensors and automation, monitor parameters like pressure, flow rate, and temperature, ensuring the system operates within safe and efficient parameters. These components work in tandem to provide a reliable and efficient conveying solution.
Application Scenarios and Operational Characteristics
Alumina powder conveying systems are widely used in various industrial sectors, including ceramics, refractories, and metalworking. In the ceramics industry, these systems are essential for transporting raw materials to production lines, where consistent powder quality is crucial for product uniformity. In refractory manufacturing, alumina is used to produce high-temperature resistant materials, and efficient conveying ensures that the material reaches the processing equipment without degradation. The operational characteristics of these systems, such as low dust generation and minimal material degradation, are critical for maintaining product integrity. Additionally, the systems are designed to handle different particle sizes and bulk densities, making them versatile for diverse applications. HeadPowder’s solutions are tailored to meet the specific needs of each application, ensuring optimal performance and reliability.
Advantages of HeadPowder’s Alumina Powder Conveying Systems
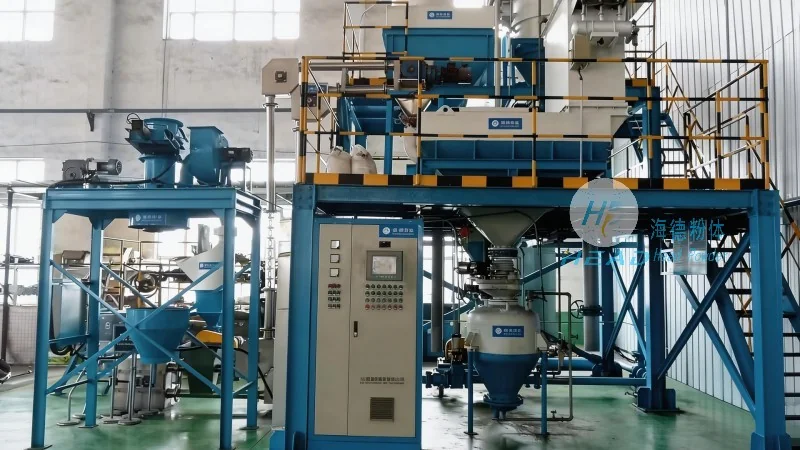
HeadPowder’s alumina powder conveying systems offer several advantages that make them ideal for industrial use. One key benefit is the reduction in dust exposure, which enhances workplace safety and compliance with environmental regulations. The systems are also designed for low maintenance, with components that are easy to replace and service, reducing downtime and operational costs. Additionally, the ability to handle fine and abrasive powders without clogging or degradation ensures consistent product quality. The company’s expertise in material handling and process optimization allows for customized solutions that align with specific production requirements. These advantages make HeadPowder’s systems a preferred choice for industries relying on alumina powder processing.




