Principle and Application Scenarios of Negative Pressure Vacuum Powder Handling Systems
Release time:2026-09-19 02:01:29
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in the development and implementation of advanced powder handling solutions. The company’s expertise lies in designing and manufacturing efficient negative pressure vacuum powder conveying systems, which are critical for industries requiring precise and controlled transport of powders. These systems are engineered to handle a wide spectrum of materials, from fine powders to bulk solids, ensuring minimal product loss and maintaining product integrity throughout the conveying process.
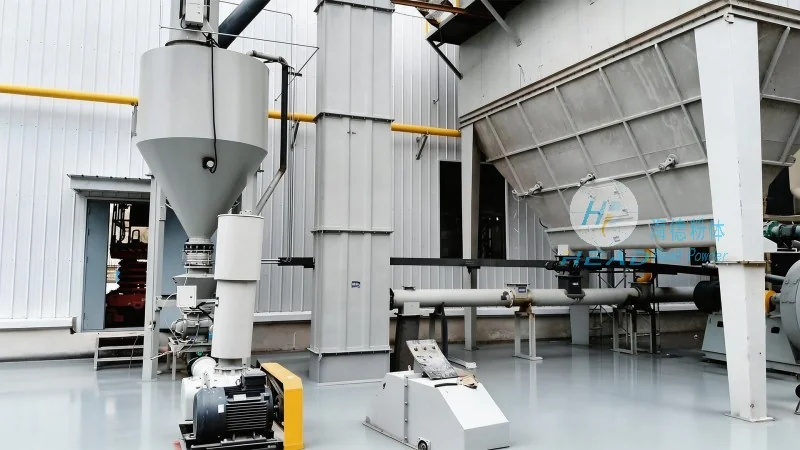
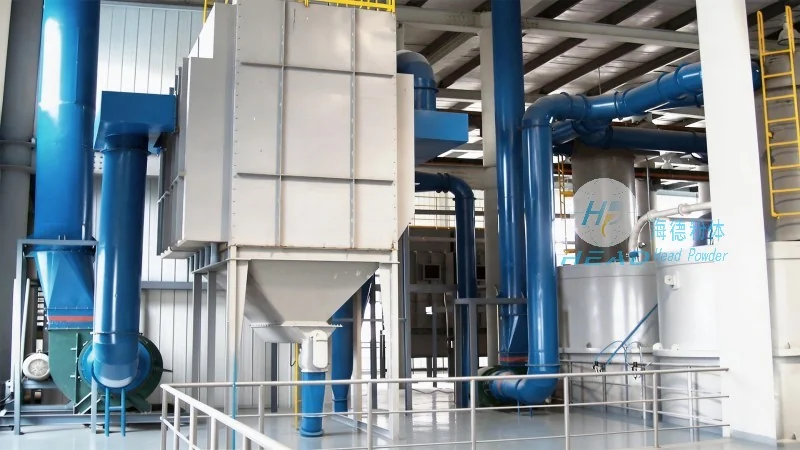
The Principle of Negative Pressure Vacuum Powder Conveying Systems
Negative pressure vacuum powder handling systems operate on the fundamental principle of creating a pressure differential between the source and destination of the powder. A vacuum is generated at the receiving end of the pipeline, typically using a vacuum pump, which maintains a lower pressure inside the system compared to the atmospheric pressure at the material source. This pressure difference forces the powder particles to move along the pipeline, often aided by a hopper or feeder that regulates the flow rate. The system ensures a sealed environment, preventing dust emissions and cross-contamination. Key components include vacuum pumps, filters, and control valves that regulate flow and pressure, enabling optimal performance and safety.
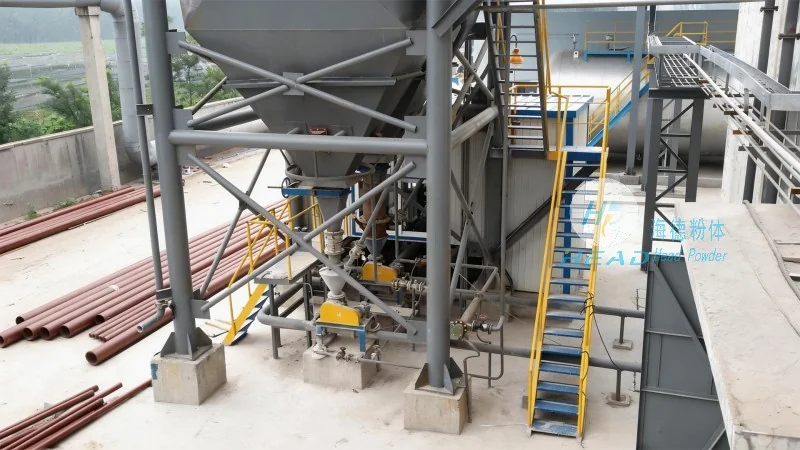
Key Working Scenarios and Applications
The negative pressure vacuum powder conveying systems from HeadPowder are versatile and suitable for diverse industrial applications. In the pharmaceutical industry, they are used to transport active pharmaceutical ingredients (APIs) and excipients, adhering to stringent regulatory standards for hygiene and product purity. In food processing, these systems handle dry ingredients like flour, sugar, and spices, maintaining quality and preventing contamination. The chemical industry benefits from reduced dust exposure and explosion risks when handling bulk chemicals. Additionally, in agriculture, they efficiently transport fertilizers and other agricultural powders, enhancing material handling efficiency and reducing labor costs.
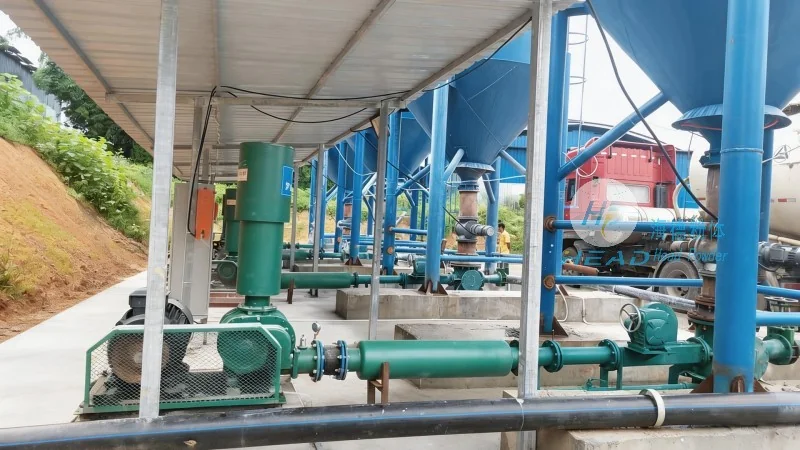
Advantages and Technical Features
HeadPowder’s negative pressure vacuum powder handling systems offer several advantages for modern industrial operations. A primary benefit is the closed system design, which minimizes dust pollution and enhances workplace safety—critical in industries where dust is a health or fire hazard. Energy efficiency is another key feature, as vacuum pumps consume less power than positive pressure systems, leading to long-term cost savings. The modular design allows for easy maintenance, with accessible components that enable quick repairs and minimal downtime. Customization is also possible to meet specific application requirements, ensuring tailored solutions for each client.




