Activated carbon is a critical material in environmental protection, chemical processing, and other industries due to its exceptional adsorption capabilities. The pneumatic conveying system designed for activated carbon powder is a highly efficient method to transport this material. This article will delve into the fundamental principles of the system and its operational characteristics across different scenarios, offering a comprehensive overview of the technology.
Core Principle of the Pneumatic Conveying System
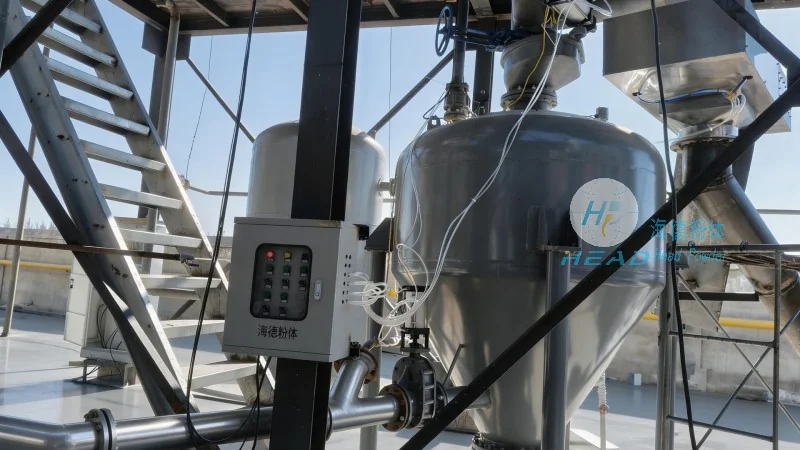
The activated carbon pneumatic conveying system operates on the principle of air flow to move powdered activated carbon. The system comprises several key components: a feeding mechanism, a conveying pipeline network, a pressure vessel, and a dust filtration unit. The activated carbon powder is introduced into the pipeline via the feeding device, while compressed air is introduced to generate a flow that propels the powder forward. The pressure vessel maintains the pressure of the air-powder mixture, and the dust removal unit cleans the air post-conveyance by capturing particulate matter.
Working Scene Characteristics and Application Diversity
The operational characteristics of the activated carbon pneumatic conveying system vary based on the specific industry and application. In environmental protection settings, the system is commonly employed to transport activated carbon to water and air treatment facilities for purification processes. Within the chemical industry, it serves to move activated carbon to production lines for adsorption and separation tasks. Additionally, the system finds applications in food processing, pharmaceutical manufacturing, and other sectors where precise powder handling is essential.
Advantages in Practical Use
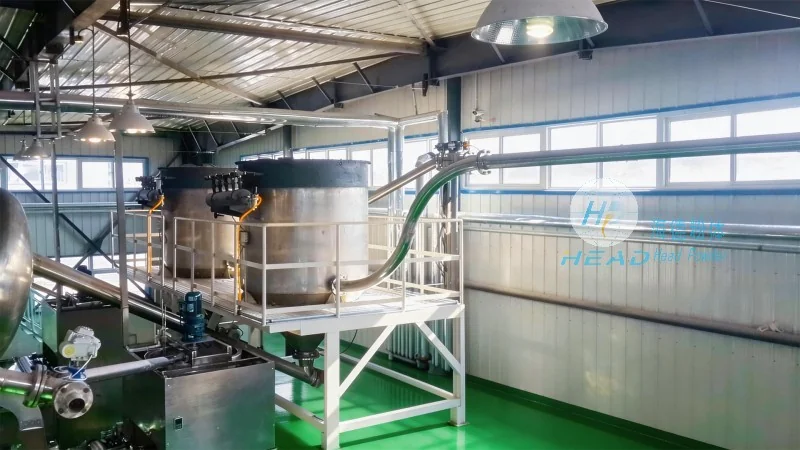
The activated carbon pneumatic conveying system offers multiple advantages, including high efficiency, cost-effectiveness, and minimal noise generation. It enables the transport of activated carbon over extended distances without manual labor, streamlining material handling. The system is also suitable for closed-loop operations, which helps prevent dust contamination and enhances workplace safety and cleanliness.
Customization and Scalability
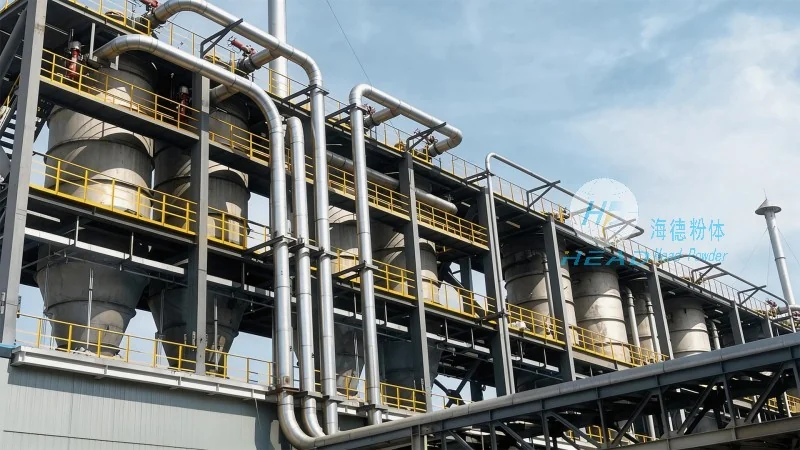
The system can be tailored to meet diverse operational requirements, such as varying conveying capacities, distances, and the specific type of activated carbon powder being handled. This adaptability makes it suitable for both small-scale laboratory applications and large-scale industrial operations. The design flexibility ensures that the system can integrate seamlessly with existing production lines or be deployed as a standalone solution.
Conclusion and Company Overview
The activated carbon pneumatic conveying system represents a reliable and efficient solution for transporting activated carbon powder across various industries. Its widespread adoption in environmental, chemical, and other sectors underscores its effectiveness. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in the design, manufacturing, and implementation of such systems. The company leverages advanced engineering and material science to deliver high-performance solutions that meet the stringent demands of modern industrial applications, ensuring optimal performance and longevity for its clients' operations.




