Bentonite material pneumatic conveying lines are critical equipment in industrial processes, especially for handling bentonite—a natural clay with high water absorption and swelling properties. These systems efficiently transport bentonite from storage to processing units, ensuring smooth operations and maintaining product quality. This article examines the working principle and key features of such systems, offering insights into their design, functionality, and benefits.
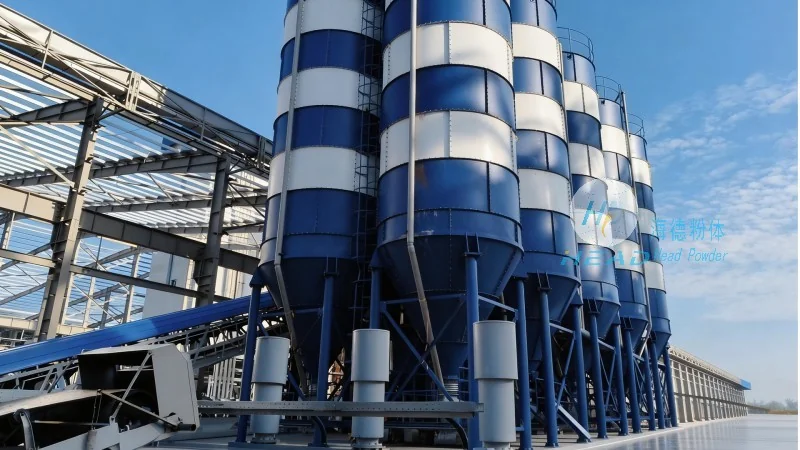
Working Principle of Bentonite Material Pneumatic Conveying Lines
The fundamental mechanism of bentonite material pneumatic conveying lines involves using air or gas to transport solid materials through a pipeline. The system typically operates under positive pressure (pressure pneumatic conveying) or negative pressure (vacuum pneumatic conveying), depending on application requirements. In positive pressure systems, a blower or compressor generates compressed air that pushes bentonite particles through the pipeline. The air flow creates a pressure differential, propelling the material forward while pipeline design—such as bends, elbows, and expansion joints—ensures smooth flow and prevents blockages. Negative pressure systems use a vacuum pump to create a low-pressure environment, drawing bentonite into the pipeline. Both methods rely on fluidization, where air suspends solid particles, allowing transport as a slurry or suspension.
For bentonite, often in powder or granular form, the conveying method depends on particle size, moisture content, and distance. Positive pressure systems are ideal for longer distances or when high pressure is needed to overcome pipeline resistance. They maintain consistent flow rates and prevent material degradation from friction or moisture. Negative pressure systems suit shorter distances or multi-source material collection, drawing material into a central point. The system components—hopper, feeder, pipeline, and receiver—work together: the hopper stores bentonite, the feeder controls flow rate, the pipeline transports material, and the receiver (e.g., storage tank or processing unit) collects it. Valves and regulators regulate air flow to maintain optimal pressure and flow, ensuring efficient and safe operation.
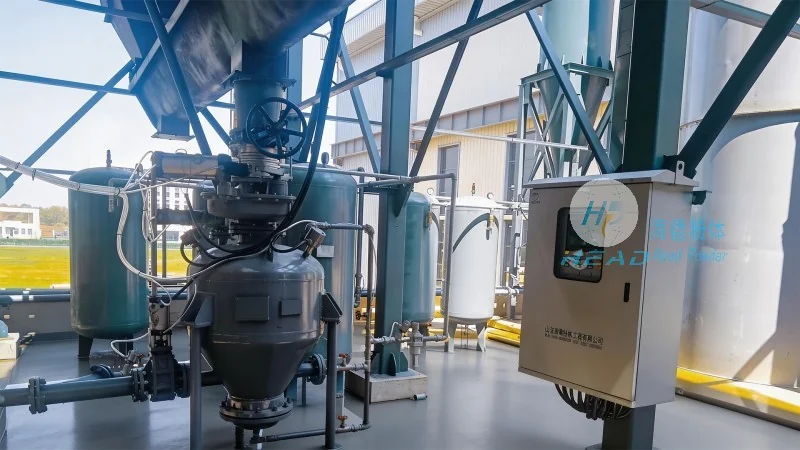
Key Features of Bentonite Material Pneumatic Conveying Lines
Bentonite material pneumatic conveying lines offer several advantages for industrial use. A primary feature is their ability to handle abrasive or sensitive materials like bentonite without damage. Air flow suspends particles, reducing friction and wear on pipelines and equipment—critical for preventing bentonite degradation. The systems also provide a dust-free, hygienic environment, enclosing material to prevent contamination and comply with health and safety regulations. This is vital in industries like food, pharmaceuticals, or cosmetics, where product purity is essential.
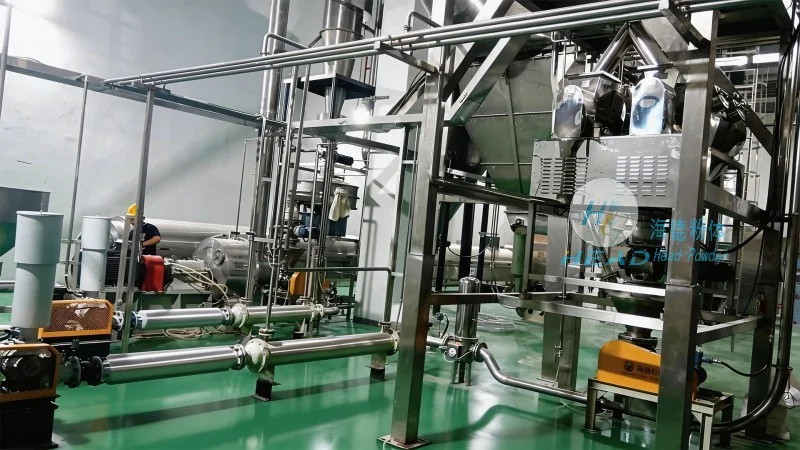
Another key feature is flexibility and scalability. Systems can handle varying material volumes and flow rates, suitable for small or large-scale operations. Modular design allows easy integration with existing production lines, with components customizable for specific processes. For example, pipeline length or diameter can be adjusted for distance or quantity. The system also offers energy efficiency, optimizing air flow to minimize consumption while maintaining performance—beneficial for long-term cost management.
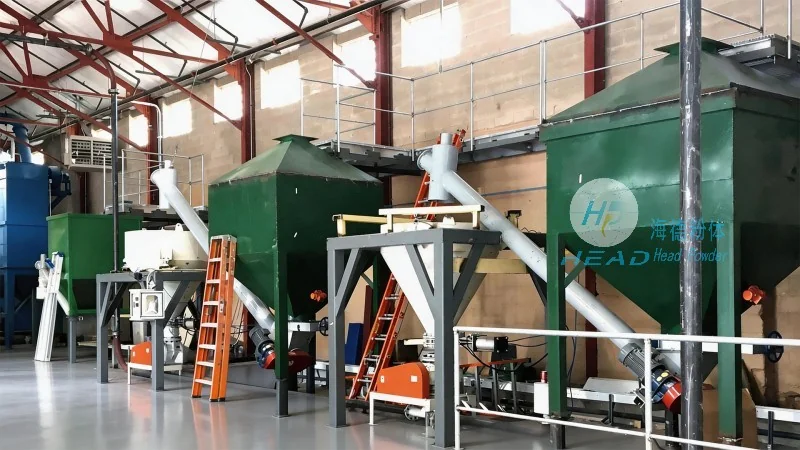
Additionally, these systems provide environmental benefits by reducing manual handling and open storage, which can cause dust emissions. Enclosed design minimizes dust dispersion, aiding compliance with air quality standards. This is crucial in regions with strict regulations. The systems also preserve product quality by preventing moisture or contaminant exposure, impacting bentonite performance in downstream processes—such as oil and gas drilling, where bentonite is a drilling fluid additive.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including bentonite material pneumatic conveying lines. HeadPowder is headquartered in Shandong, China, specializing in designing, manufacturing, and installing customized solutions for various industries. With extensive experience, HeadPowder has built a reputation for quality, reliability, and customer satisfaction. The company’s products meet international standards and are tailored to client needs, ensuring optimal performance and longevity. HeadPowder’s commitment to innovation and customer service makes it a trusted partner for businesses seeking efficient material handling solutions. Its facilities in Shandong are equipped with advanced technology and skilled personnel, enabling delivery of high-quality products and services to clients worldwide.




