HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust-free bag-in bulk material pneumatic conveying systems. These systems are designed to efficiently transfer bulk materials from sealed bags into processing equipment while maintaining a clean and controlled environment. This article explores the working principle and key features of such systems, highlighting their benefits and practical applications.
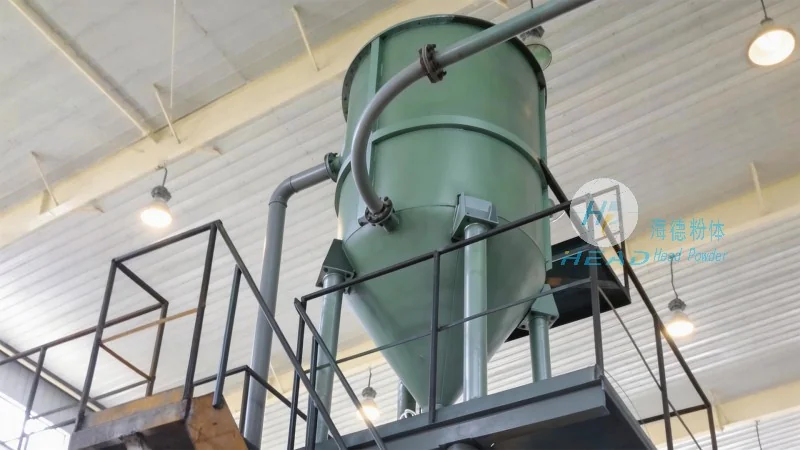
Working Principle of the Dust-Free Bag-In Bulk Material Pneumatic Conveying System
The core of the dust-free bag-in bulk material pneumatic conveying system lies in its integrated approach to material handling. The process typically begins with a sealed bag containing the bulk material. The system uses a combination of air pressure and vacuum to draw the material from the bag and transport it to the processing unit. The sealed bag design ensures that no dust or contaminants are released into the environment during the transfer, making it ideal for industries where air quality and product purity are critical.
First, the sealed bag is positioned over the intake port of the conveying system. The system then creates a vacuum inside the bag, which pulls the material out through a specialized nozzle or spout. Simultaneously, compressed air is introduced to assist in the material flow, ensuring a smooth and continuous transfer. The material is then carried through a flexible hose or rigid pipe to the destination, such as a mixer, reactor, or storage tank. The entire process is automated, with sensors and controls monitoring the flow rate and pressure to maintain optimal performance.
Key Features of the Dust-Free Bag-In Bulk Material Pneumatic Conveying System
Several distinctive features make the dust-free bag-in bulk material pneumatic conveying system a preferred choice for various industries. One of the primary advantages is its ability to maintain a completely dust-free environment. By keeping the material contained within the sealed bag until it reaches the processing equipment, the system eliminates the risk of airborne particles contaminating the workspace or the final product. This is particularly important in pharmaceutical, food, and chemical industries where product purity and regulatory compliance are paramount.
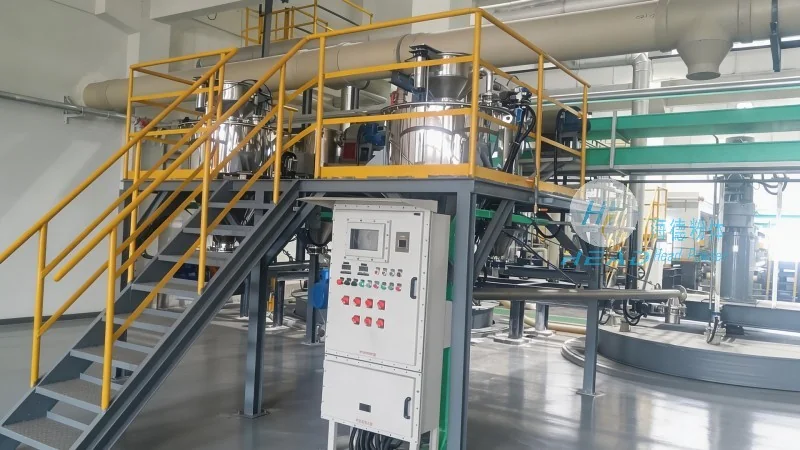
Another significant feature is the system's efficiency and speed. Compared to traditional manual or mechanical transfer methods, the pneumatic conveying system can handle large volumes of material quickly and with minimal labor. The automated operation reduces human error and increases productivity, making it suitable for high-throughput production lines. Additionally, the system is highly versatile, capable of handling a wide range of materials, including powders, granules, and even bulk solids, with minimal adjustments.
The design of the system also emphasizes safety and reliability. The sealed bag mechanism prevents accidental spills or leaks, reducing the risk of material loss or environmental contamination. The use of high-quality materials and robust construction ensures long-term durability and consistent performance. Furthermore, the system is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms to protect both the equipment and the operators.
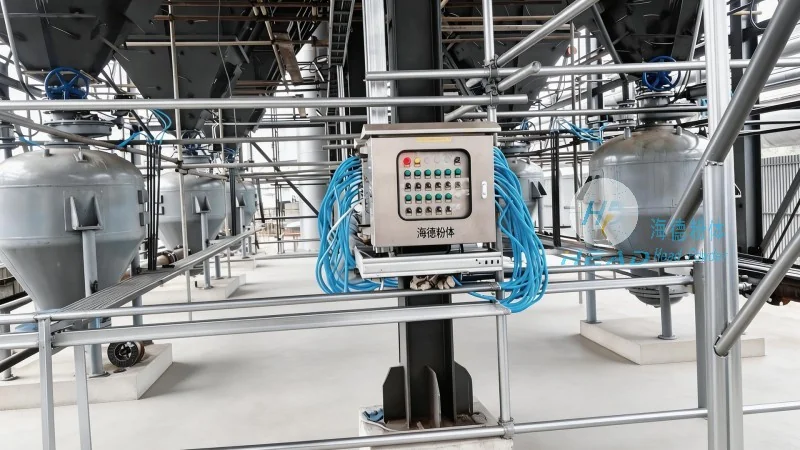
Applications and Benefits in Industrial Settings
The dust-free bag-in bulk material pneumatic conveying system finds extensive applications across multiple industries. In the pharmaceutical sector, it is used to transfer active pharmaceutical ingredients (APIs) and excipients into production lines, ensuring that the final drug products meet stringent purity standards. In the food industry, the system is employed to handle ingredients like flour, sugar, and spices, maintaining the quality and safety of the food products. The chemical industry also benefits from this technology, as it allows for the safe transfer of hazardous materials without exposing workers to dangerous fumes or dust.
One of the key benefits of this system is its contribution to improved workplace safety. By eliminating the need for manual handling of bulk materials, the system reduces the risk of workplace injuries, such as back strains or exposure to harmful substances. This not only enhances the safety of the workforce but also helps companies comply with occupational health and safety regulations. Additionally, the system's ability to maintain a clean environment reduces the need for extensive cleaning and maintenance, saving time and resources.
In conclusion, the dust-free bag-in bulk material pneumatic conveying system by HeadPowder Engineering Co., Ltd. offers a reliable and efficient solution for bulk material handling. Its working principle, centered on sealed bag technology and pneumatic transfer, ensures minimal contamination and maximum productivity. The key features, including dust-free operation, efficiency, versatility, and safety, make it an ideal choice for industries where product quality and environmental compliance are critical. As a manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality solutions to meet the evolving needs of its clients.




