Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound with various industrial applications. In many manufacturing processes, efficient and reliable material handling is crucial, and pneumatic conveying systems have emerged as a preferred method for transporting this material. This article explores the working principle and key characteristics of pneumatic conveying systems specifically designed for heptahydrate magnesium sulfate, highlighting how such systems enhance operational efficiency and safety in material handling operations.
The Working Principle of Heptahydrate Magnesium Sulfate Pneumatic Conveying
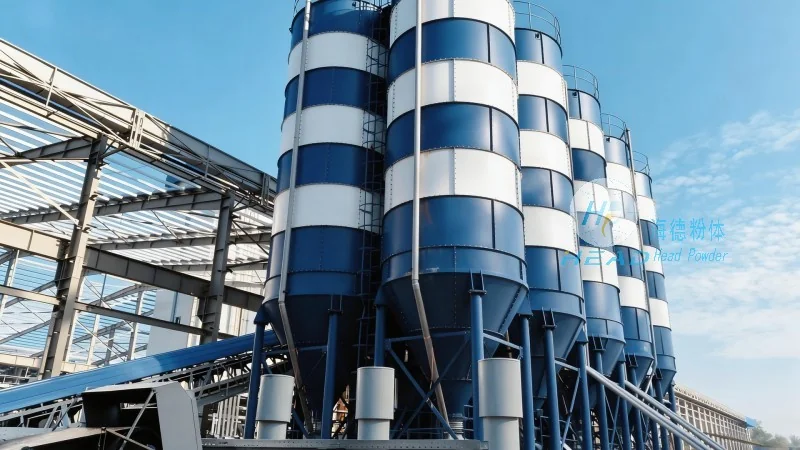
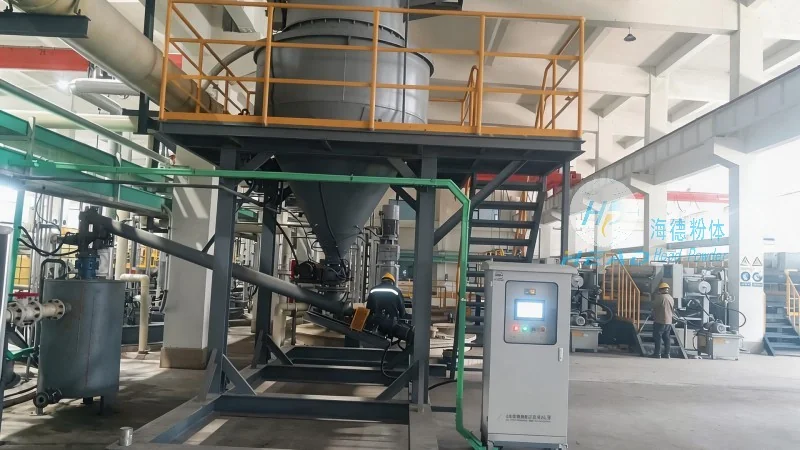
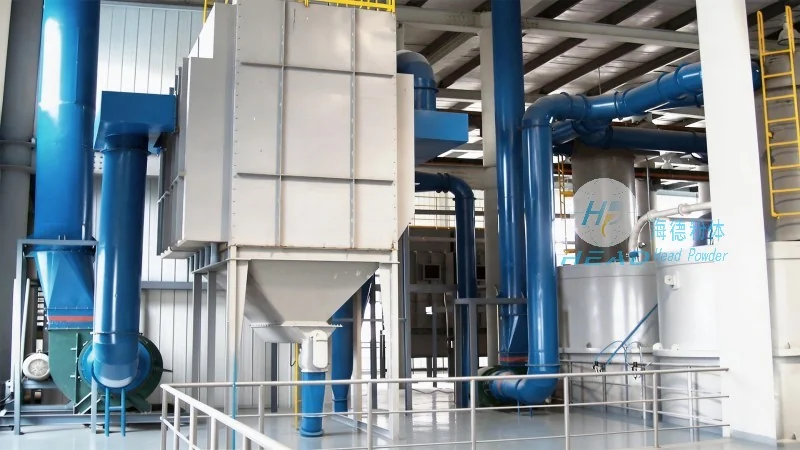
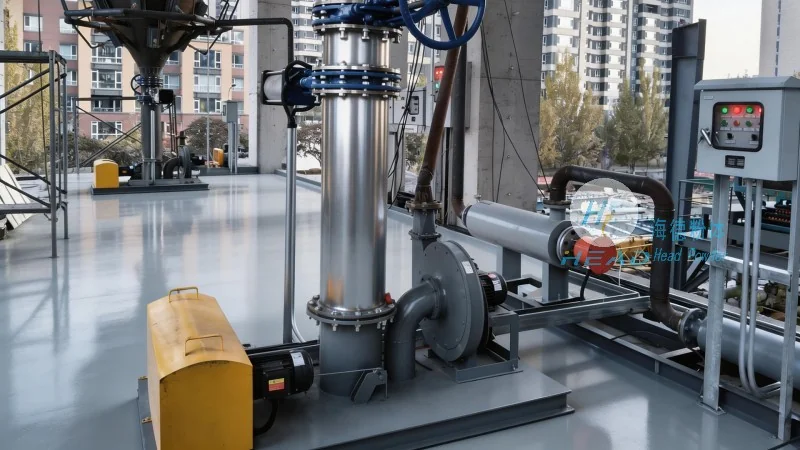
Pneumatic conveying, or air conveying, utilizes compressed air to transport bulk materials like heptahydrate magnesium sulfate through a network of pipes. The process typically involves several key components and steps. First, the material is fed into the system via a hopper or a rotary valve, which controls the flow rate. Then, a blower or compressor generates high-pressure air that is introduced into the conveying line. As the air flows through the pipe, it creates a flow that lifts and transports the solid particles of heptahydrate magnesium sulfate. The air velocity is carefully controlled to ensure that the particles are carried without excessive wear or degradation. The conveying line may include bends, expansions, or other components to direct the material to the destination, such as a storage silo or a processing unit. At the end of the line, a separator or cyclone separates the material from the air, allowing the heptahydrate magnesium sulfate to be collected and the air to be filtered and recycled. This closed-loop system minimizes dust emissions and ensures a clean, efficient operation.
Key Characteristics of Heptahydrate Magnesium Sulfate Pneumatic Conveying Systems
Systems for conveying heptahydrate magnesium sulfate via pneumatic methods exhibit several notable characteristics that make them advantageous in industrial settings. One primary characteristic is their high efficiency in material transport. By using air as the conveying medium, these systems can move large quantities of heptahydrate magnesium sulfate over considerable distances with minimal energy consumption compared to traditional mechanical methods like belt conveyors. This efficiency is particularly valuable in large-scale production facilities where continuous material flow is essential. Additionally, pneumatic conveying systems offer enhanced safety features. Since the material is transported within a sealed pipe system, there is a reduced risk of dust exposure, which is critical for maintaining a safe working environment and complying with occupational health regulations. The enclosed design also prevents material contamination from external sources, ensuring the purity of heptahydrate magnesium sulfate, which is vital for its use in pharmaceutical, food, and other sensitive applications. Another characteristic is the flexibility of the system. Pneumatic conveying can be easily adapted to different production layouts, allowing for changes in material flow routes or integration with other processing equipment without significant modifications. This adaptability makes it suitable for diverse industrial applications, from small-scale laboratories to large-scale manufacturing plants. Furthermore, the systems are relatively low in maintenance compared to mechanical conveyors, as they have fewer moving parts and are less prone to wear and tear from abrasive materials like heptahydrate magnesium sulfate. The use of air as the conveying medium also reduces the risk of material buildup or clogging in the pipes, which can be a common issue with mechanical systems. Overall, the combination of efficiency, safety, and flexibility makes pneumatic conveying an ideal choice for handling heptahydrate magnesium sulfate in various industrial processes.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on innovative and efficient systems, the company specializes in the design, manufacturing, and installation of pneumatic conveying equipment tailored to the needs of various industries. HeadPowder's expertise lies in developing customized solutions that optimize material flow, enhance operational safety, and improve overall productivity. The company's facilities are located in Shandong, China, where it leverages advanced technology and a skilled workforce to deliver high-quality products and services. By adhering to stringent quality standards and customer-centric approaches, HeadPowder has established itself as a trusted partner for businesses seeking reliable material handling solutions for heptahydrate magnesium sulfate and other bulk materials. The company's commitment to excellence and continuous improvement ensures that its clients receive systems that meet their specific requirements and contribute to their long-term success in the market.




